Globule Manufacturing's fully wash down sanitary equipment are custom engineered solutions for your specific product needs. Globule conveyors, bucket elevators and vibrator are created to simplify the product handling process. We specialize in raw product handling, food and pharmaceutical processing industry, including dairy; meat, poultry, bakery, fresh and frozen produce and pet food.
Globule equipment is designed with sanitation in mind, Our engineering design team had over 10 years hand-on experiences from the industries. Our cutting design are simply and durable. Our highest quality workmanship is designed and follow FSMA guidelines.
Globule product is designed for food and pharmaceutical industries to meet the hygiene standards required within these industries. We use superior high grade materials designed for ease of use and hygiene.
We recognize that each customer has unique requirements. To meet these needs, we provide customized solutions to ensure that each piece of equipment can be precisely matched to your production process and product specifications. By working closely with our customers, we are able to design and manufacture equipment that meets specific capacity, size, and hygiene requirements, thereby optimizing production efficiency and product quality.
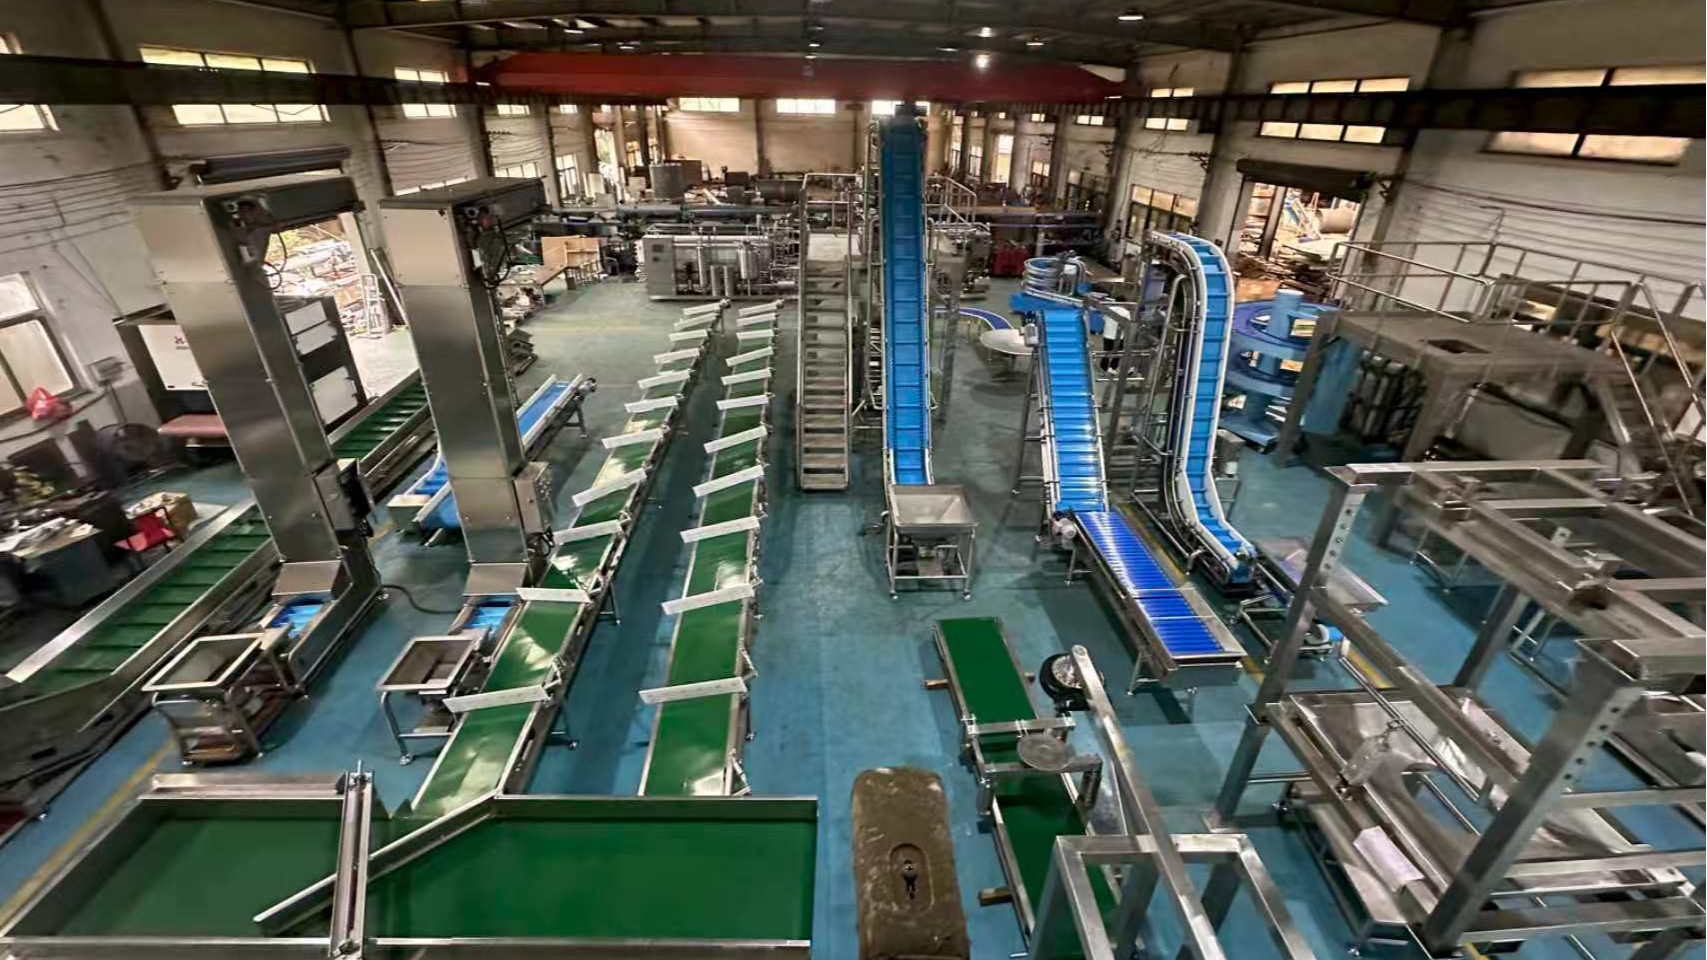
We implement strict quality inspections at every stage, from raw material procurement to finished product delivery, and adhere to international standards to ensure our equipment is durable, reliable, and has a low failure rate.
Behind this is the GLOBULE team — a group of professionals driven by passion and expertise. With a joyful spirit, they develop cutting-edge machinery, deliver superior service, and are all committed to fulfilling the company's mission and ensuring customer satisfaction.
 EN