EN

- Overview
- Recommended Products
Overview
1. Product Overview
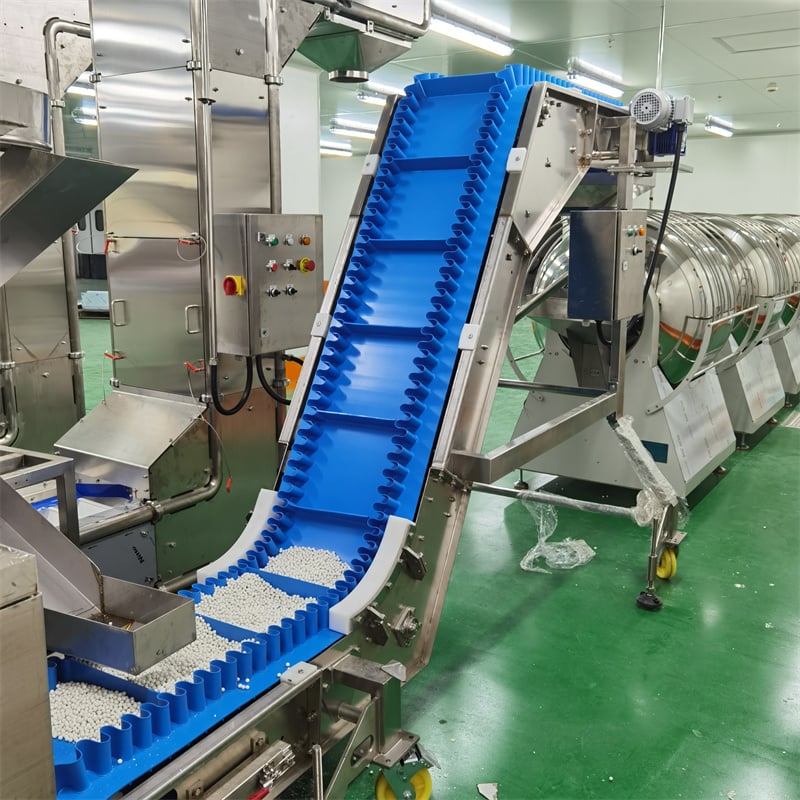
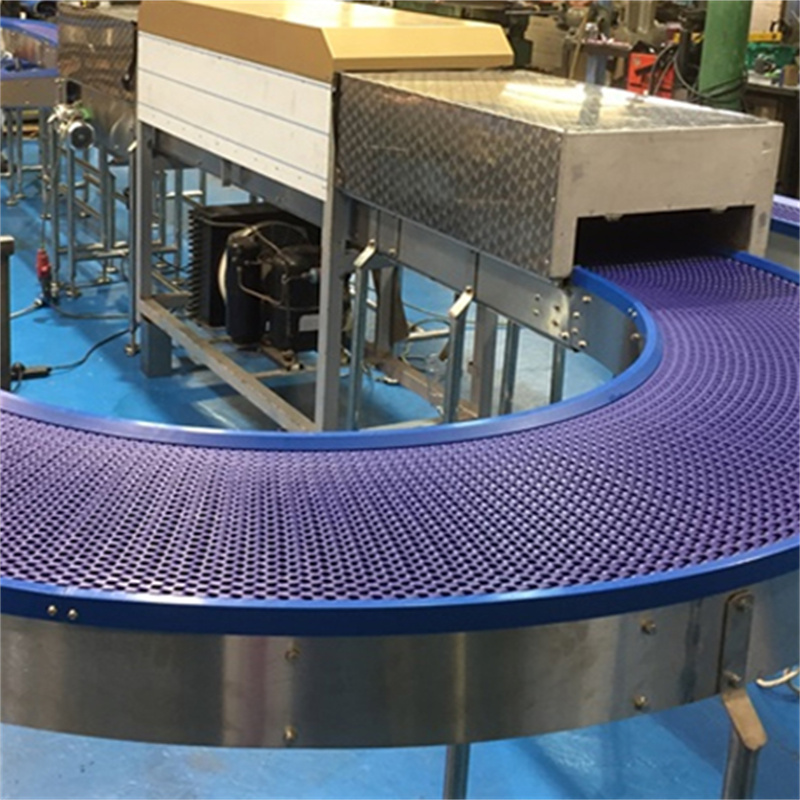
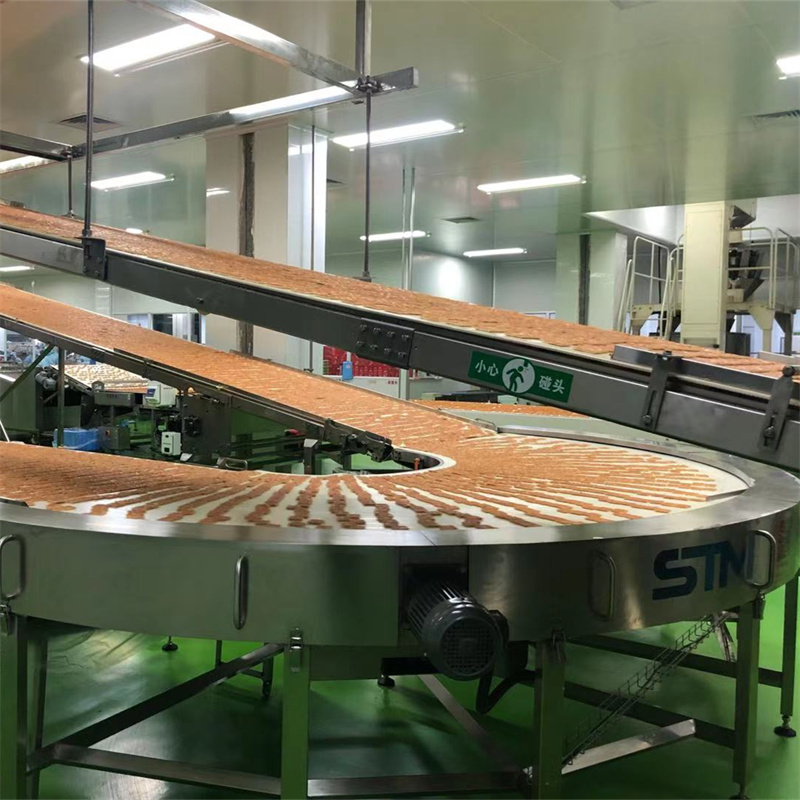
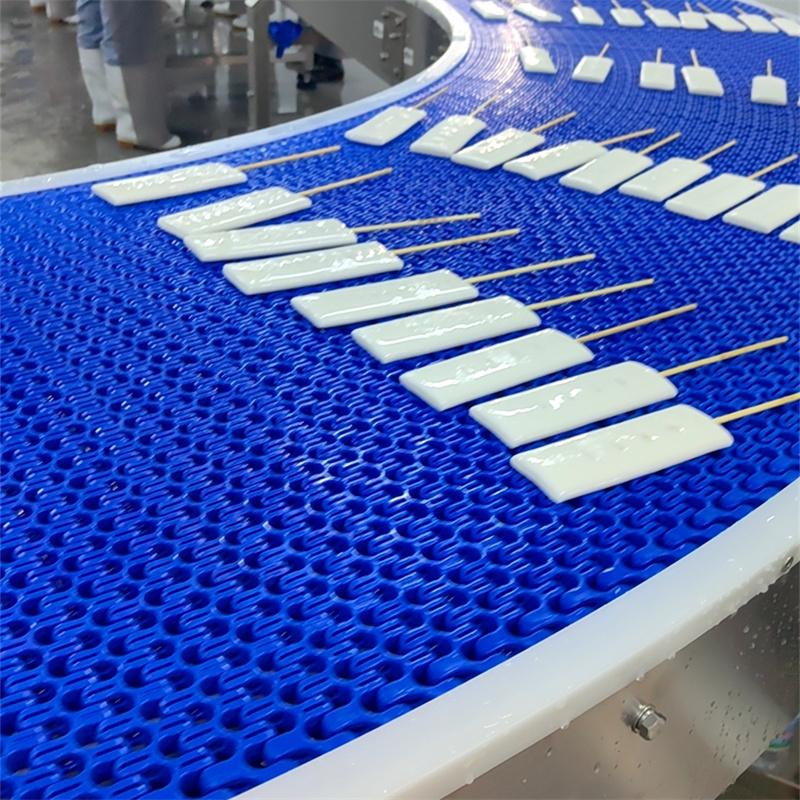
The Conveyor is a hygienic belt conveying system developed by Globule Sanitary Conveyor Pty Ltd for the post-packaging logistics of food factories. In the 2-in-1 Merging Line it performs the merging and buffering duty for finished bags: it gathers the finished bags discharged from the VFFS packaging machine and take-off conveyor — bags that originate from two weighing channels — into one orderly main stream, and provides buffer accumulation when the downstream case-packing station is temporarily busy, so that the high-speed packaging section never has to stop.
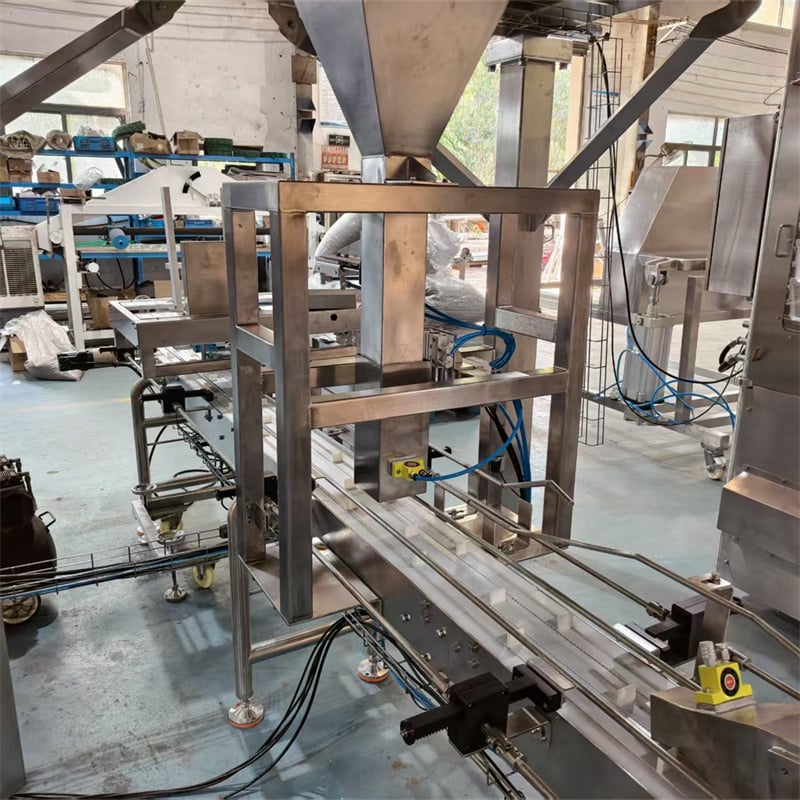
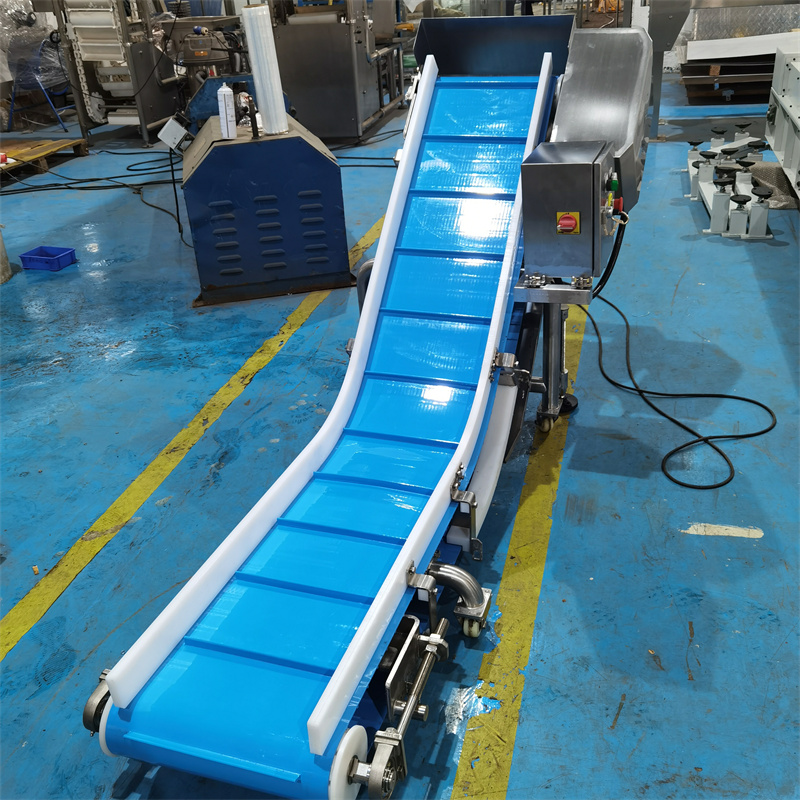
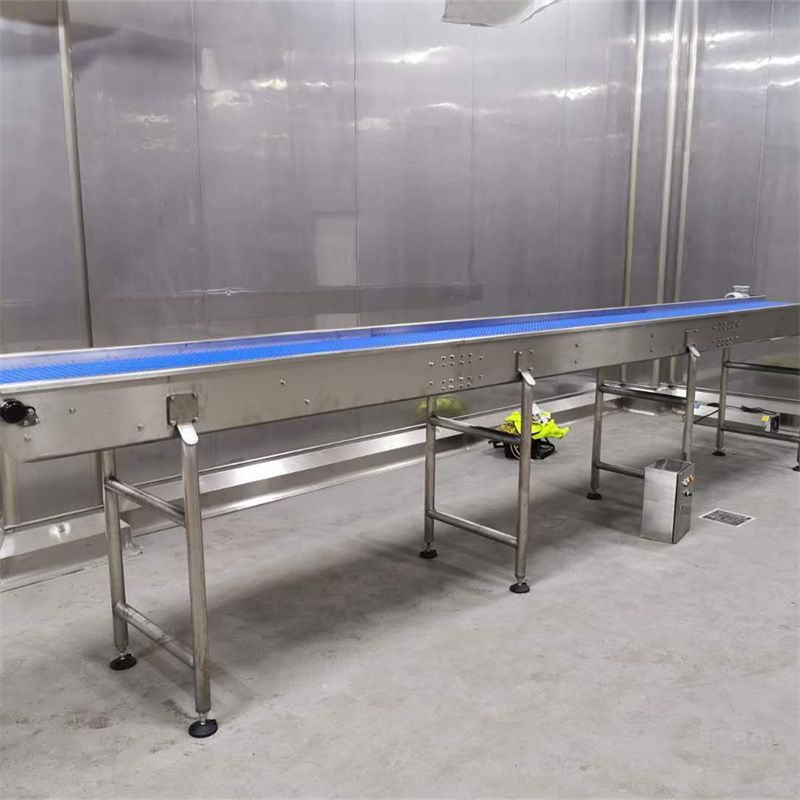
The whole conveyor carries Globule's unified hygienic design language: round-tube frame, concealed wiring, washdown-capable construction and quick-release conveying parts. The frame is made of food-grade stainless steel, and the belt can be selected from food-grade PU, TPU and other safe materials that are non-toxic to food contact and easy to clean. Frame height, width and length can all be customized according to the line layout and bag dimensions, and the conveyor can be built to the same height datum and interface as other units of the 2-in-1 Merging Line for seamless docking.
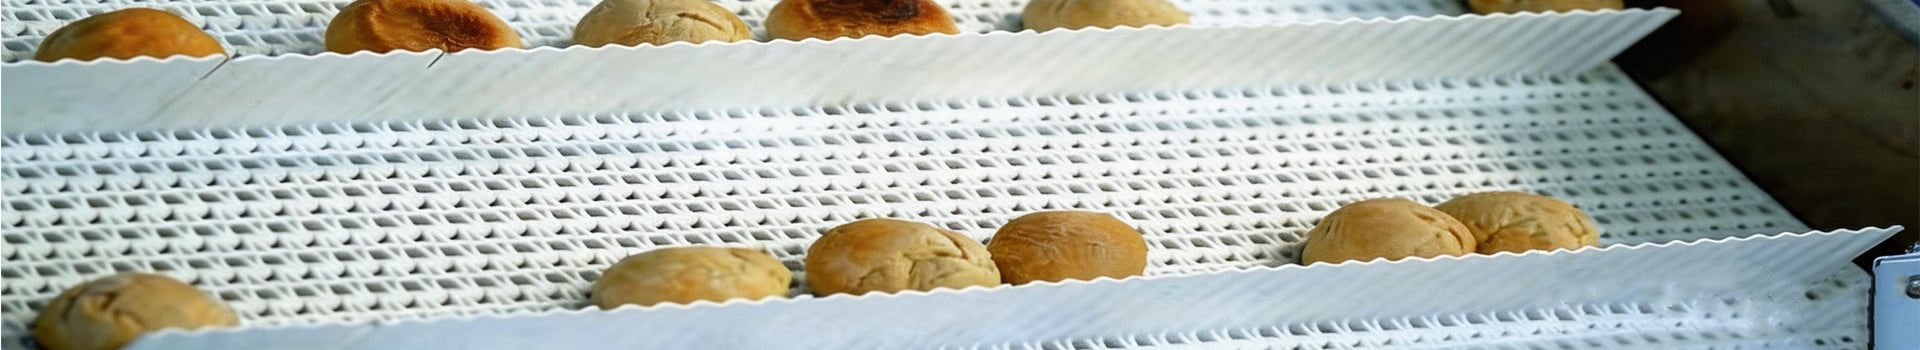
For puffed products such as potato chips, corn chips and egg yolk cakes, finished bags are light, fragile and easily crushed, so conveying must be smooth, impact-free and jam-free. Through variable-frequency speed control, guiding side rails and smooth transfer sections, the Globule conveyor keeps bags aligned and stable, reducing the time spent on manual tidying and lowering the risk of bag breakage and product shattering. It can be purchased alone for retrofitting the rear section of an existing line, and it is also an indispensable "blood vessel" of the Globule 2-in-1 Merging Line.
2. Core Advantages
Advantage 1: Conveying engineered specifically for finished bags
The conveyor is optimized for the "light, brittle, slippery" nature of puffed-snack bags: a smooth belt surface with moderate friction and adjustable guiding rails keep bags on track without skewing, stacking or scratching. Transfer sections are seamlessly joined to eliminate steps and drops that cause impact, minimizing bag breakage and content shattering and protecting the integrity of every bag of chips or egg yolk cakes.
Advantage 2: Merging and buffering in one — escorting high-speed packaging
The heart of the 2-in-1 Merging Line is a high-speed VFFS machine; after the two channels merge, a large number of finished bags are produced every minute. If downstream case packing or palletizing lags behind for a moment and no buffer exists, the entire front section has to stop and wait. The Globule conveyor solves this with a well-designed merging angle and buffer zone where bags queue naturally and accumulate in order, buying valuable time for downstream operators and maximizing overall line efficiency. No more "high-speed packaging, low-speed finishing".
Advantage 3: Round-tube frame plus whole-machine washdown — hygiene without dead corners
The frame uses Globule's signature round-tube construction: smooth, edge-free surfaces that never trap dirt. The belt and rollers can be dismantled quickly for daily cleaning and sanitation, and the whole machine tolerates direct washdown with a high-pressure water gun, complying with FSMA sanitary design guidelines. A food-factory audit no longer needs to worry about "dirt hiding" in the conveying equipment.
Advantage 4: Concealed wiring — safe and good-looking
Motor cables and sensor cables all run through dedicated concealed channels — no exposed cables dragging on the floor, no risk of forklifts or personnel snagging them, and no dust or foreign matter hiding on cable surfaces. The clean, uniform appearance matches the overall style of the 2-in-1 Merging Line and makes the workshop look professional and tidy.
Advantage 5: Highly modular — flexible match with the line
Frame height, length, belt width and speed can all be customized; horizontal, inclined and climbing configurations are available. The conveyor docks seamlessly with the Metal Inspection and Weighing Machine, take-off conveyor and packing tables. The modular design also makes future line reconfiguration, relocation and expansion simpler, protecting the customer's long-term investment.
3. Technical Specifications
| Item | Specification / Description |
| Equipment | Hygienic food-grade belt conveyor (finished-bag merging/buffering type) |
| 2-in-1 role | Finished-bag merging and buffer conveying |
| Frame material | Food-grade stainless steel, round-tube design |
| Belt material | Food-grade PU / TPU, etc. (selected by product) |
| Speed control | Variable-frequency drive |
| Hygiene design | Whole-machine washdown, no dead corners, quick disassembly |
| Wiring | Concealed wiring |
| Suitable products | Bagged puffed products: potato chips, corn chips, egg yolk cakes, etc. |
| Customization | Frame height/width/length, belt speed, side rails, merging angle per line layout |
| Note | Detailed dimensions and load data are engineered per actual layout and bag spec; refer to the official proposal |
4. Role in the 2-in-1 Merging Line
"2-in-1" means that two feeding and weighing channels merge into one packaging machine, so downstream of the packer the finished bags naturally arrive at "double density": the output of the two weighing channels converges in one place and bags pour out in a short time. Without a reliable merging and buffering conveying system, the rear section would jam and stop constantly, and the speed advantage created by merging two lines would be completely lost.
The core role of the Globule conveyor in the system is "buffering and order". First, it receives finished bags from the take-off conveyor and merges the two-line output into a single orderly product stream through the merging section. Second, its buffer section absorbs the pace difference between front and rear sections: when the case-packing station is busy, bags queue and accumulate on the line so the VFFS machine and the Metal Inspection and Weighing Machine keep running. Third, as the connecting link, it carries the bags smoothly onward to packing and palletizing stations.
In short, the conveyor is the key that lets the 2-in-1 Merging Line move from "high-speed packaging" to "smooth finishing". Without it, front-end speed is cancelled out by rear-end congestion; with it, the whole line runs continuously, evenly and efficiently.
5. Why Choose Globule
One hygiene standard for the whole line
● : Globule conveyors share the same round-tube design, washdown standard and concealed-wiring approach as every other unit of the 2-in-1 Merging Line — not a single dead corner, passing FSMA audits at the first attempt.
We understand puffed food and your bags
● : with long-term experience serving potato-chip and corn-chip producers, we know how fragile those bags are, and every conveying detail is designed around smoothness and zero damage.
10+ years of engineering experience
● : our core team brings more than ten years in food conveying equipment and provides one-stop service from design and fabrication to installation and commissioning.
Modular and expandable
● : the conveyor is designed modularly, so future speed-up or capacity expansion costs the least change and the least money.
Fast response
● : local Shanghai manufacturing and technical support guarantee delivery schedules and after-sales service.
6. Contact Us
● Company: Globule Sanitary Conveyor Pty Ltd / Shanghai Lingan Equipment Manufacturing Co., Ltd.
● Email:
● Tel: +86 13818737877
● Address: No.28 Huiye Road, Songjiang District, Shanghai, China