Chain Conveyor Solutions for Efficient Handling

Contact me immediately if you encounter problems!

All Categories

chain conveyor

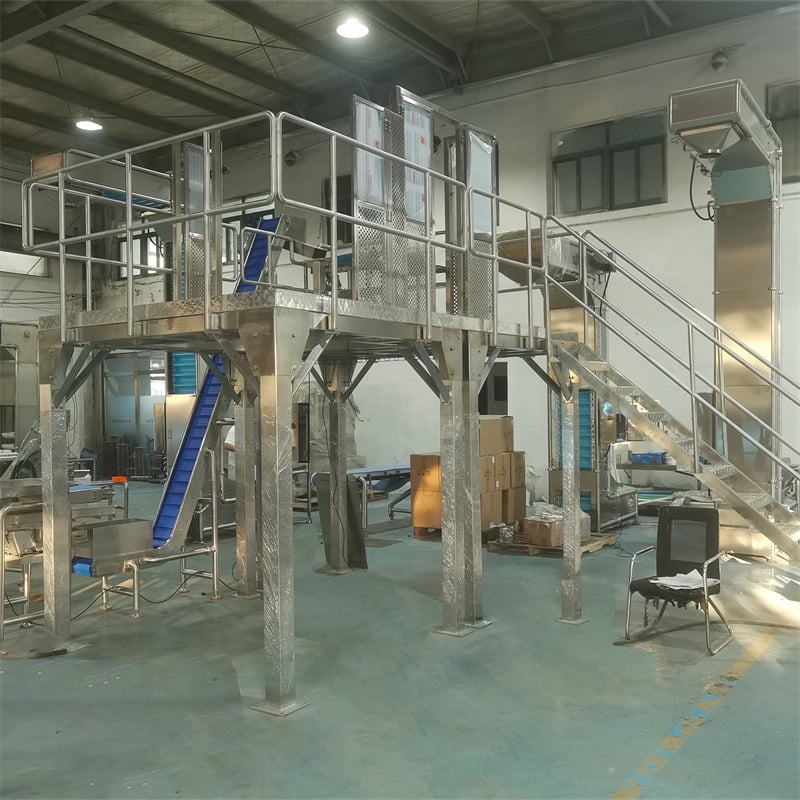
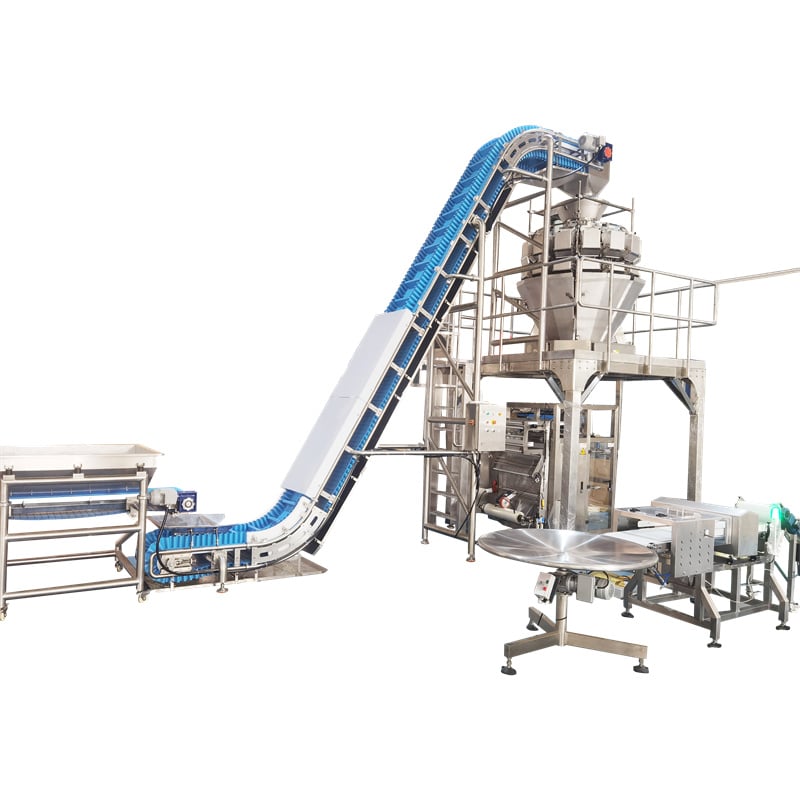
Chain conveyors offer many benefits for wholesale buyers. First, they are built to last. The strong chains can carry heavy loads without breaking. This is important because businesses need machines that won’t fail. For example, a factory that makes  cars needs to move heavy parts  like engines. A chain conveyor can  do this safely and quickly. Second, chain conveyors are very flexible. They can  be designed  to fit  different spaces and needs. Whether you need a straight line or a curved path, a chain conveyor can be made just for you. This means businesses can use them in many different ways.  Third, they  can save  time. With chain conveyors, items move  automatically from one place to another. Workers can focus on other important tasks instead of  moving items  by hand. This helps companies work faster and get more done.

Another great benefit is that chain conveyors can help reduce waste.  When  items move smoothly, there is less chance of them getting damaged. For example, fragile items like glass can be transported safely using a chain  conveyor. This means less money spent on replacing broken products. Furthermore, chain conveyors are usually easy to maintain. Most of the time,  a simple cleaning or lubrication is all that is needed to keep them running smoothly. This saves both time and money for businesses. Overall, chain conveyors from GLOBULE are a  smart choice  for wholesale buyers looking  to improve  their operations. If you are interested in exploring different types of conveyors, consider checking out our Packed spiral conveyor.
Our Products

What Are the Key Benefits of Chain Conveyors for Wholesale Buyers?

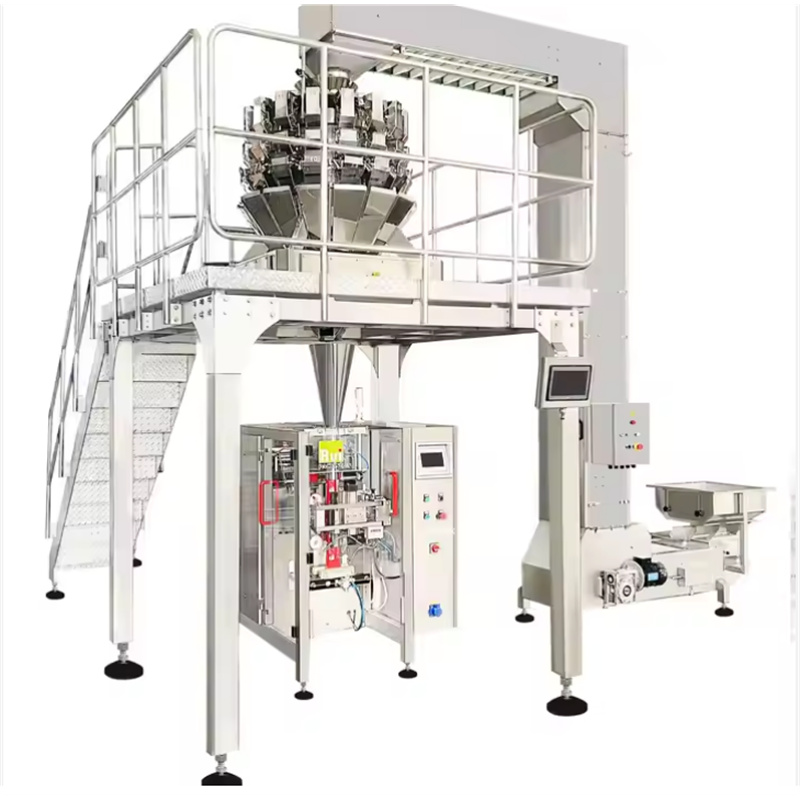
Chain conveyors are  important machines  used in factories and warehouses. They help move things from one  place to  another quickly and easily.  GLOBULE's chain conveyors are designed to make work faster and more efficient. In a  factory, workers often have to lift  heavy items and move  them around. This can take a lot of time and energy. With chain conveyors, items can be placed on the conveyor, and the machine moves them to where they need to go. This means workers  can focus on other important tasks  instead of just moving things. Additionally, our Z bucket elevator can complement your operations by providing vertical transport solutions.

While chain conveyors are very helpful,  they can sometimes have problems. One common issue is that the  chain can get loose or break. This can happen if the machine is not maintained properly. When the chain is loose, it can cause the conveyor  to  stop working. This is frustrating  for  workers and can  slow  down production. To avoid this,  it is important to regularly check the chain and tighten it when needed. GLOBULE  recommends setting up a maintenance schedule to keep everything running smoothly.

Frequently Asked Questions

What industries are chain conveyors suited for?

Our chain conveyors are designed for food and pharmaceutical production, delivering hygienic, FDA/FSMA-compliant material handling and gentle product transfer.
Yes. We customize length, chain type, flighting, speed, and sanitary features to meet specific product, layout, and regulatory requirements.
We use stainless steel and food-grade materials, with smooth finishes and corrosion-resistant components for durability and hygienic cleaning.
Conveyors feature open frames, sloped surfaces, minimal crevices, and easy-access panels to enable quick washdown and meet sanitary standards.
Yes. We offer system integration, installation guidance, validation support, and aftermarket service to ensure compliance and reliable operation.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Mobile
Message
0/1000

Related product categories

Where to Find High-Quality Chain Conveyors for Wholesale Purchase

Where to Find High-Quality Chain Conveyors for Wholesale Purchase

Another  problem that can occur is  that  items can  get stuck  on  the conveyor. This can happen if the conveyor is overloaded or  if the items are not placed correctly. When items get stuck, the whole system can back up, causing delays.  To fix  this, workers  should be  trained on  how to  load items  properly.  They should  also be  careful not to put too many items on the conveyor at  once. GLOBULE provides guides and training  sessions to  help workers understand how to use chain conveyors effectively.

How Chain Conveyors Improve Productivity in Manufacturing Processes

How Chain Conveyors Improve Productivity in Manufacturing Processes

Sometimes,  chain conveyors can  also make noise. If  a conveyor  is  noisy, it can be  a  sign  that something is wrong,  like a loose part or lack of  lubrication. This can be distracting for workers and may affect their ability  to  focus.  To solve this issue,  regular checks should be  made to ensure everything is in good condition. Adding oil to  moving parts  can also help reduce noise.  GLOBULE offers solutions and support to help businesses keep their  conveyors quiet and  efficient.

Common Usage Issues with Chain Conveyors and How to Resolve Them

Common Usage Issues with Chain Conveyors and How to Resolve Them

Finding  high-quality chain conveyors at good prices is  important for any  business.  GLOBULE offers durable  chain conveyors that are built to  last.  When looking for conveyors, it is important to consider quality first. Cheaper conveyors might save  money at first, but if  they break easily, they can end up  costing more  in repairs  and replacements. GLOBULE ensures that  their chain conveyors  are made  from  strong materials that can handle  heavy loads  and daily use without breaking  down.