EN

- Overview
- Competitive Advantage
- Recommended Products
Overview
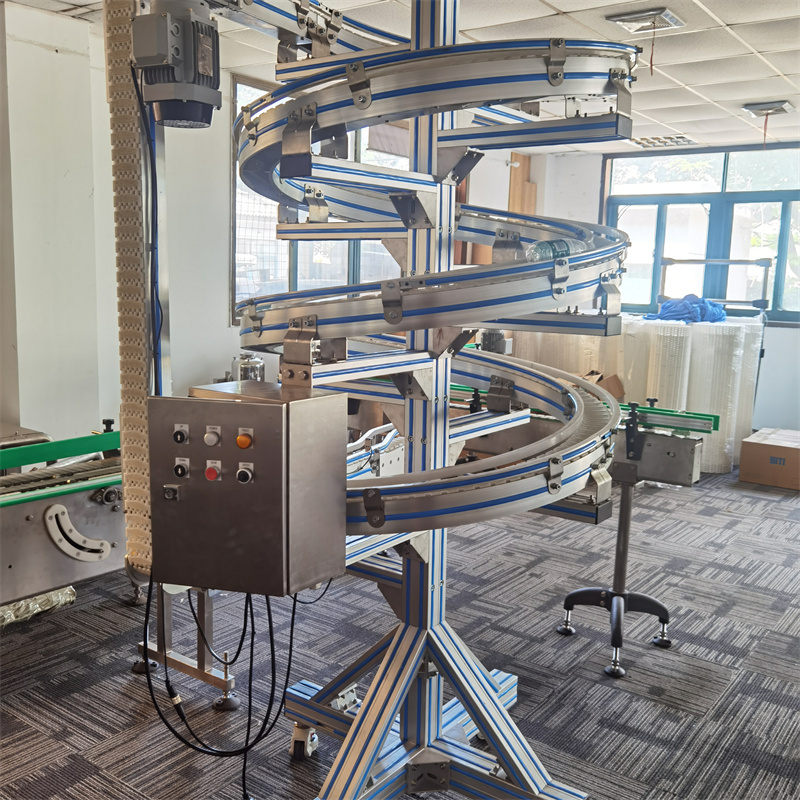
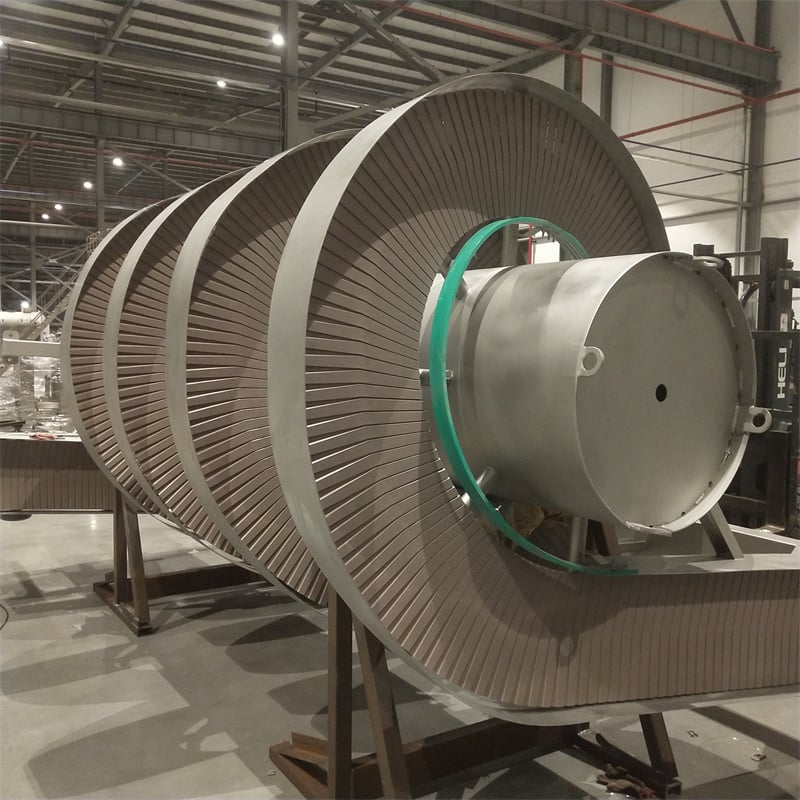
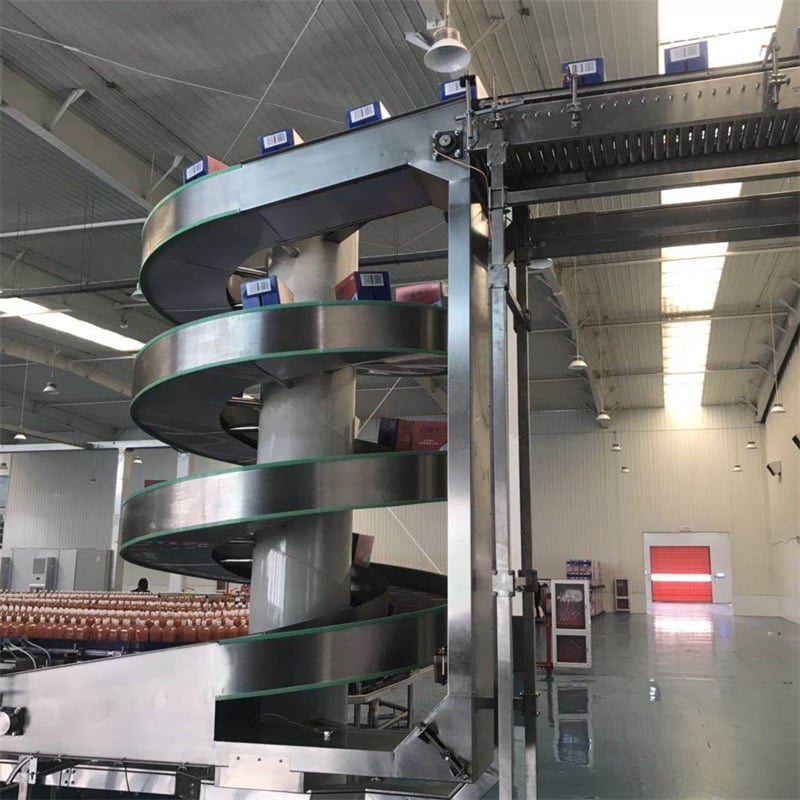
The Packed Spiral Conveyor market is currently experiencing a structural shift, growing at over 50% YoY on Alibaba.com—far outperforming traditional bulk screw conveyors. This surge is primarily fueled by the automation wave in e-commerce fulfillment centers and the pharmaceutical cold chain. Unlike standard belt conveyors, these systems provide a continuous, high-speed vertical flow for cartons, totes, and cases, allowing facilities to expand capacity upward rather than outward.
Data shows a Supply-Demand Ratio of only 13.14, indicating a significant scarcity of professional suppliers capable of delivering integrated packaging solutions. While the market is currently valued at ~USD 355 million, it is projected to hit USD 3.2 billion by 2034, with Europe and North America leading as high-growth regions due to escalating land and labor costs.
Competitive Advantage
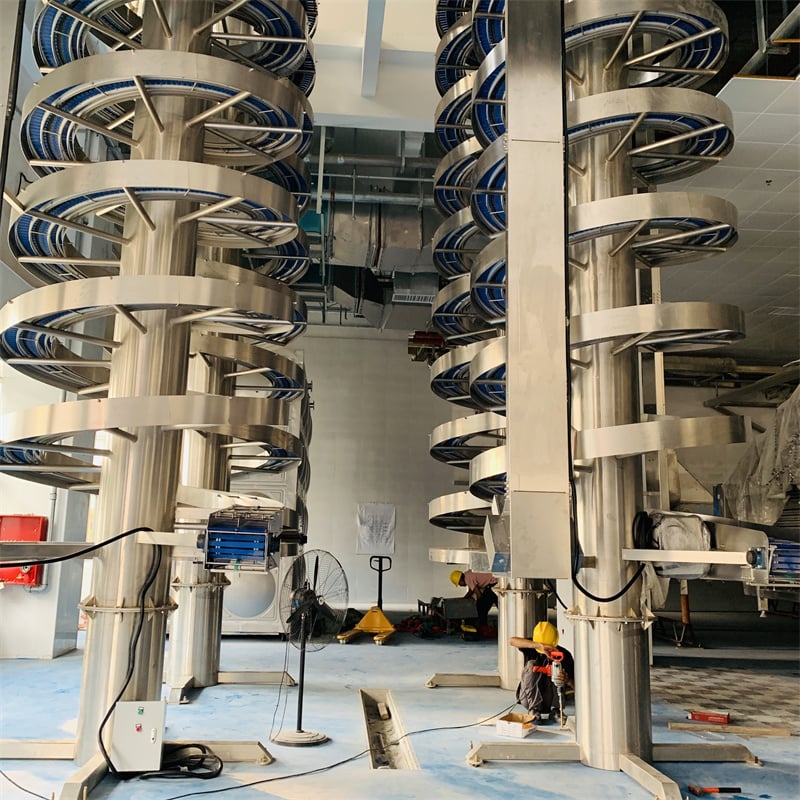
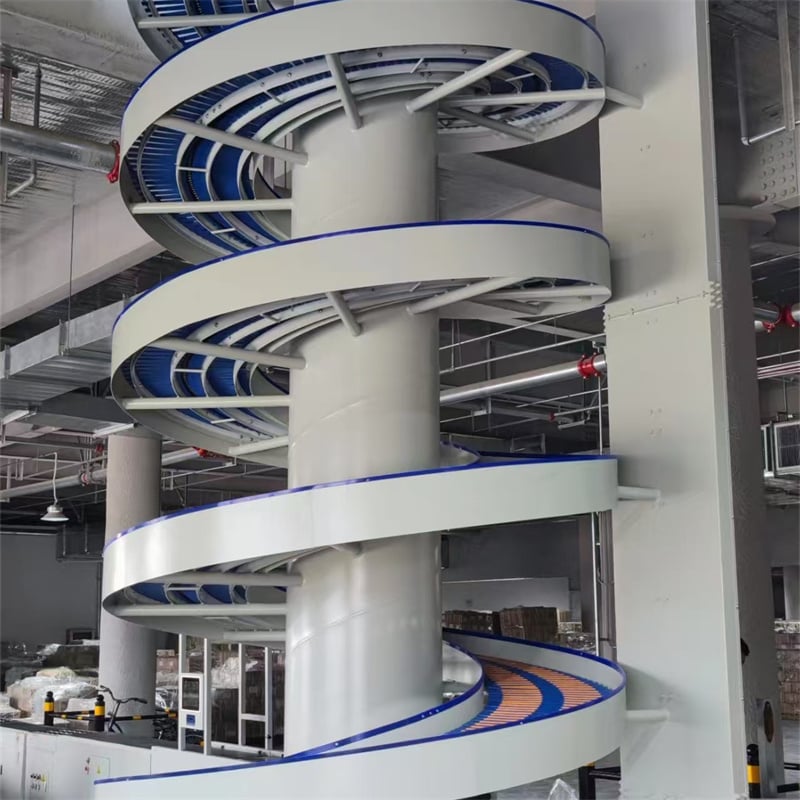
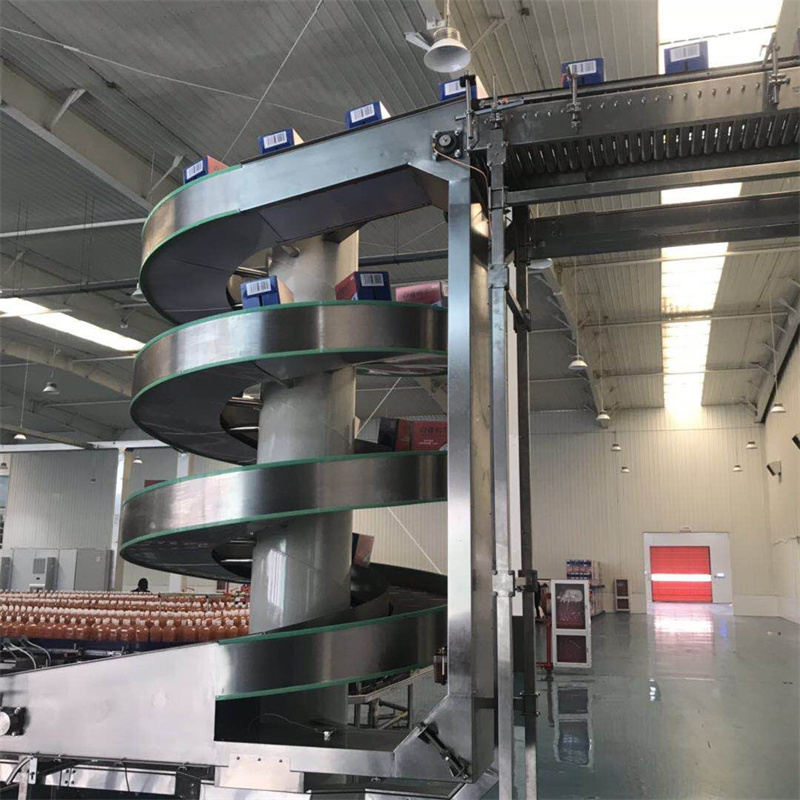
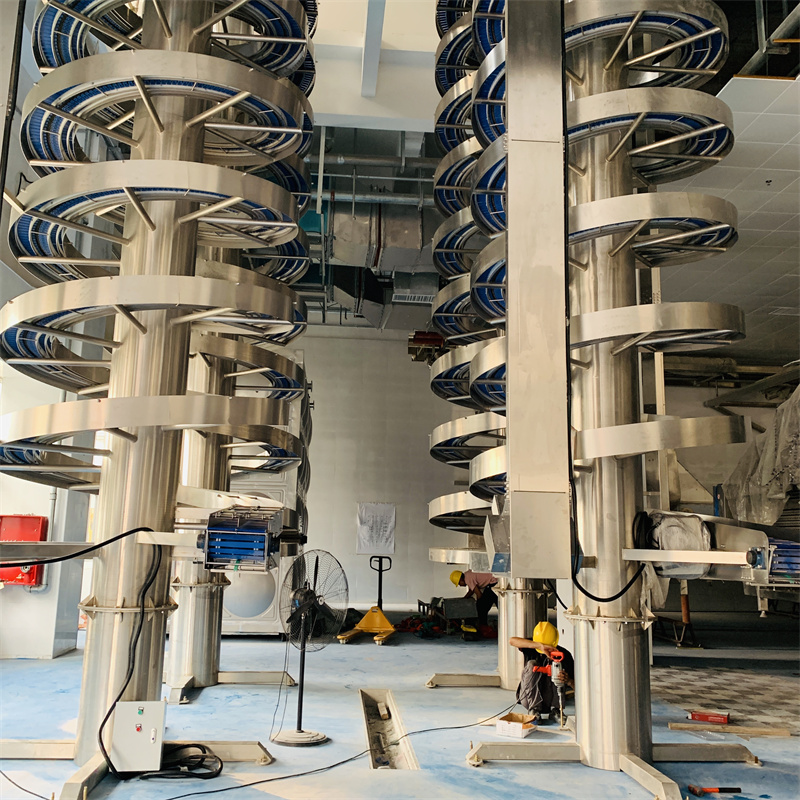
Vertical Space Maximization: Replaces long, sprawling inclined conveyors with a compact footprint, saving up to 80% of floor space. This is a decisive ROI factor for high-rent urban logistics centers.
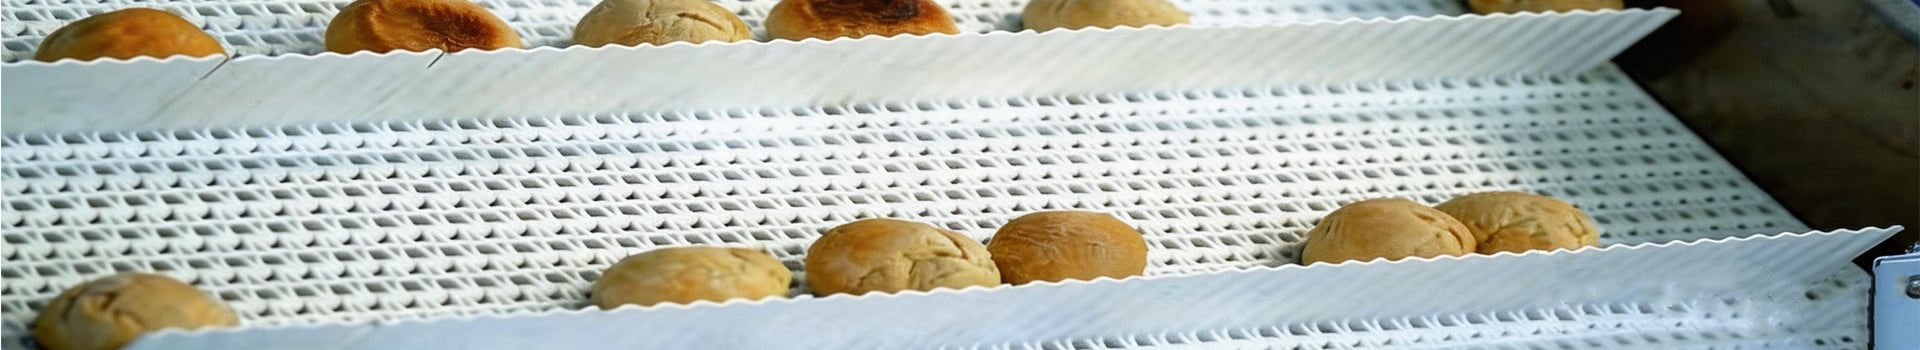
Superior Product Protection: Unlike traditional vertical elevators that "stop-and-start," the continuous slat-type surface ensures that packaged goods (even fragile boxes) move smoothly without tipping, vibration, or jamming.
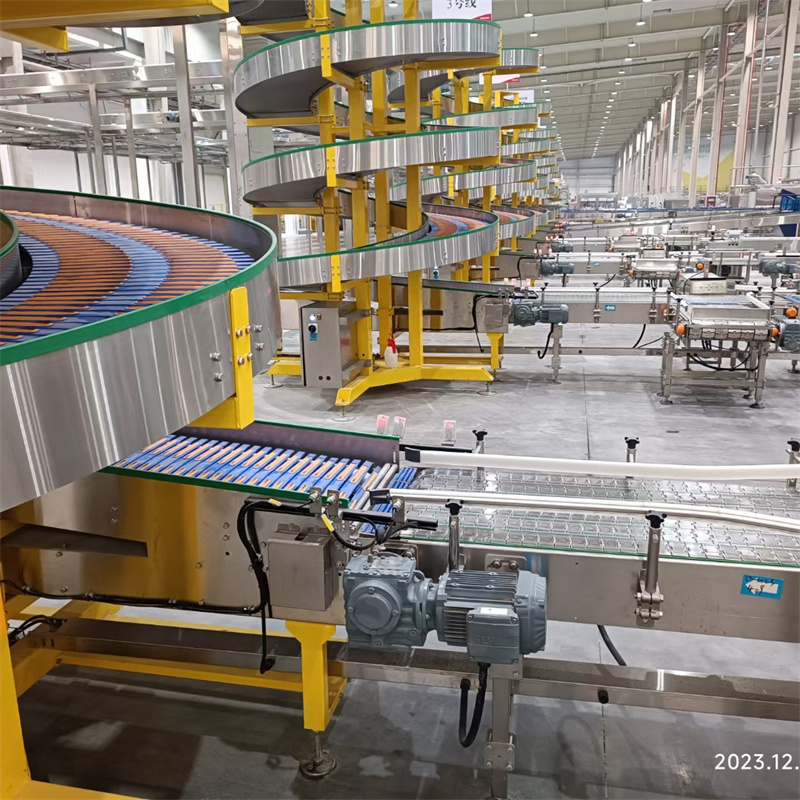
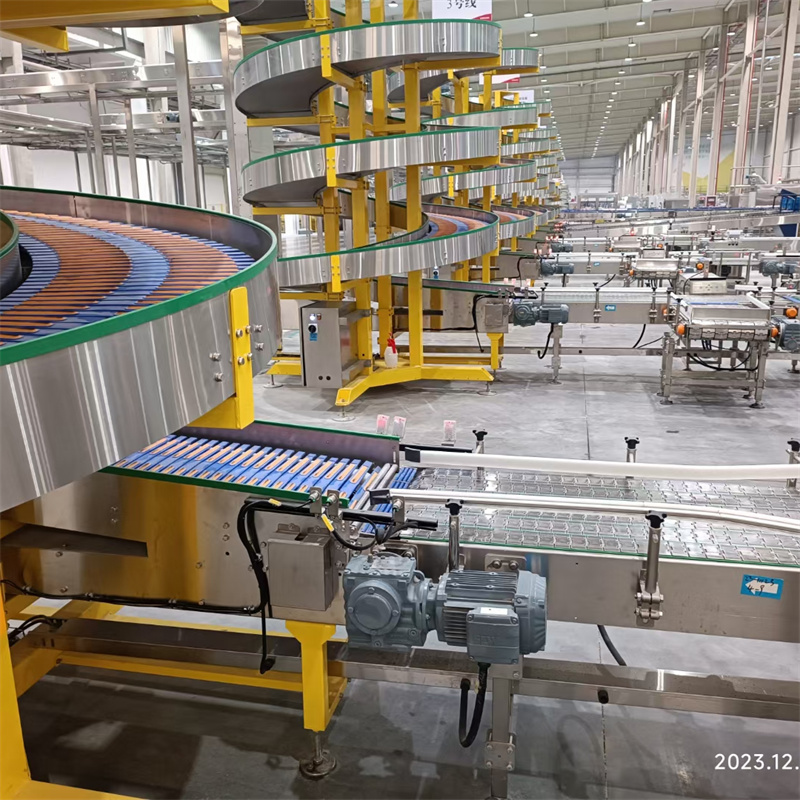
High Throughput & Reliability: Engineered for 24/7 operation with throughput capacities exceeding 2,000-3,000 cases per hour. The single-drive motor design reduces energy consumption by 30-50% compared to multiple belt stages.
Modular & Scalable Design: System segments can be added or rearranged based on floor height changes or layout reconfigurations, drastically reducing engineering and installation costs for long-term upgrades.
Washdown & Cold-Chain Compatibility: Specialized models offer SS304/SS316 frames with IP65-rated motors, ensuring compliance with FDA hygiene standards for food processing and structural stability in -25°C freezers.