EN

- Overview
- Competitive Advantage
- Recommended Products
Overview
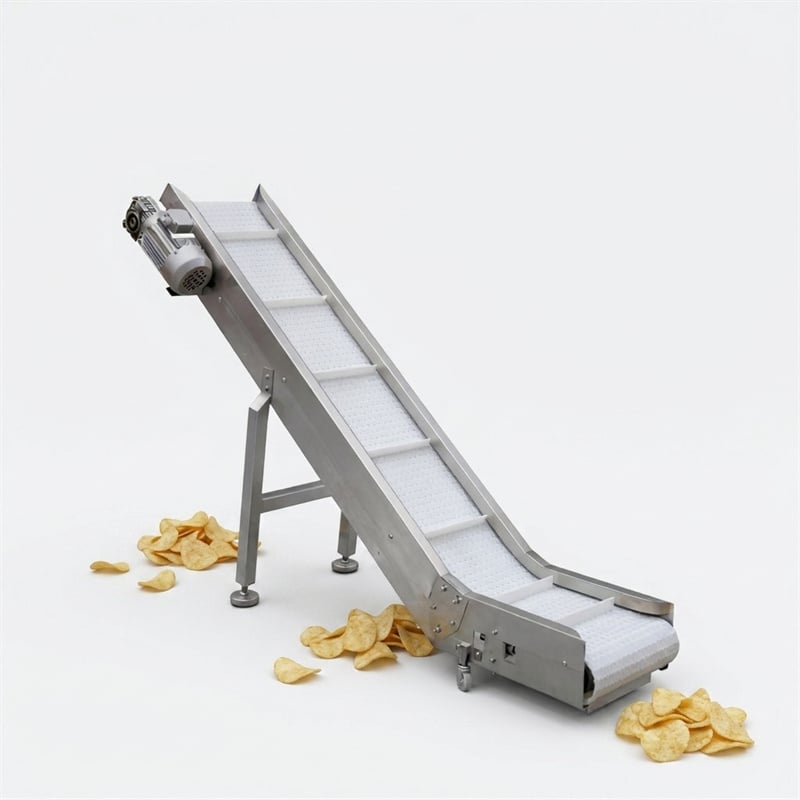
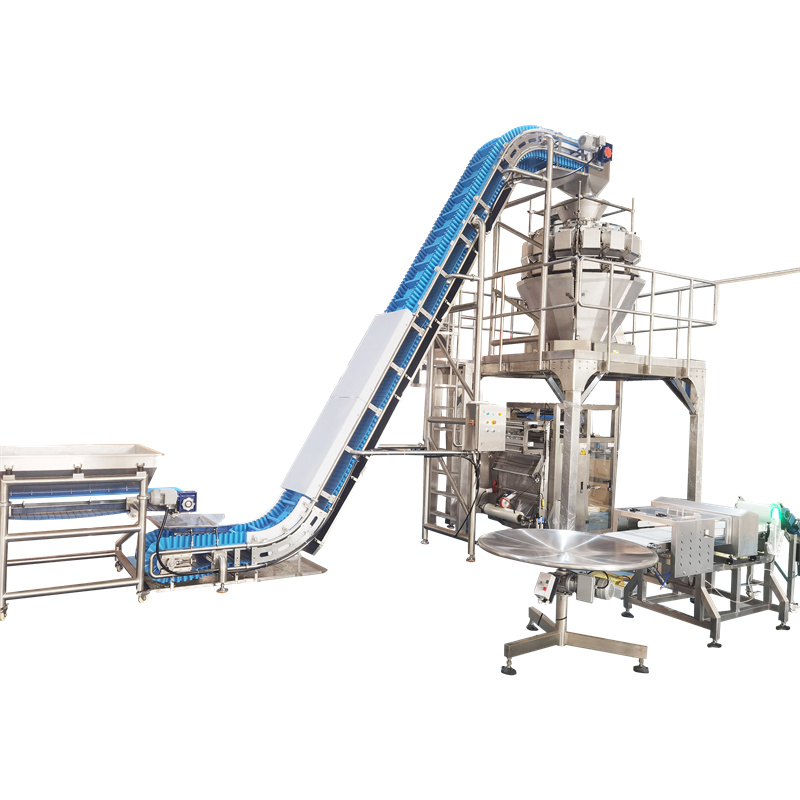
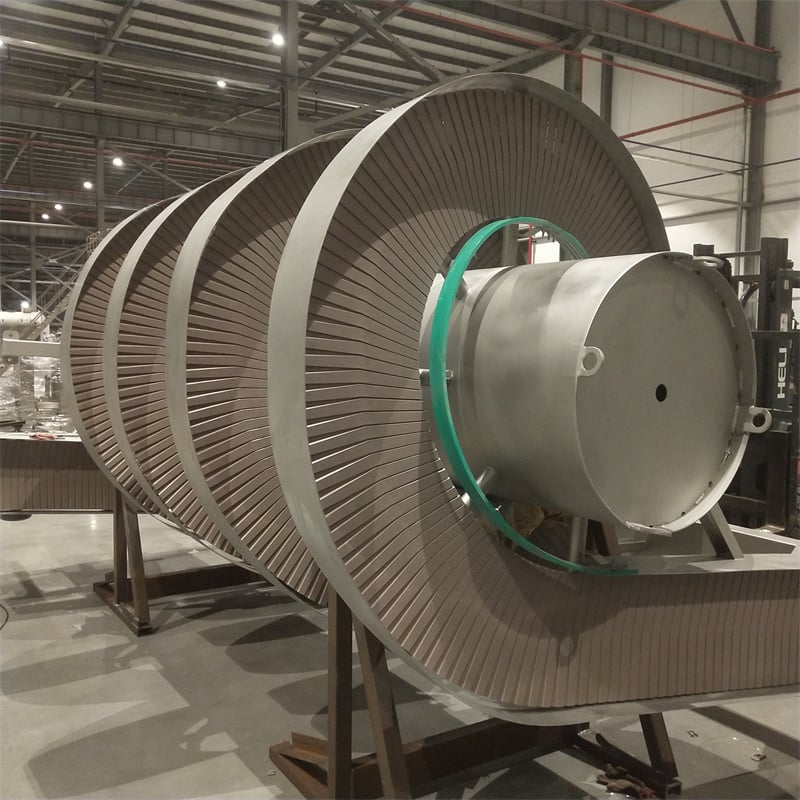
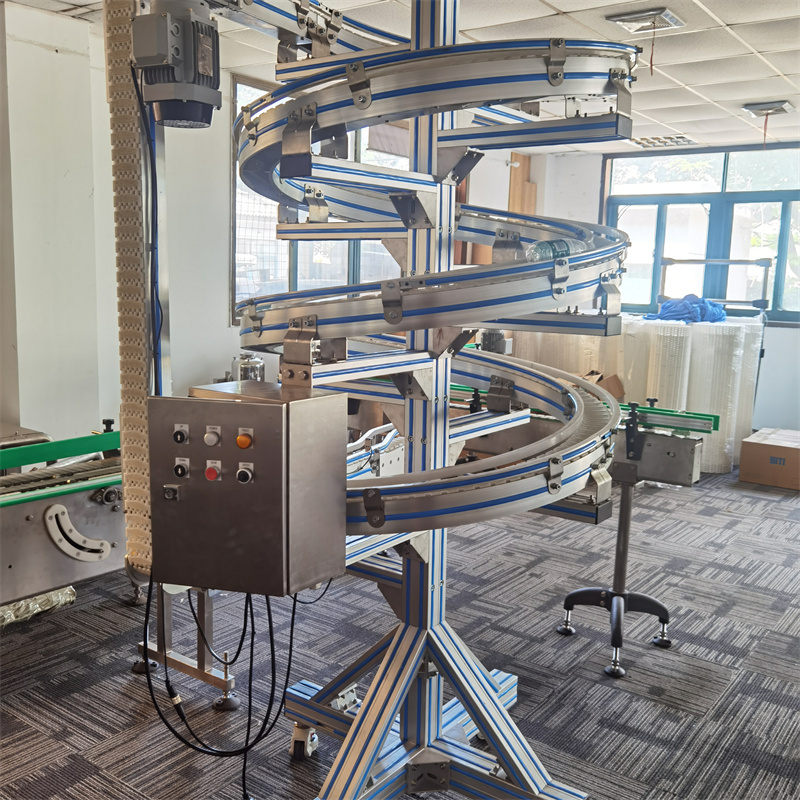
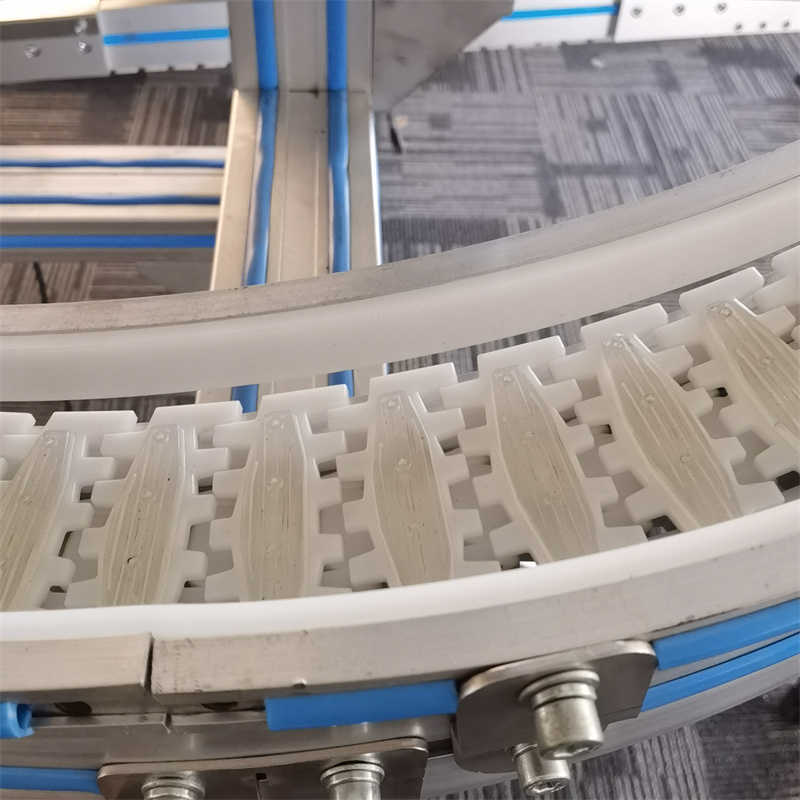
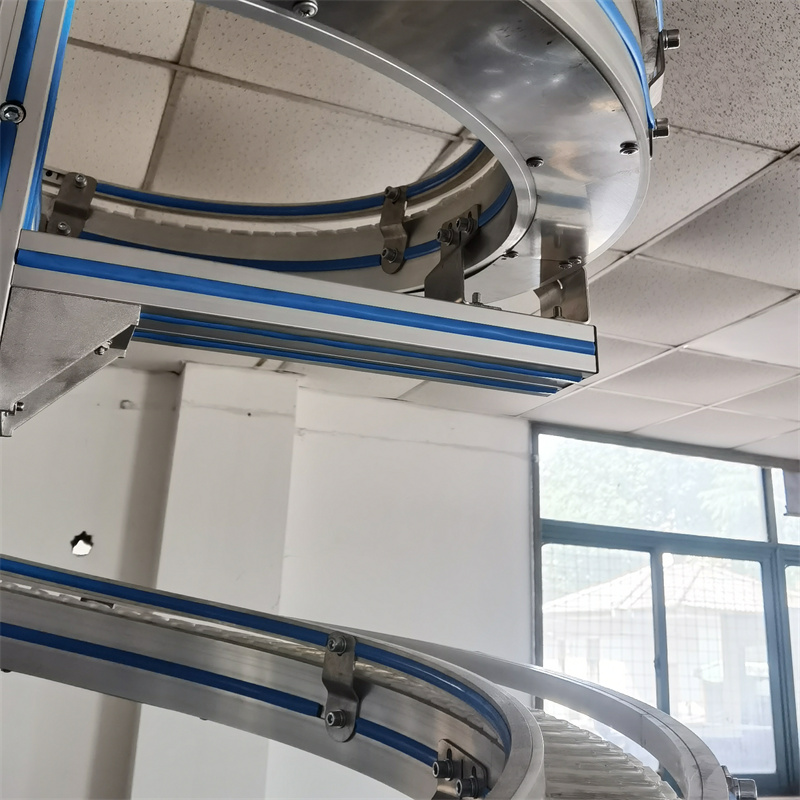
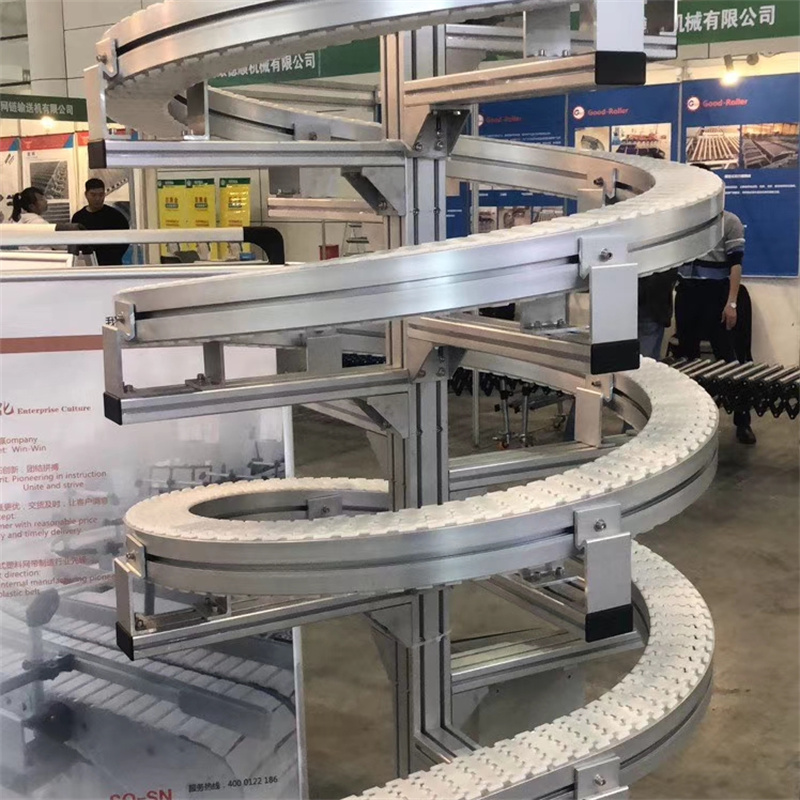
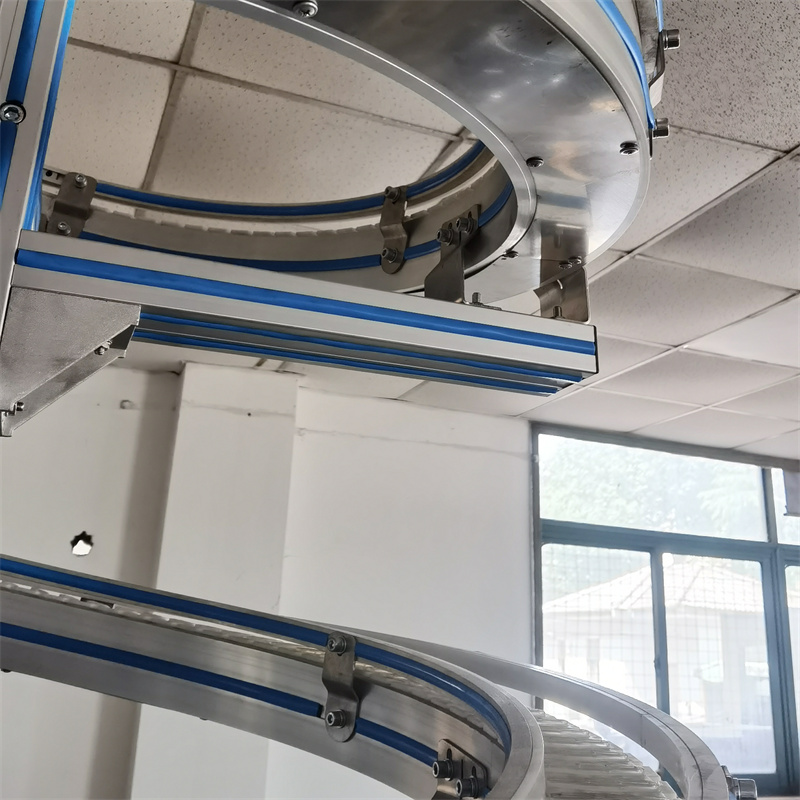
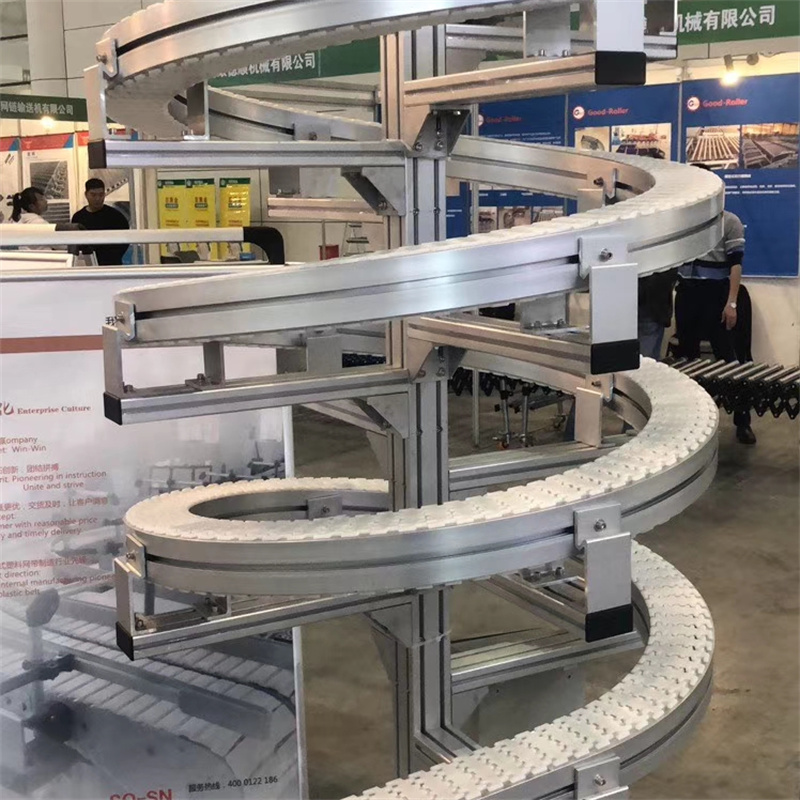
The Spiral Flexible Conveyor is a high-performance vertical and curvilinear transport solution designed to maximize floor space and streamline production flows. Unlike traditional flat-bed conveyors, these systems utilize a continuous spiral path to move goods (from powders and grains to packaged boxes) between different elevations or through tight plant layouts. Currently, the global market is valued at approximately USD 305 million, with a steady CAGR of 5.7% projected through 2032.
Key demand is driven by the rapid automation of warehouse logistics and the stringent hygiene requirements in food and beverage processing. In the Alibaba.com ecosystem, while the supplier base is concentrated in China's industrial hubs (like Henan and Shandong), there remains a significant "blue ocean" opportunity for high-precision, shaftless, and food-grade certified (FDA/CE) models.
Competitive Advantage
Extreme Space Efficiency: Save up to 60-75% of floor space compared to traditional inclined conveyors. Its compact footprint allows for vertical elevation changes within a minimal radius, making it ideal for crowded production lines.
Handling "Difficult" Materials: Specialized Shaftless designs excel at moving sticky, sluggish, or stringy materials that typically clog traditional screw conveyors. Enclosed tube options also prevent dust leakage and cross-contamination.
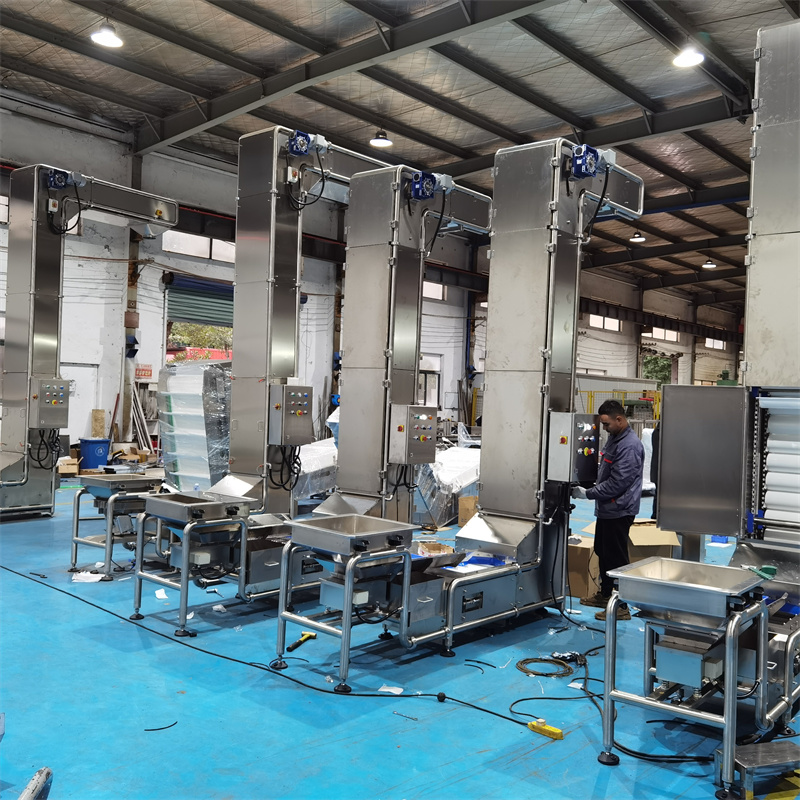
Low Total Cost of Ownership (TCO): The modular design and high-strength spiral segments allow for individual part replacement rather than full system overhauls. This significantly reduces downtime and maintenance labor costs.
High Throughput & Flexibility: Supports multi-entry and multi-exit configurations. Variable speed controls and continuous movement ensure a steady flow of goods without the "stop-and-start" bottlenecks common in industrial elevators.
Environmental & Safety Compliance: Fully enclosed systems protect both the product from contamination and the workspace from noise and dust, aligning with modern ESG and safety standards (GMP/Industry 4.0).