EN

- Overview
- Recommended Products
Overview
1. Product Overview
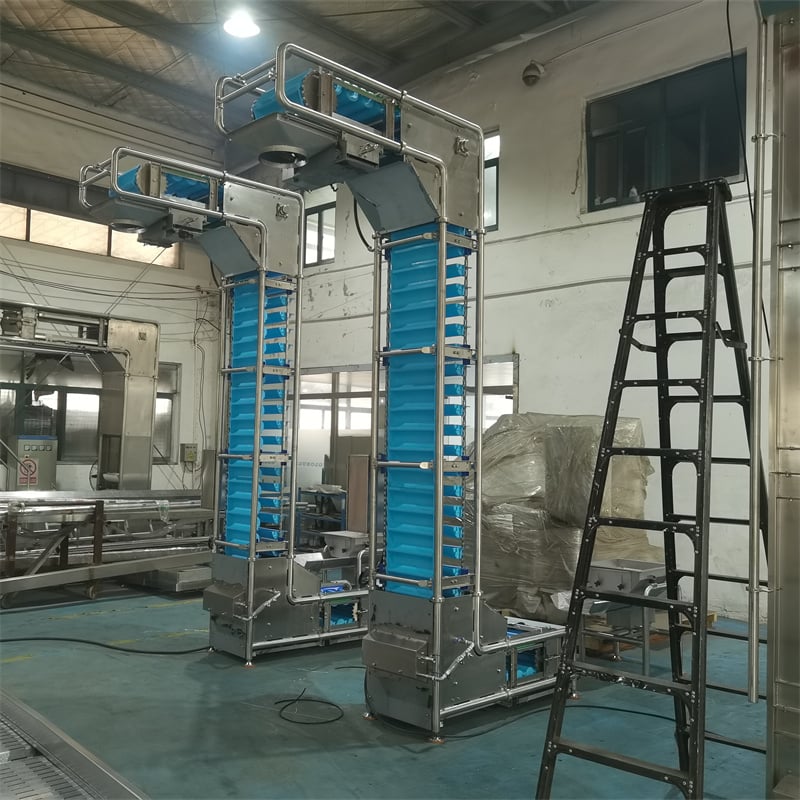
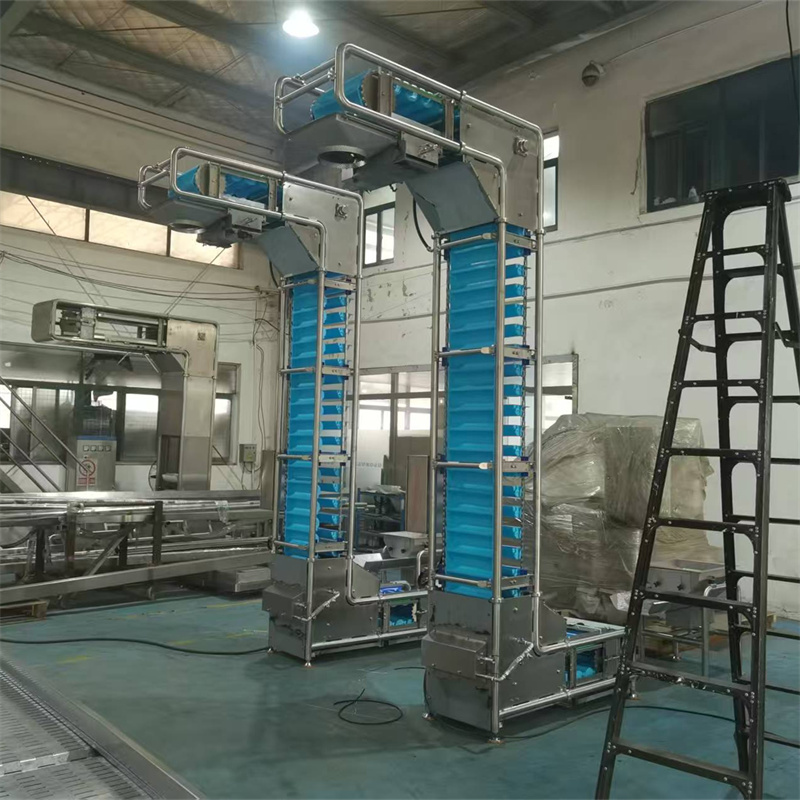
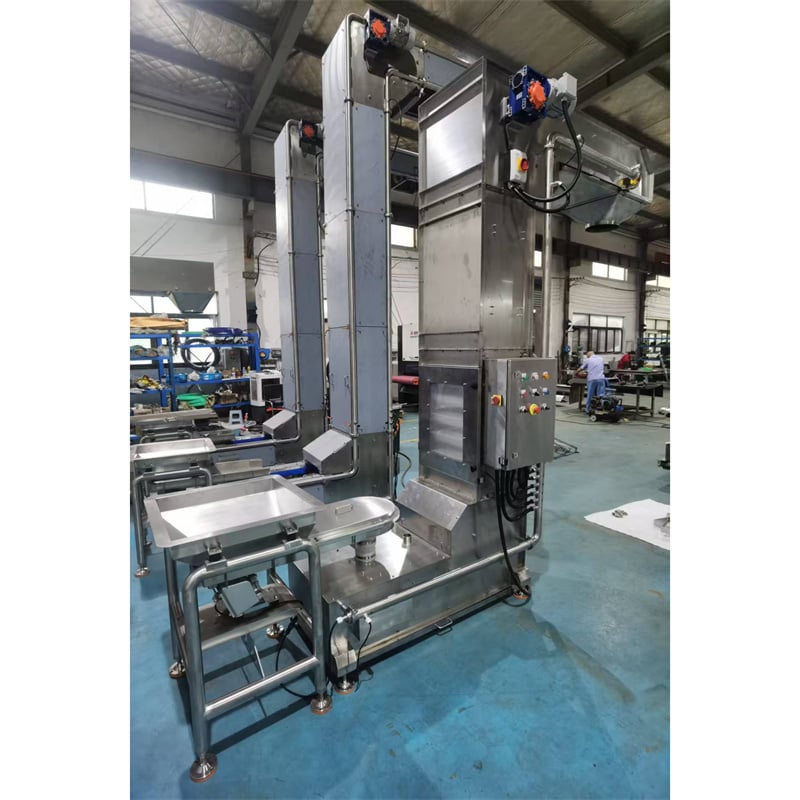
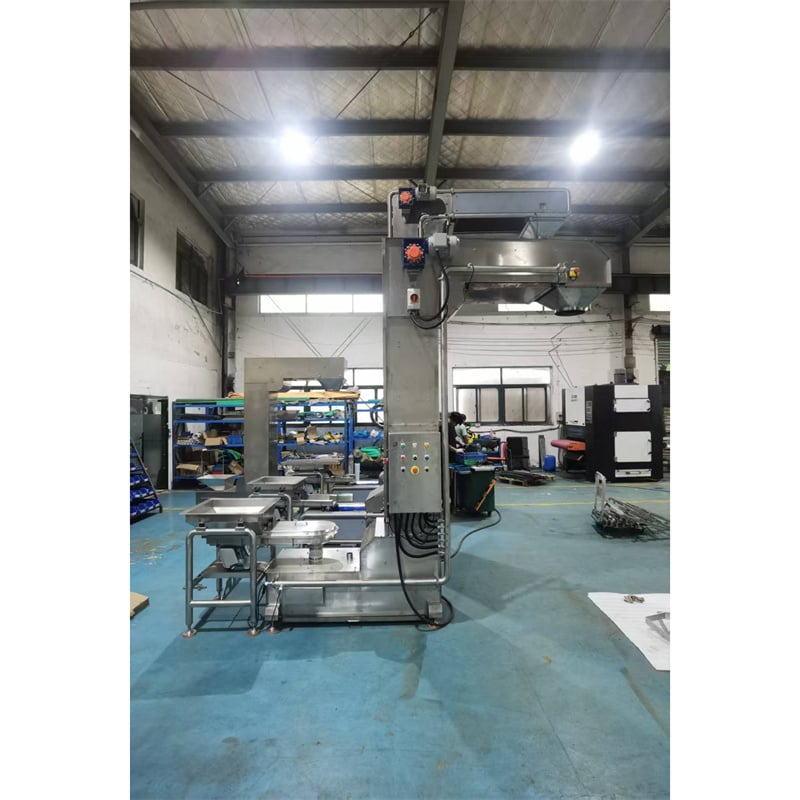
The Bucket Elevator is the continuous-feeding machine that handles "large-vertical-lift" transport on a puffed-snack packaging line. In a typical puffed-snack plant, bulk product is produced at ground level or at a low-level process stage, while the high-speed weighing and bagging station — the multihead weigher and vertical bagging machine — stands on a mezzanine or elevated frame. The product must be carried from low to high in the shortest time and at the greatest continuous flow. This machine runs a train of food-grade buckets in a continuous high-speed loop along an enclosed or semi-enclosed track: it scoops chips, popcorn, nuts and other puffed products at the intake, lifts them vertically, and tips them out at the top, delivering high-speed, single-line, continuous feeding.
Unlike the twin-line parallel configuration used in the two-in-one category, this machine is designed for high-speed single-line production: one bucket elevator serves one high-speed puffed line, and its feeding rhythm is designed entirely around that line's multihead-weigher take-up cadence. Shanghai Linguan Equipment Manufacturing Co., Ltd. (Globule Sanitary Conveyor Pty Ltd) designs the bucket elevator and the same-line quick-return conveyor as one interlocked unit — the elevator keeps product flowing up while the quick-return conveyor sends excess or returned product back to the front in a controlled way. The two are interlocked in rhythm, so the single line is always "well fed" yet never "overstocked".
2. Position in the Puffed-Snack Packaging Line
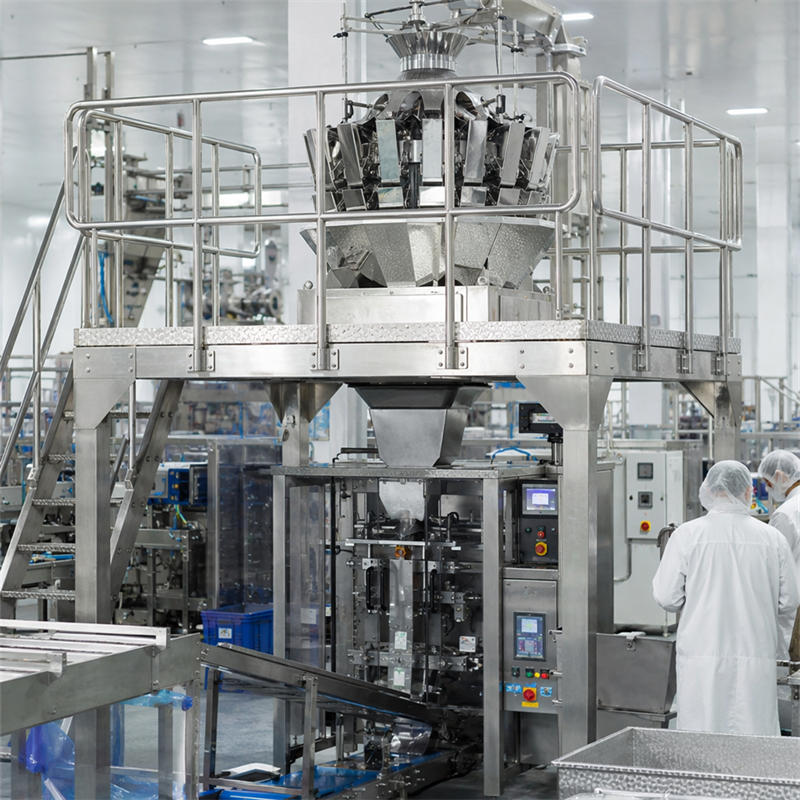
In the layout of a high-speed single-line puffed line, the bucket elevator is placed at the key node where product must cross floors or a large height difference:
Low-level intake
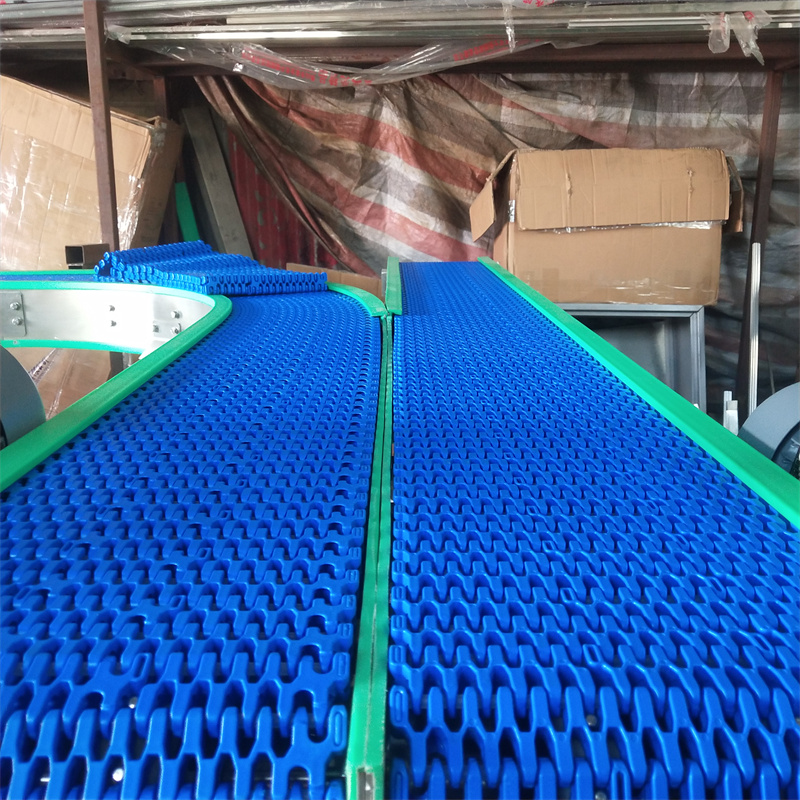
● : it receives bulk product from the inclined conveyor, the modular belt conveyor, or directly from the fryer/seasoning discharge;
Vertical elevation
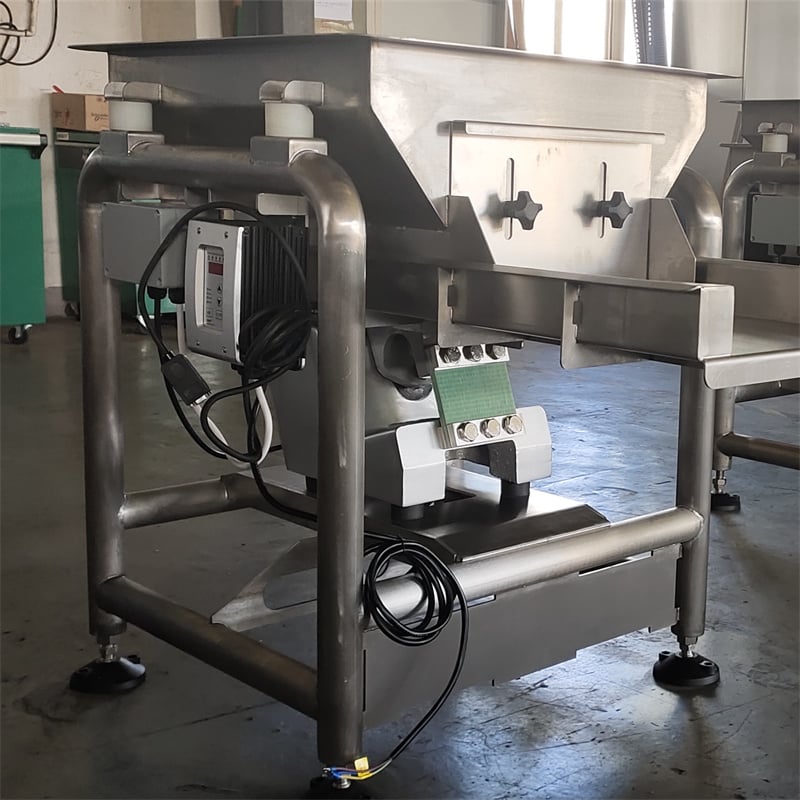
● : it lifts the product continuously and at high speed into the elevated buffer hopper, which feeds the vibrate feeder and multihead weigher;
Rhythm coordination
● : the discharge flow at the top matches the dosing frequency of the multihead weigher, and surplus product is routed by a bypass into the quick-return conveyor, which returns it to the front for redistribution — keeping the whole single line in material balance.
This "single-line continuous feeding plus quick-return" organisation keeps a high-speed line free from interruption, waste and blockage even when the multihead weigher takes product frequently and occasionally overflows.
3. Core Advantages: High-Speed Single-Line Continuous Feeding
1. High-speed continuity — the single line never starves. Buckets circulate continuously at a fixed pitch, and the lifting speed and bucket volume are matched to the maximum dosing frequency of the multihead weigher, so the elevated hopper always holds product. Even at maximum combination frequency the elevator keeps the scale "full and on pace", and single-line capacity is never compromised.
2. Rhythm matching with the quick-return conveyor. This is the machine's core coordination logic on a puffed single line: a level sensor between the elevator top and the buffer hopper detects full condition, and surplus product is routed through a bypass into the quick-return conveyor, which sends it back to the line head or a distribution point at a controlled speed. The elevator output and the quick-return speed are interlocked and adjusted together, so the system balances itself automatically under both high-yield and overflow conditions — preventing the pile-up and re-lifting that crush fragile product.
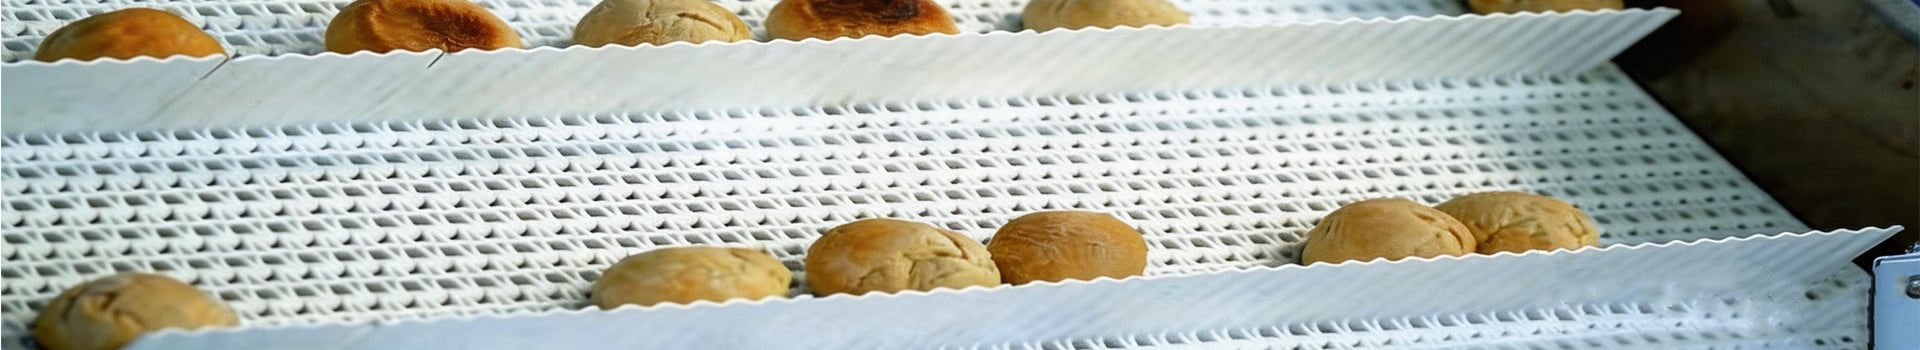
3. Gentle scooping that reduces breakage. Puffed snacks are fluffy and fragile. The buckets use food-grade material and generous radii, and the scooping and tipping paths are optimised to reduce knocking during loading and discharge. A cushioned discharge option is available for sheet-type products such as chips, minimising breakage at the elevation stage.
4. Enclosed hygiene — no foreign matter or dust. The casing is a sealed food-grade stainless steel structure that prevents product from dropping, splashing or being contaminated by the environment during lifting. Top venting and cleaning ports make routine sanitation easy, meeting the high hygiene grade required by puffed snacks.
4. Structure and Hygienic Design
Food-grade stainless steel casing and buckets
● : all product-contact parts are food-grade stainless steel with radiused transitions and weld-free dead corners, complying with FSMA hygienic design criteria;
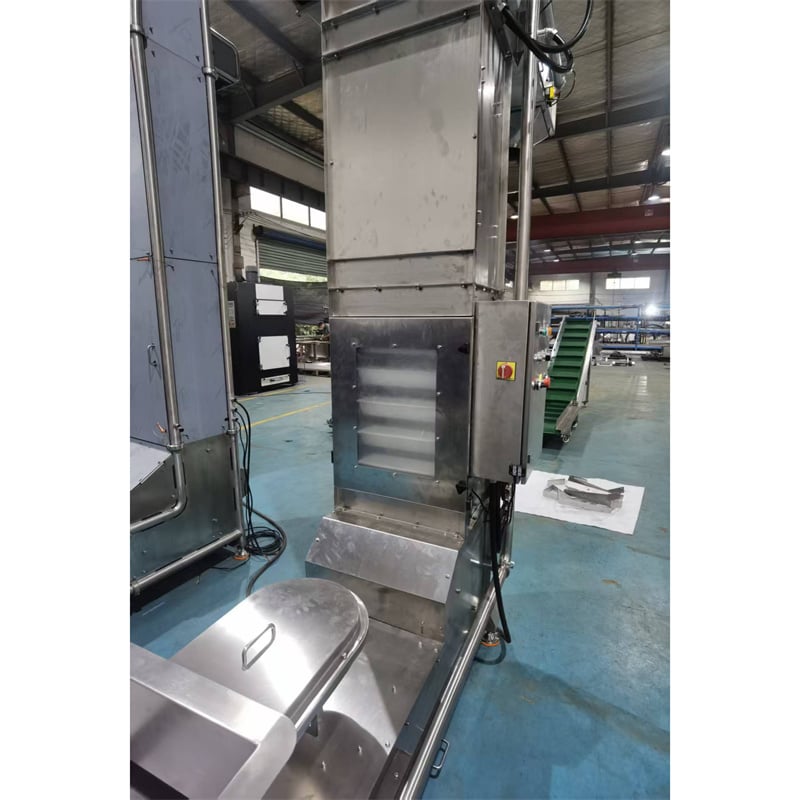
Quick-access inspection doors
● : the casing has quick-opening doors so the buckets, chain and sprockets can be inspected without dismantling the machine;
Fully washable
● : waterproof electrics and concealed wiring allow high-pressure hose-down of the casing and buckets;
Safety protection
● : overload protection, anti-runback device and top covers are fitted; motors and drives are fully guarded for safe and reliable operation;
Compact footprint
● : vertical elevation takes almost no horizontal space, ideal for multi-floor, wall-side installation.
5. Technical Specifications
| Parameter | Value / Option |
| Feeding mode | High-speed single-line continuous feeding |
| Lifting form | Vertical / steep-angle (customised to site) |
| Bucket material | Food-grade stainless steel (large radii, breakage-reducing design) |
| Casing material | Food-grade stainless steel, sealed against dust |
| Coordinated equipment | Quick-return conveyor (rhythm interlock) |
| Protection | Overload protection, anti-runback, quick-access doors |
6. Integration with the Whole Line
The Bucket Elevator is the key element of the "vertical feeding plus quick-return circulation" closed loop on a high-speed single-line puffed system. Upward, it feeds the elevated buffer hopper, the vibrate feeder and the multihead weigher; downward, it works with the quick-return conveyor to send overflow and returned product back to the line head in a controlled way, forming a complete material-circulation network together with the inclined conveyor and modular belt conveyor; on the finished side, the vertical bagging machine, take-off conveyor and metal-detector/checkweigher combo unit complete bagging and inspection. Globule programmes the whole electrical control system, interlocking the elevator start/stop and speed with the quick-return conveyor and the weigher's hopper-level signals, so supply and demand stay balanced during high-speed continuous production.
7. Suitable Products and Conditions
● Vertical elevation of sheet-type puffed snacks such as potato chips and shrimp crackers;
● Round light products such as popcorn and corn balls (cushioned, breakage-reducing discharge);
● Bulk nuts and mixed kernels;
● High-speed single-line scenarios crossing floors or large height differences with demanding continuous feeding.
8. Quality and Service
Shanghai Linguan Equipment Manufacturing Co., Ltd. was founded in 2019, and our engineering team has more than ten years of experience in food conveying equipment, strictly following FSMA hygienic design criteria. The Bucket Elevator's height, bucket pitch and speed can all be customised to the single-line cadence, with unified electrical control and interlock logic across the whole line. We provide full drawings, hygiene documentation, bilingual operation manuals, on-site installation and commissioning, and remote maintenance support — so your puffed single line "lifts high, feeds steady and returns fast".