EN

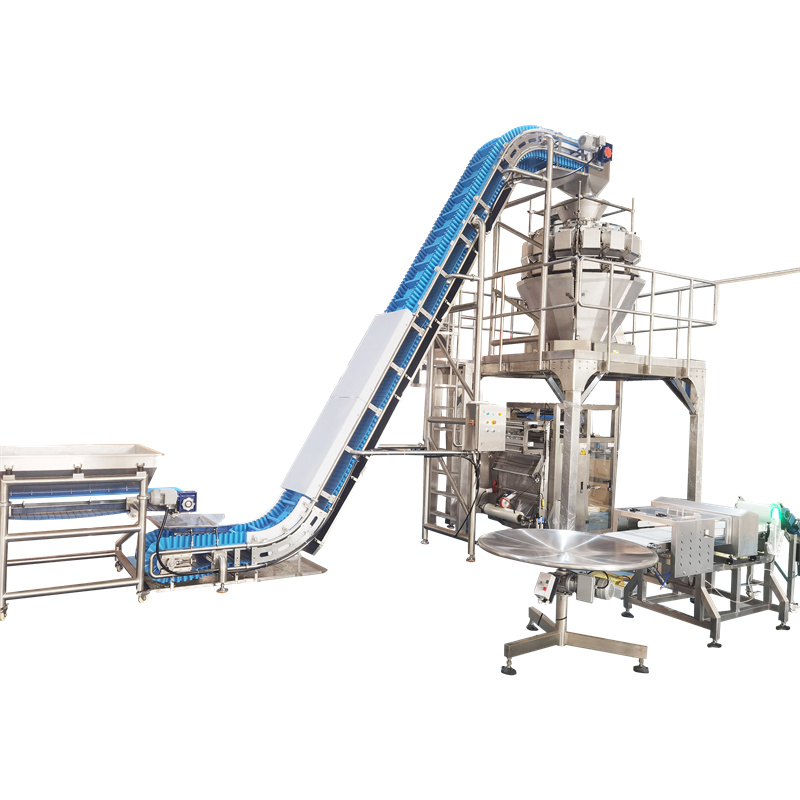
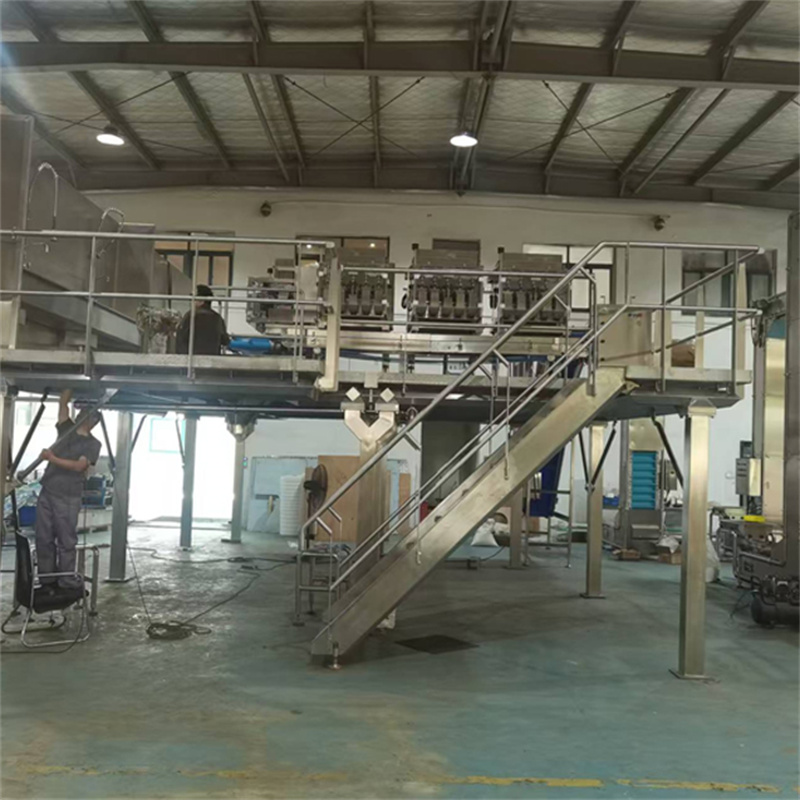
Hopper conveyor systems are an important part of moving materials in factories and warehouses. They help transport items from one place to another quickly and easily. GLOBULE specializes in making these systems. A hopper conveyor is a type of equipment that uses a large container, called a hopper, to hold materials. The materials can be anything from grain to small parts. Once the hopper is full, a conveyor belt moves the materials to the next step in the process. This allows workers to focus on other tasks, making the whole operation run smoother.
Wholesale buyers can enjoy several benefits when they choose hopper conveyor systems from GLOBULE. First, these systems make it easier to handle bulk materials. For example, if a company needs to move a lot of grains or powders, a hopper conveyor can hold large amounts and move them quickly. This means less time spent on moving materials and more time for other important tasks. Second, hopper conveyors are designed to reduce waste. With a proper system, materials are less likely to spill or get damaged during transport. This saves money for businesses because they won’t have to replace lost materials. Another benefit is that hopper conveyor systems are often customizable. GLOBULE offers different sizes and designs, so buyers can choose a system that fits their specific needs. Whether it’s for a small workshop or a large factory, there’s a right hopper conveyor for everyone. Lastly, these systems can improve safety in the workplace. By automating material handling, workers are less likely to get injured while lifting heavy items. This is very important in industries where safety is a priority. In summary, hopper conveyor systems help wholesale buyers save time, reduce waste, customize their setups, and keep workers safe. Additionally, GLOBULE offers a variety of options including the Z bucket elevator which is perfect for handling heavy materials.