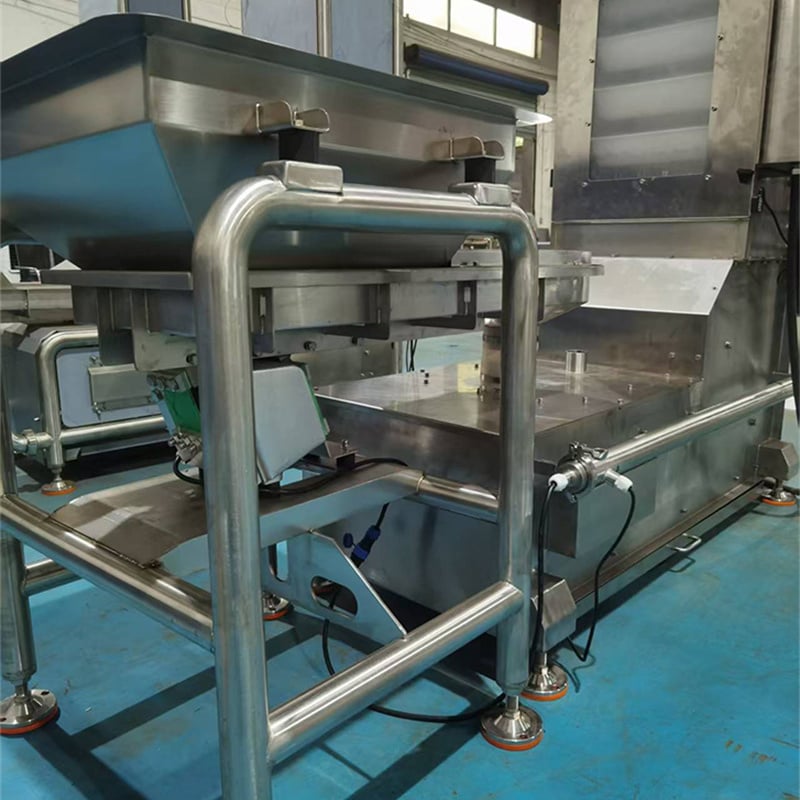
Mining Conveyor Belt for Efficient Material Handling

Contact me immediately if you encounter problems!

All Categories

mining conveyor belt

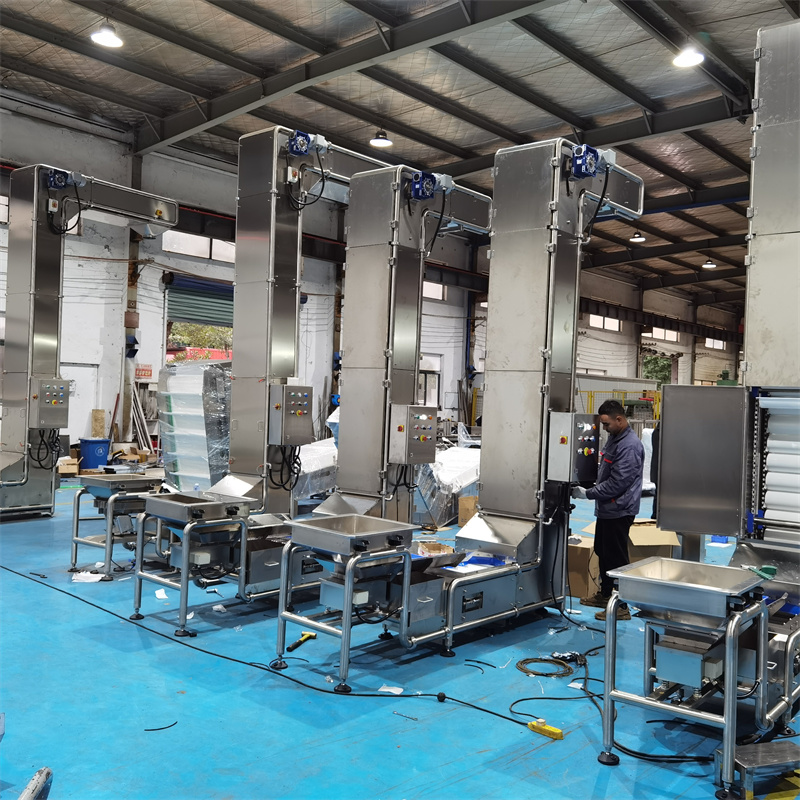
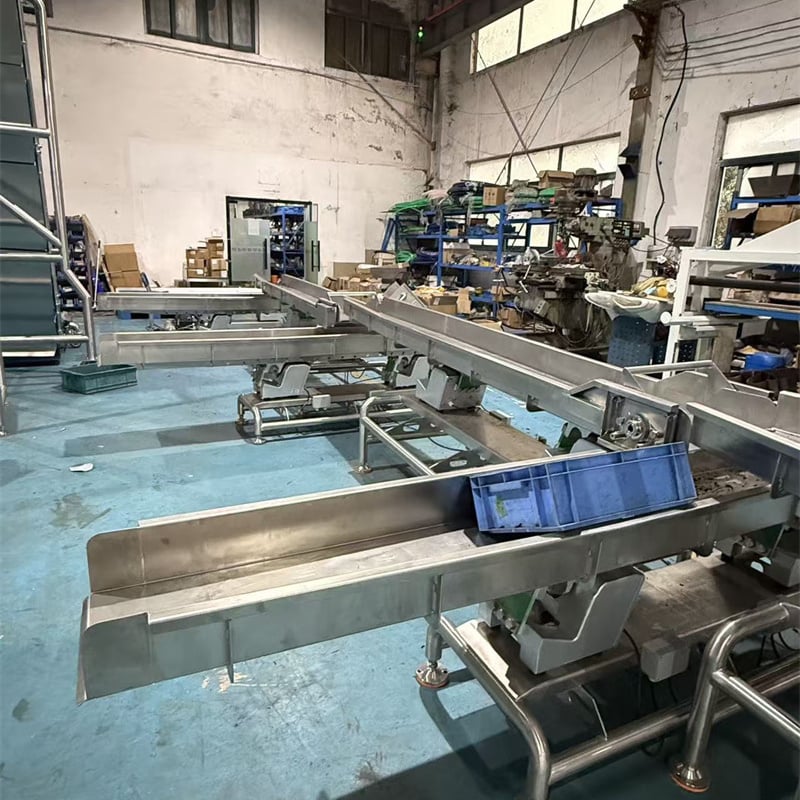
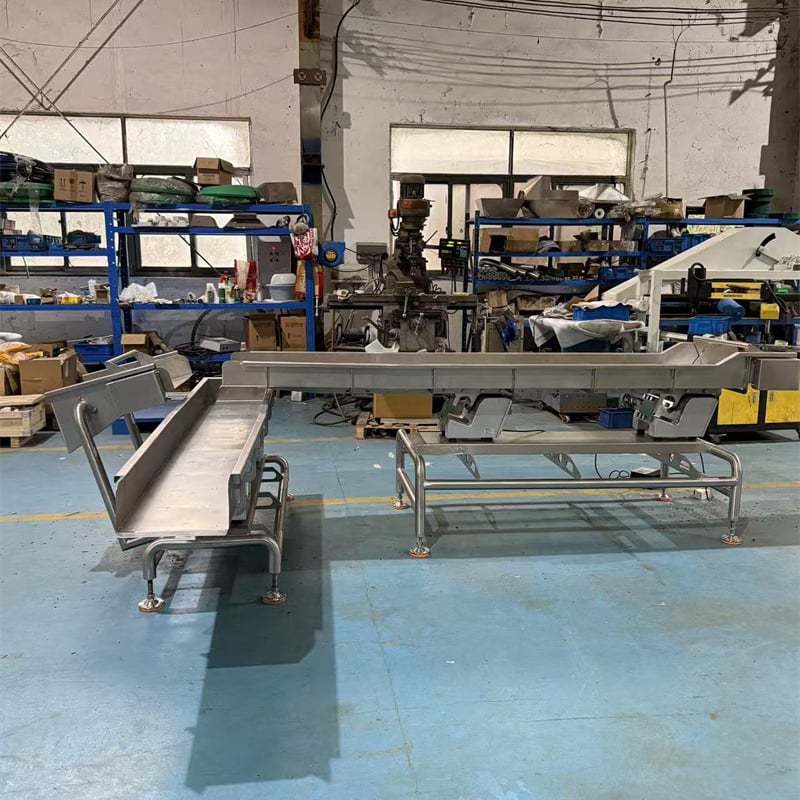
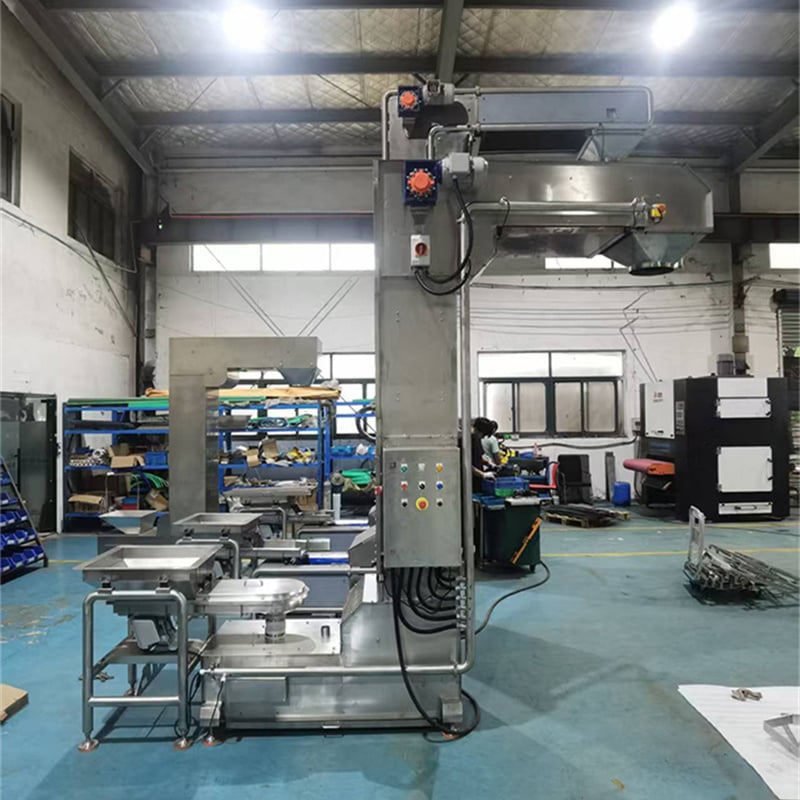
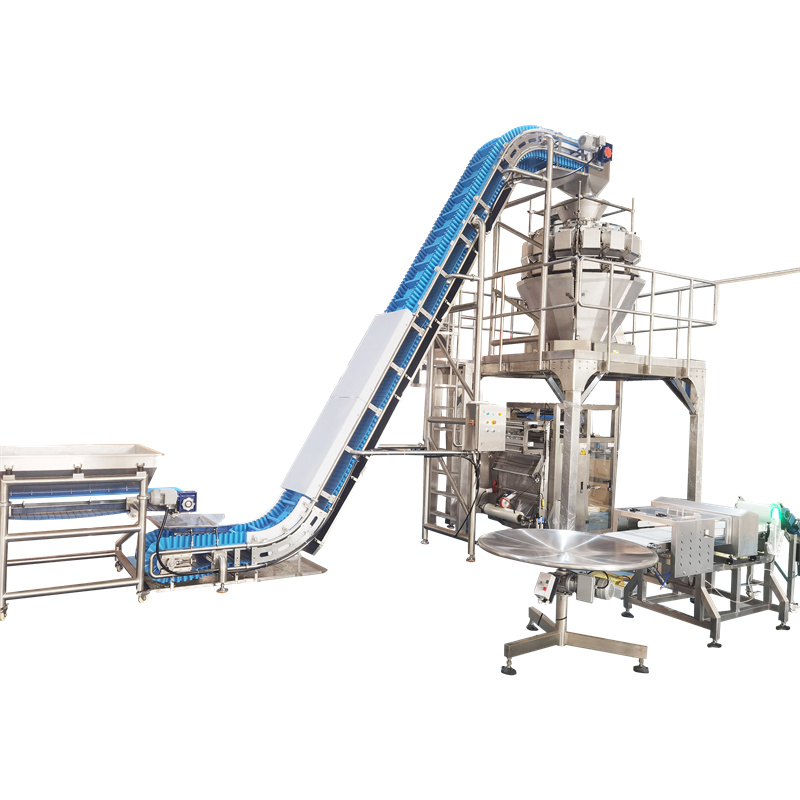
Mining conveyor belts are  very important in the world of mining. They help move materials like coal, minerals, and rocks from one place to  another. Imagine a long belt that carries heavy loads without needing a lot of people to  do the work. This makes mining much easier and faster. Conveyor belts are  made strong so they can handle rough materials. They are also designed to work in tough conditions, like  heat and dust. GLOBULE makes high-quality mining conveyor belts  that help businesses operate smoothly and efficiently. With these belts, workers can focus on other tasks while the materials are moved automatically. This not only saves time but also makes the workplace safer.

Mining conveyor belts offer many  great benefits for moving bulk materials. One of the  biggest advantages is efficiency. When  using conveyor  belts, materials can be moved quickly from one location to another without delays. This means that mining operations can keep running smoothly without stopping for breaks. Workers can load the materials onto the belt, and the belt does the rest. This saves a lot of time compared to using trucks  or other methods. Additionally, conveyor belts reduce the need for many workers to carry heavy loads. This means fewer injuries and a safer work environment for  everyone. Another benefit is that conveyor belts can carry materials over long distances and tricky terrains. They can go up hills, around corners, and even across water. This flexibility is very useful  in mining where the landscape is often not flat. Conveyor belts are also designed to be strong and durable,  which means they can last a long time, saving money in the long  run. Regular maintenance helps keep them running smoothly, so they rarely break down. Plus, conveyor belts are often more cost-effective than other methods.  They require less fuel and fewer machines to operate,  which can  lower overall costs for mining companies. GLOBULE  focuses on  making these conveyor belts with high-quality materials to ensure they work well for a long time. This means businesses can rely on them without worry. For those looking to enhance their operations further, exploring options like the Secondary Packaging System might also be beneficial.
Our Products

What Are the Key Benefits of Mining Conveyor Belts for Bulk Material Handling?

Finding high-quality wholesale mining conveyor belts is important for businesses looking to improve their operations. One  place to start  is by visiting specialized  suppliers who focus on mining equipment. These suppliers often have a wide range of conveyor belts designed for different types of materials and mining conditions. It’s also a good idea to look for companies that have a good reputation, like GLOBULE.  Our company is known for making strong and reliable conveyor belts that  meet the needs of miners. When searching for conveyor belts, customers should consider the  materials used in the belts. Strong materials mean longer-lasting belts that can handle heavy  loads. Also,  checking reviews and feedback from other customers can help in choosing  the right supplier. Many suppliers have  websites where they showcase their products, making it easy to compare options. Sometimes, visiting trade shows or mining expos can provide a  chance to see various conveyor belts in person and talk directly to suppliers. This can help businesses make better decisions.  Lastly, reaching out to suppliers directly for quotes can lead to good  deals and better  pricing, especially for bulk orders. GLOBULE is always ready to help customers find the best conveyor  belt solutions for their mining needs. It's worth noting that integrating systems such as the Mixing Packaging System can also enhance operational efficiency.

When  people buy  mining conveyor belts, they often face some problems. One big issue is choosing the right size. Mining conveyor belts come in many sizes and types. If someone picks  a belt that is  too small or too big, it won't work well. This can cause delays and even accidents. Another problem is wear and tear. Mining is tough on equipment, and conveyor belts are no exception. They can break or wear out quickly if they are not made from  strong materials. Buyers need to find belts that can handle heavy loads and rough conditions.

Frequently Asked Questions

What is the mining conveyor belt designed for?

Our mining conveyor belt is engineered for sanitary, durable material handling in food and pharmaceutical-related mining processes, ensuring contamination control and consistent product flow with hygienic design features.
Yes. We offer tailored belt widths, lengths, speeds, and mounting options to match your plant layout and processing requirements while maintaining FSMA-compliant hygienic standards.
We use corrosion-resistant stainless steel frames and FDA-compliant belt materials selected for durability, cleanability, and compatibility with food and pharmaceutical environments.
Belts feature sloped surfaces, minimal crevices, easy-access guards, and quick-disconnect components to allow thorough washdown and reduce microbial harborage points.
We provide installation guidance, preventative maintenance plans, spare parts, and responsive technical support to maximize uptime and ensure ongoing FSMA compliance.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Mobile
Message
0/1000

Related product categories

Where to Find High-Quality Wholesale Mining Conveyor Belts?

Where to Find High-Quality Wholesale Mining Conveyor Belts?

Another issue is maintenance. Conveyor belts  need regular check-ups to make sure  they  are  working properly. If a belt is not  taken care of, it can break down,  causing lost time and money. Buyers often struggle to find  good  maintenance  services  or training for their workers. Additionally, the cost  can be  a  concern. Some buyers  want a cheap belt,  but sometimes, spending a little more on a quality belt  can save money in the long run. GLOBULE offers a variety of conveyor belts that are both durable and affordable, making it easier  for buyers to find  what they need without breaking the bank. Lastly, buyers might not know how to install the belts  properly. If the installation is wrong,  it can lead to more problems later. Getting help from experts can make a big difference.

What Common Issues Do Buyers Face with Mining Conveyor Belts?

What Common Issues Do Buyers Face with Mining Conveyor Belts?

Another way  conveyor belts improve  efficiency  is by reducing the risk of  injury. When workers don’t  have to carry  heavy loads, there are  fewer chances of accidents. This makes the  workplace safer and can lead  to fewer days  off work  due to  injuries. Conveyor  belts also  operate continuously, meaning they can run for  hours without stopping. This increases  the amount of material that can be moved in a day,  helping  companies  meet their  goals faster.

How Mining Conveyor Belts Improve Efficiency in Material Transport?

How Mining Conveyor Belts Improve Efficiency in Material Transport?

GLOBULE  conveyor belts are designed to  be strong and reliable, so they can handle heavy materials  without breaking. This means that companies can  trust  their equipment  to work well every day.  Additionally, using  conveyor belts can help reduce costs. When materials are moved efficiently,  companies spend less money on labor and fuel. This can lead to greater profits.  Overall,  mining conveyor  belts help  improve  the  way  materials  are  transported, making the whole  process  smoother and more effective.