EN

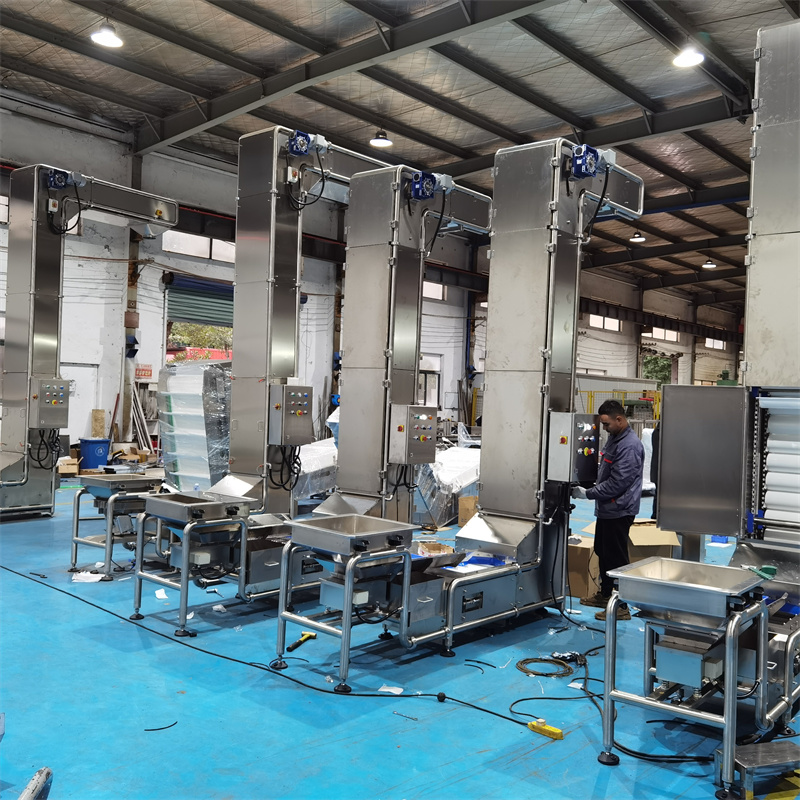
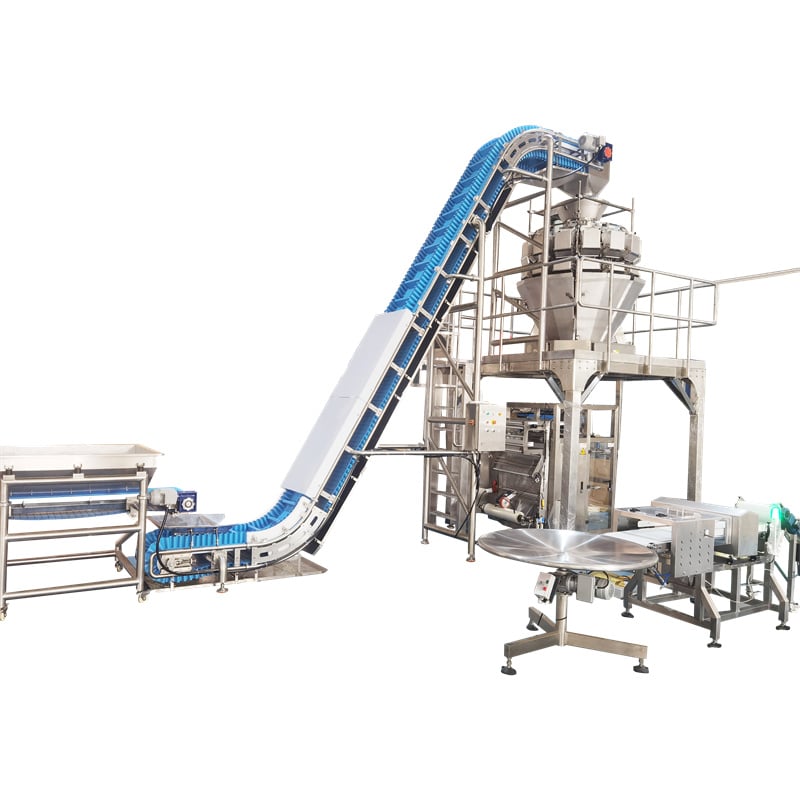
Chain bucket conveyors are machines that help move materials, like grain or coal, from one place to another. They work by using a series of buckets attached to a chain. As the chain moves, the buckets carry the materials along a path, which can be vertical or horizontal. This type of conveyor is very useful in factories, mines, and other places where large amounts of materials need to be transported. At GLOBULE, we focus on creating durable and efficient chain bucket conveyors that meet the needs of our customers.
Chain bucket conveyors have several important benefits when it comes to moving bulk materials. One major advantage is that they can carry materials vertically, which saves space in factories or warehouses. Instead of needing a lot of room to move materials around on the ground, these conveyors can lift buckets up high, allowing for more efficient use of space. For example, if a factory has limited floor area, a chain bucket conveyor can transport items from the ground level to a higher storage area without taking up additional floor space. This is particularly relevant when considering systems like the Secondary Packaging System, which can also benefit from space-efficient designs.