EN

- Overview
- Recommended Products
Overview
Product Position: A Gentle Ramp Where Nuts "Cannot Roll, Cannot Fall, Cannot Break"
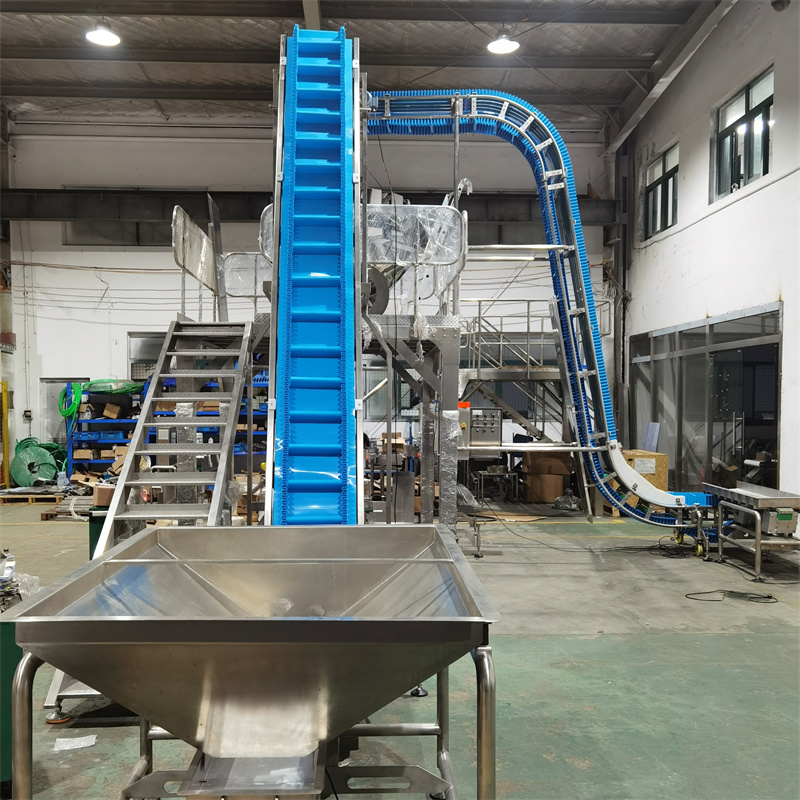
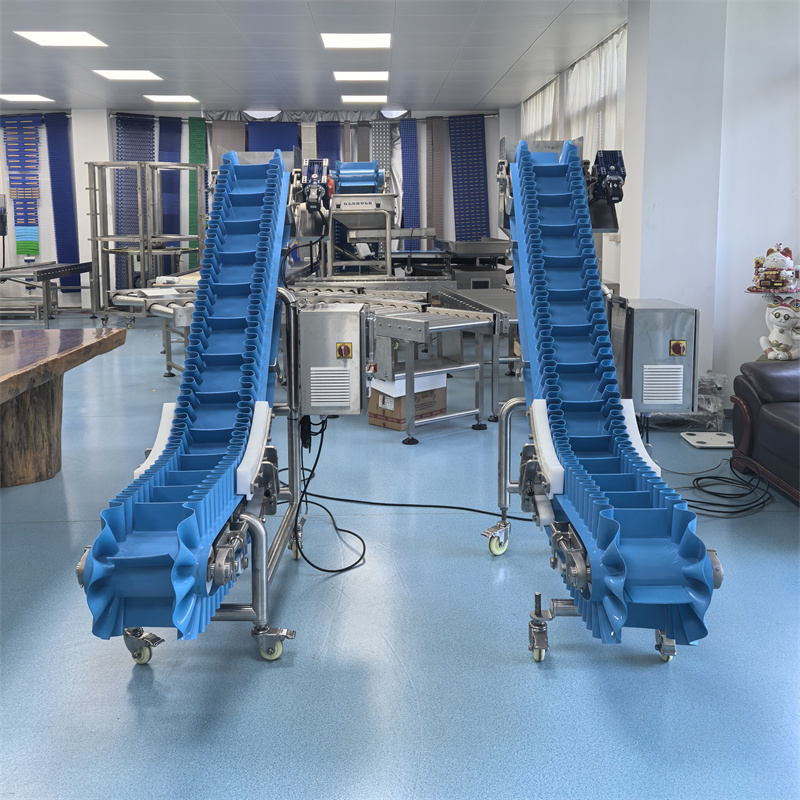
In a nut weighing and packaging system, material must be carried smoothly from a lower elevator outlet, vibratory feeder or buffer hopper to elevated processes such as the multihead weigher or checkweigher-combination machine. Space is limited and elevation differences exist — this is where the inclined conveyor enters the scene. But nuts are not puffed snacks, still less ore. Macadamia nuts are round, natural "rollers"; almond and cashew kernels are flatter yet brittle. The design philosophy of the Globule nut-line inclined conveyor can be summed up in one sentence: small angle, low speed, anti-roll, anti-breakage — high-value nuts climb the incline at a walking pace instead of being hurled along.
The Essential Difference from High-Speed, Steep-Angle Conveyors
On puffed-snack or high-throughput bulk lines, inclined conveyors often chase 60° or even 80° steep angles and high conveying speeds to minimize footprint and maximize output. For nuts, such duty is a disaster: the steeper the angle, the more nuts roll back and pile at the belt's root, squeezing each other; the faster the speed, the harder nuts slide and collide on the belt surface, and shell and kernel breakage risk climbs sharply. The Globule nut inclined conveyor deliberately does the opposite — a gentle slope lets material "lie still" on the belt, and low-speed running lets every nut follow the belt steadily. Nothing rolls back, nothing jolts — the two chronic problems of breakage and pile-up are eliminated at the source.
Engineering Details for Anti-Roll and Anti-Breakage
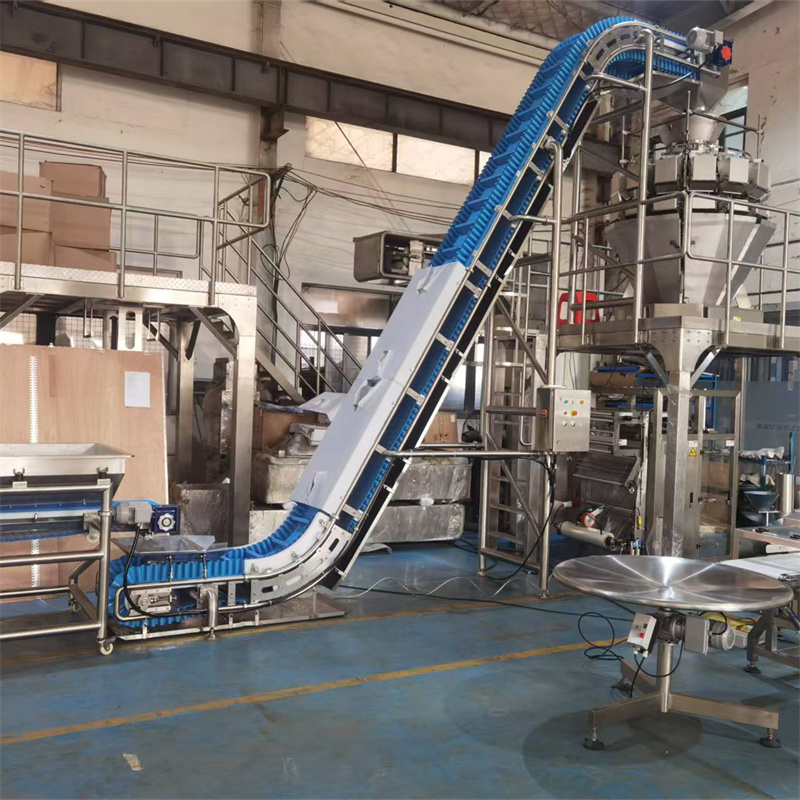
1. Gentle slope design. The incline is set within a flat range based on the angle-of-repose characteristics of nuts and the specific product variety, so even round nuts stay put without rolling back. Both the loading and discharge sections include horizontal transitions, keeping nuts level as they enter and leave the slope and preventing the tumbling caused by sudden "head-up / head-down" changes.
2. Low-speed flexible conveying. Frequency control keeps belt speed in a low range matched to nut appearance requirements. The belt runs smoothly with no pulsation; nuts travel in a uniform single layer, without squeezing or stacking — zero damage to appearance.
3. Food-grade belt with side protection. The belt is made of food-grade materials whose surface texture offers just the right grip — it neither scratches shells nor slips. Low, flexible side guards gently contain the product, preventing nuts from falling off the edge without blocking the operator's view or hindering cleaning.
4. Soft transfer at feed and discharge. Buffer and guide structures at both head and tail drums let nuts move between machines without dropping — they glide smoothly along guide surfaces, matched precisely to the inlets and outlets of the bucket elevator, multihead weigher and checkweigher.
5. Hygienic machine body. The whole conveyor is built of food-grade stainless steel; the belt is easy to remove and the frame easy to wash down, with no sanitary dead spots — meeting the clean-environment requirements of high-value nuts.
Hygiene First · Safety First
Founded in 2019, our engineering team brings more than ten years of food-grade sanitary conveying experience and strictly follows FSMA sanitary design principles. Every part of the inclined conveyor that contacts nuts is made of food-grade materials with smooth, drainable, washable construction, making daily cleaning a simple and reliable routine. Fully guarded moving parts and clear boundary design keep both personnel safety and product safety under control.
Value of System Integration
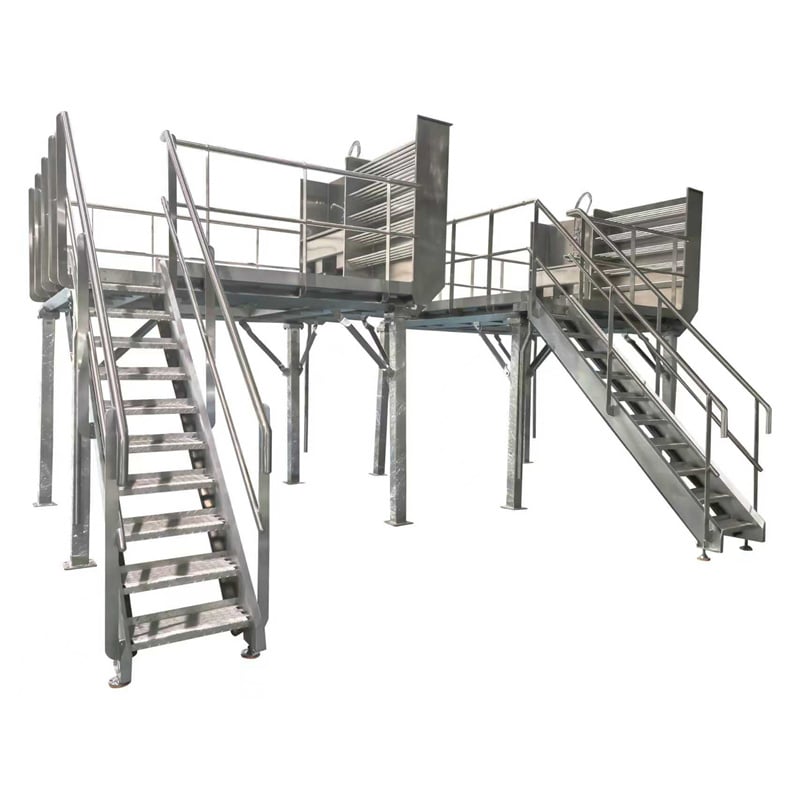
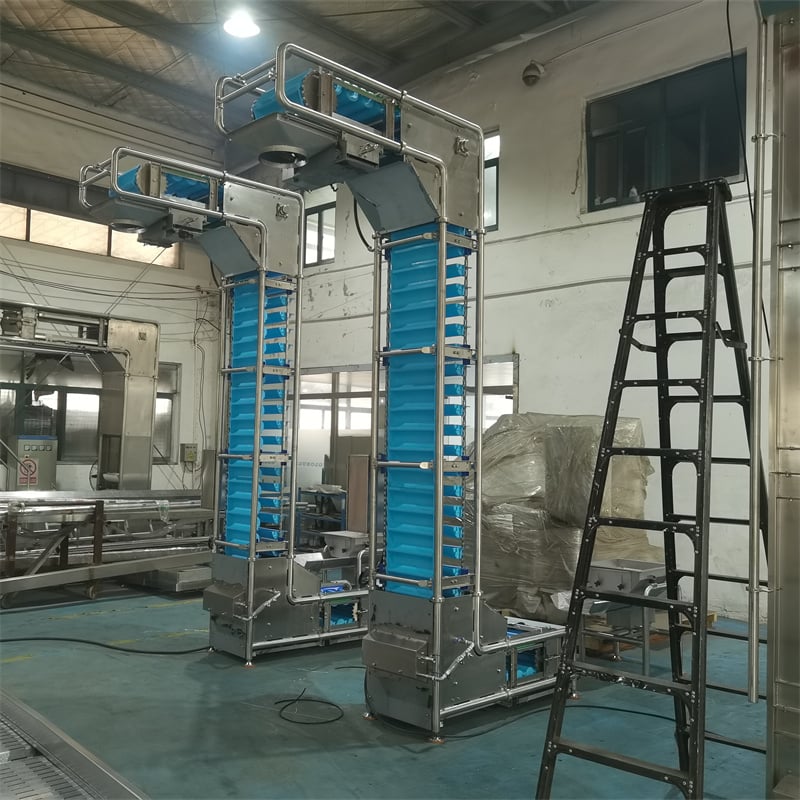
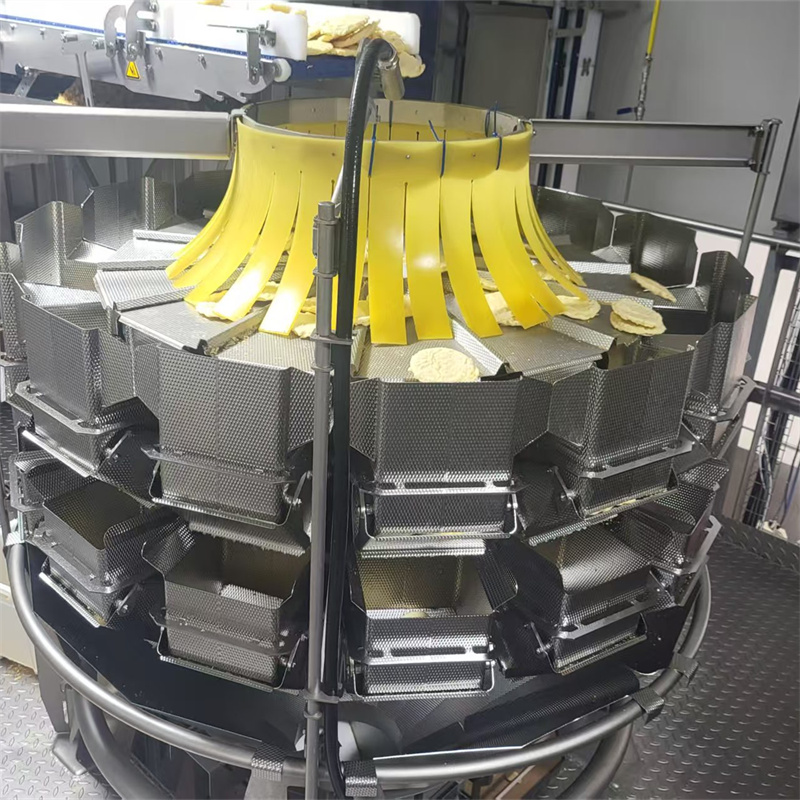
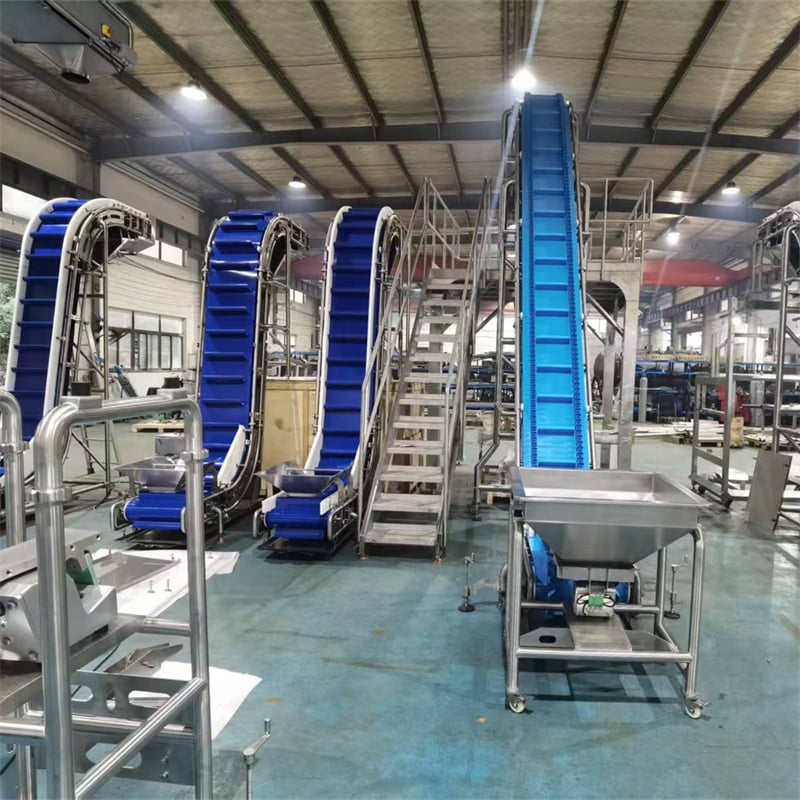
Within the Globule nut weighing and packaging system, the inclined conveyor works with the multihead weigher, stainless steel platform, bucket elevator, vibratory feeder, checkweigher-combination machine and transfer turntables to bridge the height and space gaps between processes. Conveying length, incline angle, belt width and speed are all customizable to your plant layout and product varieties, and can be linked and adjusted with the whole line — ensuring macadamia nuts, almond kernels, cashews and other high-value nuts travel smoothly, at constant speed, with zero damage on every stage of their journey.
Let nuts "walk slowly" and their appearance will "win steadily" — the Globule nut inclined conveyor keeps every high-value nut safe along the way.
Operating and Configuration Notes
Speed linked to the whole line. The conveyor's frequency drive can be wired into the line control so its belt speed follows the upstream feeder and the downstream weigher automatically. When the line pauses for a hopper change or a scale check, the belt stops cleanly without dumping a pile of nuts at the transfer point — no accumulation, no overflow, no wasted product.
Gentle options for every nut shape. Round products such as macadamia rely on the gentle slope and moderate surface grip; flatter products such as almond and cashew kernels can travel at slightly higher speeds within the same low-stress envelope. Where a steeper rise is forced by the building, low-profile soft flights can be added as an option — but even then the speed is kept low and the transition sections horizontal, so the nut never drops freely and never slides backwards against the flights.
Stable tracking and long belt life. Crowned pulleys and a reliable tracking system keep the belt running true, and the low-speed regime reduces wear on both belt and rollers. The result is less maintenance downtime on a machine that, in most plants, runs every production day of the year.
Service and Support
Every conveyor is delivered with installation guidance, a sanitation and maintenance manual, and a stocked spare-parts list covering belts, bearings and drive components. Our engineers commission the machine on site, confirm the speed and angle settings with your product, and stay available as your product range or line layout changes.