Belt Chain Conveyors for Efficient Material Handling

Contact me immediately if you encounter problems!

All Categories

belt chain conveyor

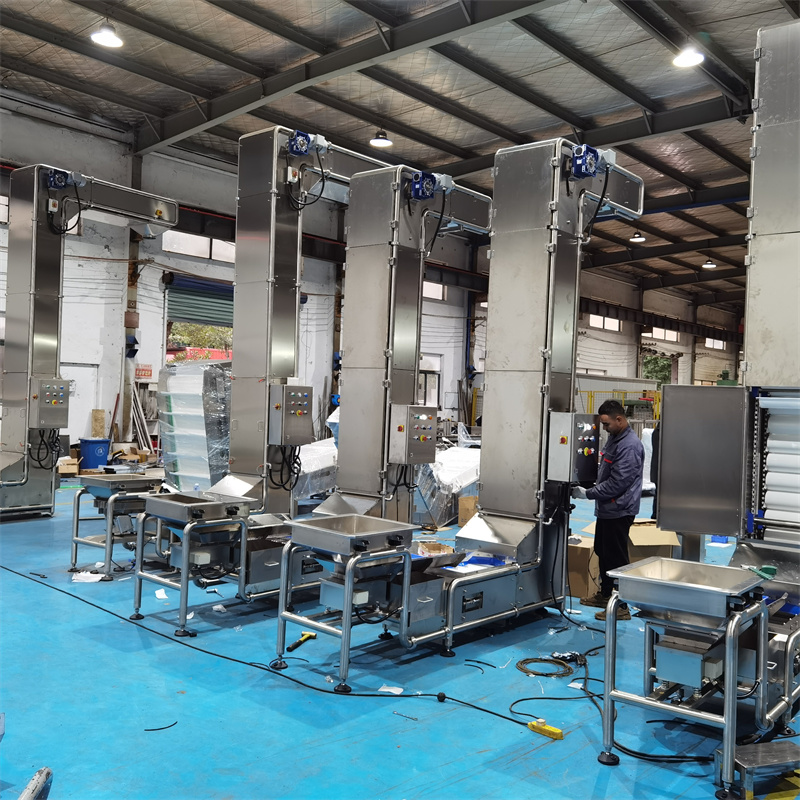
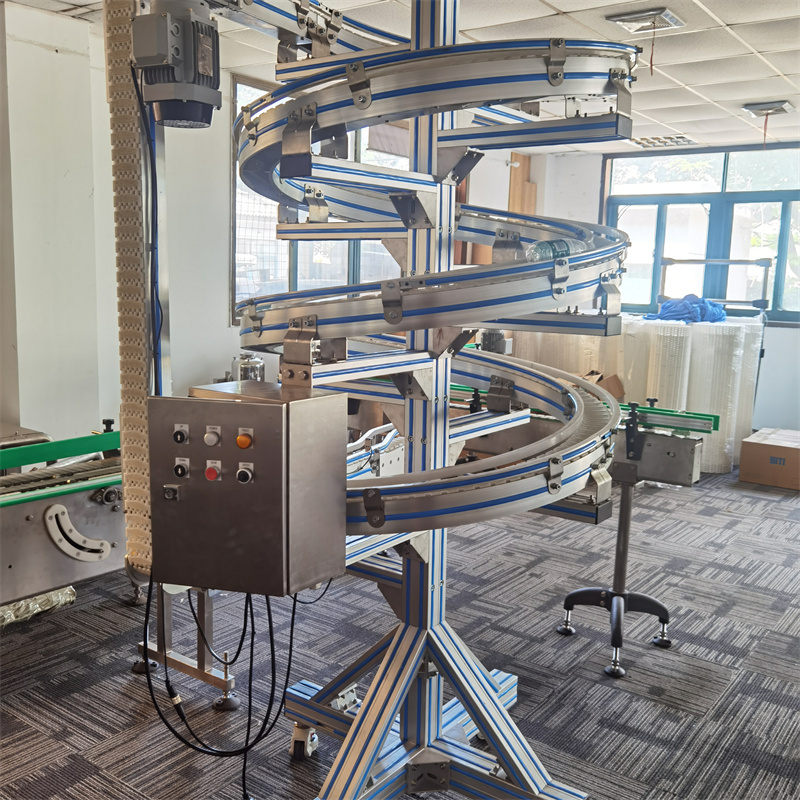
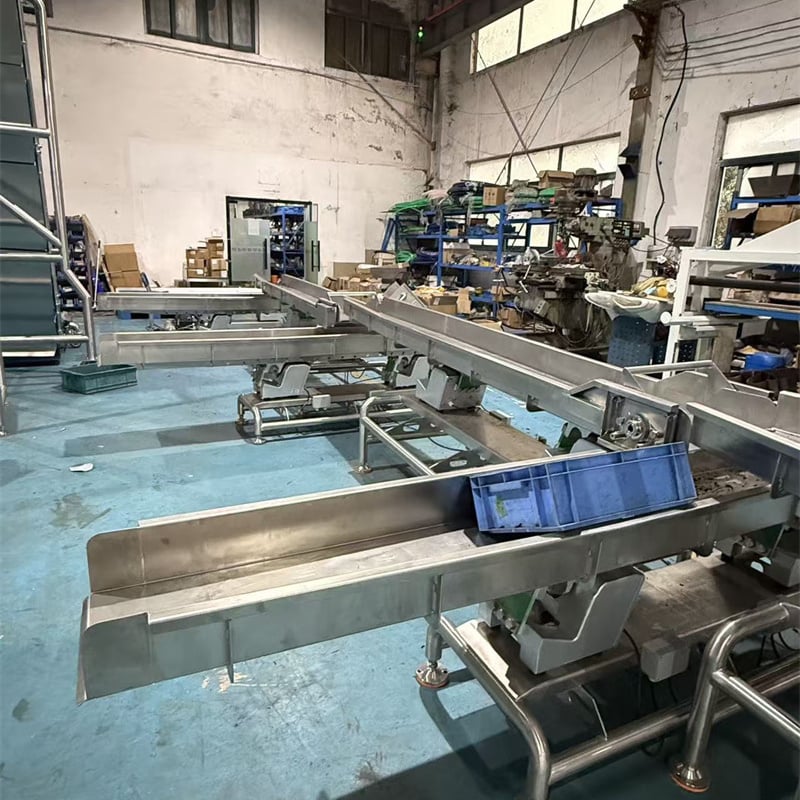
Belt chain  conveyors are  important machines  used in  many industries. They help move items from one place to another quickly and  easily. Imagine a long belt that carries boxes,  bags, or even parts of machines. This belt is connected to  a chain that makes  it  strong and  able to handle heavy loads.  Our  company, GLOBULE, provides high-quality belt chain conveyors that are built to last. They are used  in  factories, warehouses, and many other places where moving  items efficiently is needed. When you think of how busy factories are, you can see  why  these conveyors are  so important. They save  time and energy, allowing workers to  focus on other tasks.
Our Products

What is a Belt Chain Conveyor and How Does it Work?

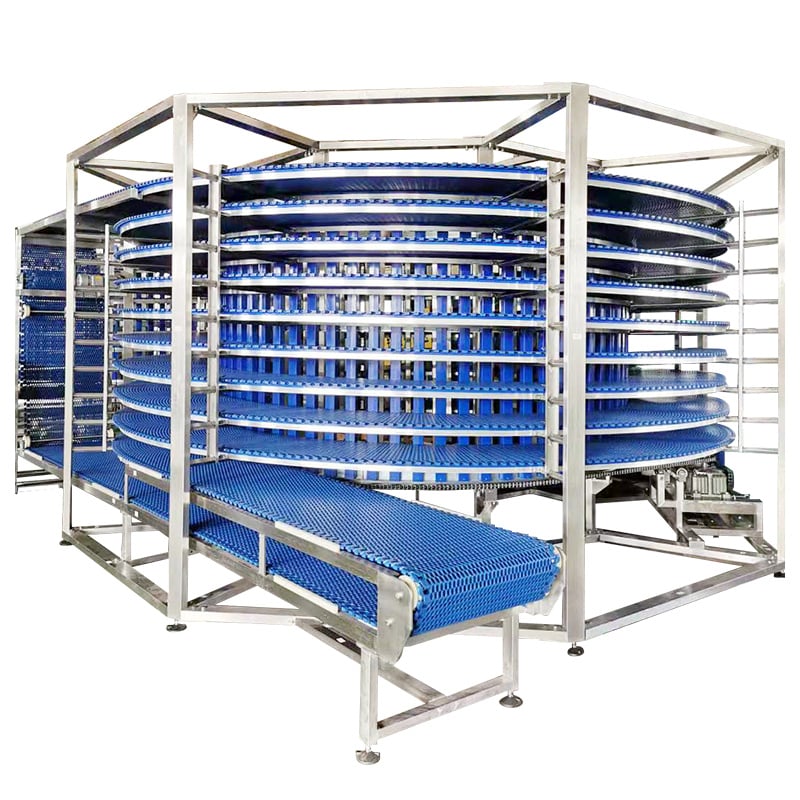
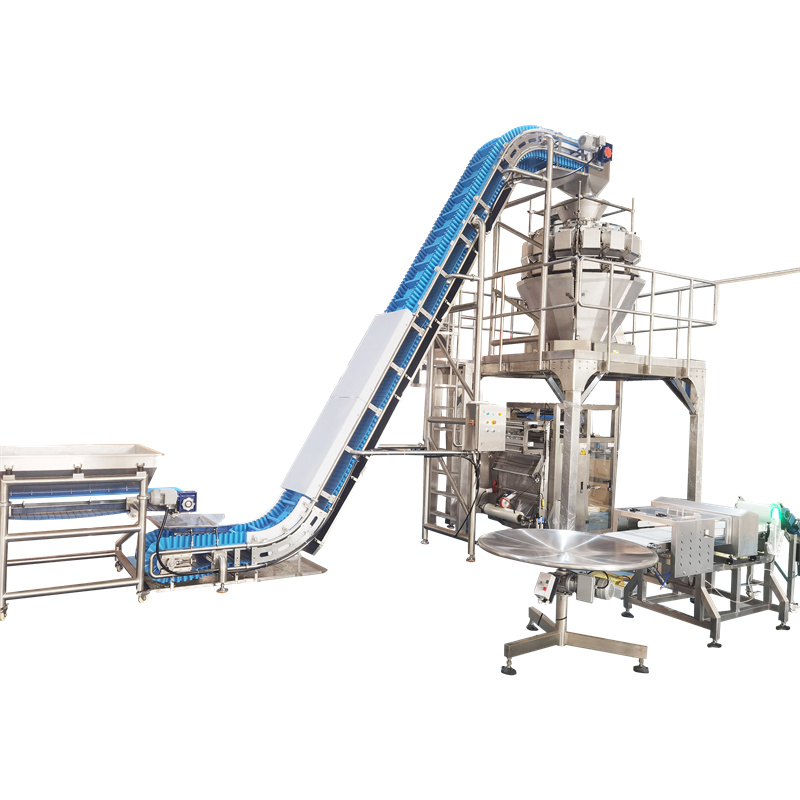
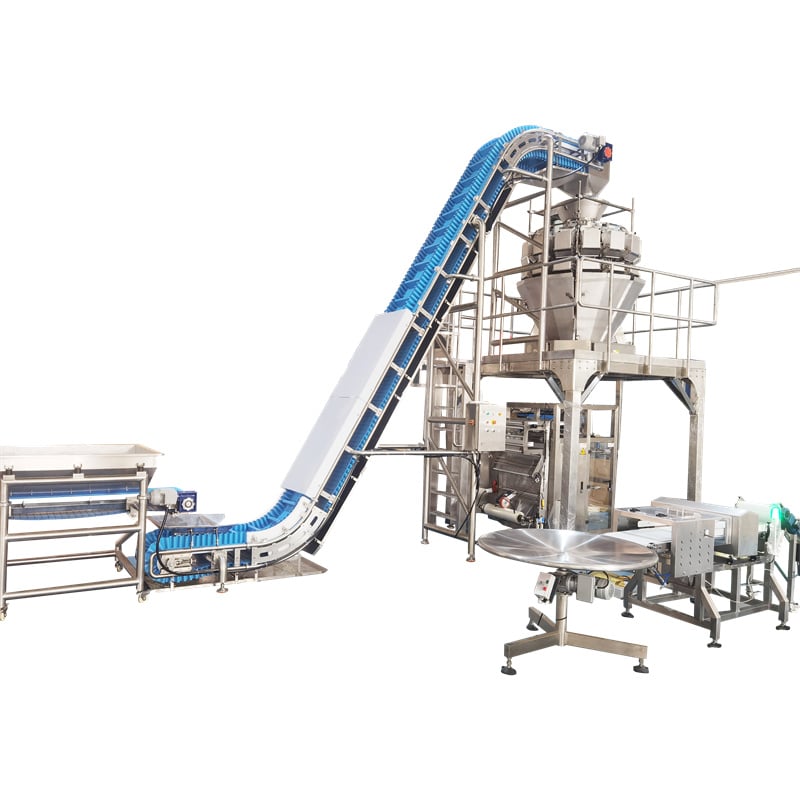
What is a Belt Chain Conveyor and How Does it  Work? A belt chain conveyor is a kind of machine that moves things along a belt. The belt  is made of strong materials that can hold heavy objects. The chain that connects  to the belt helps it move smoothly. When  the conveyor is turned on, the motor makes the chain move, and  this  pulls the belt along with it. For example, in a factory, workers  might place  items on the belt  at  the  beginning. As the belt moves, the items travel down the line to different stations,  where other workers can  pick them up or add more  parts. This system is very helpful because it keeps everything organized and running smoothly. GLOBULE's  belt chain conveyors are designed to be strong and  reliable,  making them perfect for  heavy-duty work. They can be  used to carry many kinds of products, from small pieces to large boxes. Our expertise also extends to the Powder Packaging System, showcasing our versatility in handling various materials.


Frequently Asked Questions

What is the belt chain conveyor used for?

A sanitary transfer system for moving packaged or bulk food and pharmaceutical products on production lines, designed for gentle handling and consistent throughput.
Yes. We use hygienic stainless steel finishes and food-grade materials to minimize contamination and meet FSMA-oriented sanitation practices.
Absolutely. We offer tailored lengths, widths, chain types, and integrations with existing equipment to match product handling, speed, and footprint requirements.
Routine cleaning, chain lubrication if specified, inspection of wear components, and scheduled replacement of sprockets or seals keep performance optimal and compliant.
Yes. We offer installation, start-up assistance, and documentation to support validation, sanitary compliance, and operator training for production use.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Mobile
Message
0/1000

Related product categories

Common Usage Issues with Belt Chain Conveyors and How to Solve Them

Common Usage Issues with Belt Chain Conveyors and How to Solve Them

Common Usage Issues with Belt Chain Conveyors and How to Solve Them  can happen when the conveyor is not working  properly. Sometimes, the belt  might slip or get stuck. This  can slow down  production and frustrate workers. One common problem is when items  fall  off the belt. This can happen if  the belt  is not  set up correctly or if it is damaged. To solve these issues, it’s important  to check the conveyor regularly. Workers should look for  signs of wear and tear on the belt. If the belt is too loose, it can  be tightened.  GLOBULE recommends that workers inspect the machine before starting their shifts. Keeping  the  conveyor clean  and free of debris also helps it run better. If a problem does occur, having  a maintenance team on hand can  help fix it quickly. Training workers on how to use the conveyor  properly can prevent many common problems, ensuring that everything runs smoothly. Moreover, implementing a Nuts Packaging Weighing System can enhance the efficiency of the entire process.
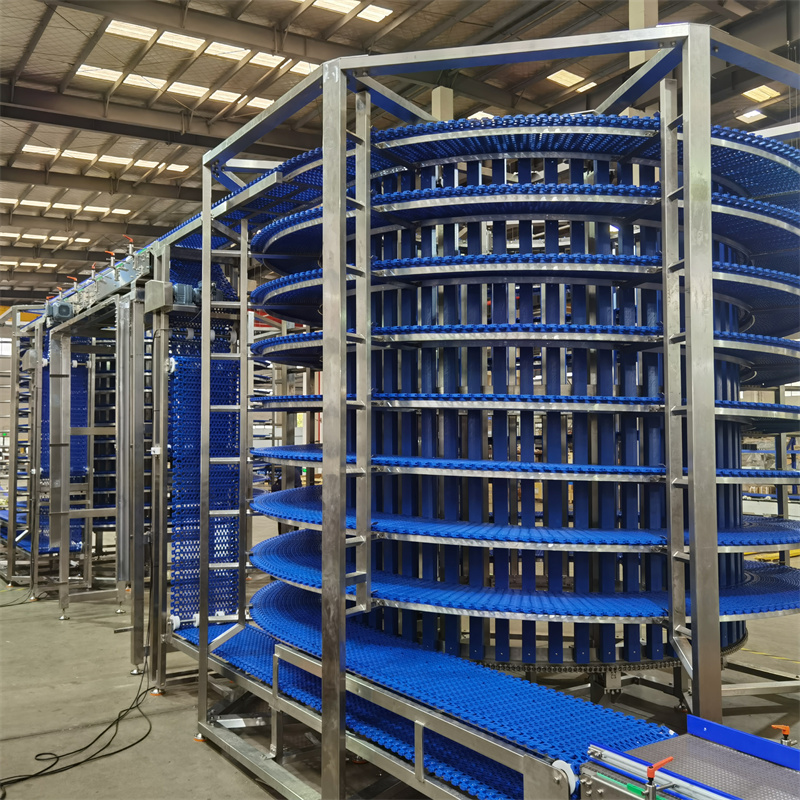
What Makes Belt Chain Conveyors Essential for Efficient Material Handling?

What Makes Belt Chain Conveyors Essential for Efficient Material Handling?

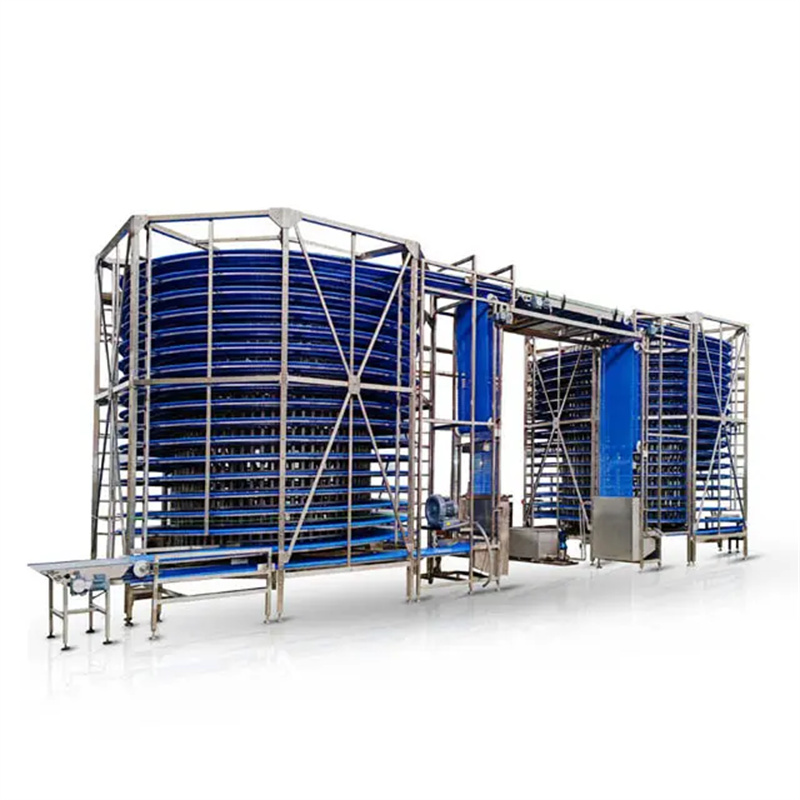
Belt  chain conveyors are very important for moving  materials in factories, warehouses, and other places where products need to  be transported. They are made up of a long belt that moves on top  of a series  of rollers or chains. This helps  to carry heavy items from one place to another without having to lift them by hand. Using a belt chain conveyor can save a lot of time and effort. It makes the work easier and faster because workers do not have to carry items themselves. Instead, they can place the items on the conveyor, and the belt will do the rest. This is especially important  in places where many items need to be moved quickly, like in a  busy factory or a large warehouse. When using a  belt chain conveyor, safety is also better.  It reduces the chance of workers getting hurt while  lifting heavy objects. Workers can focus on other tasks while the  conveyor moves the items. This means that  overall productivity increases. In addition, the design of belt  chain conveyors allows  for transporting items over long distances,  even around corners. They  can be  adjusted to different heights and angles, which makes them very flexible. Because of these  benefits, many businesses choose belt chain conveyors to keep their operations running smoothly. At GLOBULE, we understand how important these systems are for efficient material handling and always aim to provide the best solutions  to meet your needs.

How to Optimize Your Operations with Belt Chain Conveyors

How to Optimize Your Operations with Belt Chain Conveyors

To get the most out of your belt  chain conveyors, there are several tips you can follow. First, make sure you choose the right  type of conveyor for your materials.  Different items might need different types of belts or chains. For example, some items might  be too small or too heavy for  certain conveyors. Next,  regular maintenance is very important. Just like  a car needs oil changes, belt chain conveyors need to be checked and cleaned regularly.  This helps to prevent any problems that could slow down the conveyor or make it stop working. If something goes wrong, it can be very costly and time-consuming to fix. Another way to optimize your operations is to train your workers on how to use and  care for the conveyor systems properly. When workers  know how to operate the equipment  safely and efficiently, it can help prevent accidents and make the work go faster. Additionally, consider the layout of your workspace. The conveyor should be placed in a way  that allows for smooth movement of items without any obstacles. Planning the flow of materials can make a big difference in efficiency. Finally,  at GLOBULE, we recommend using technology to monitor the performance of your conveyor.  Smart systems can alert you when something is not  working as it should, allowing you  to fix issues before they become bigger problems. By following these tips, you can ensure  your  belt chain conveyors are  running at their best, saving you time and money in the  long run.