Micro Conveyors: Enhance Efficiency & Productivity

Contact me immediately if you encounter problems!

All Categories

micro conveyor

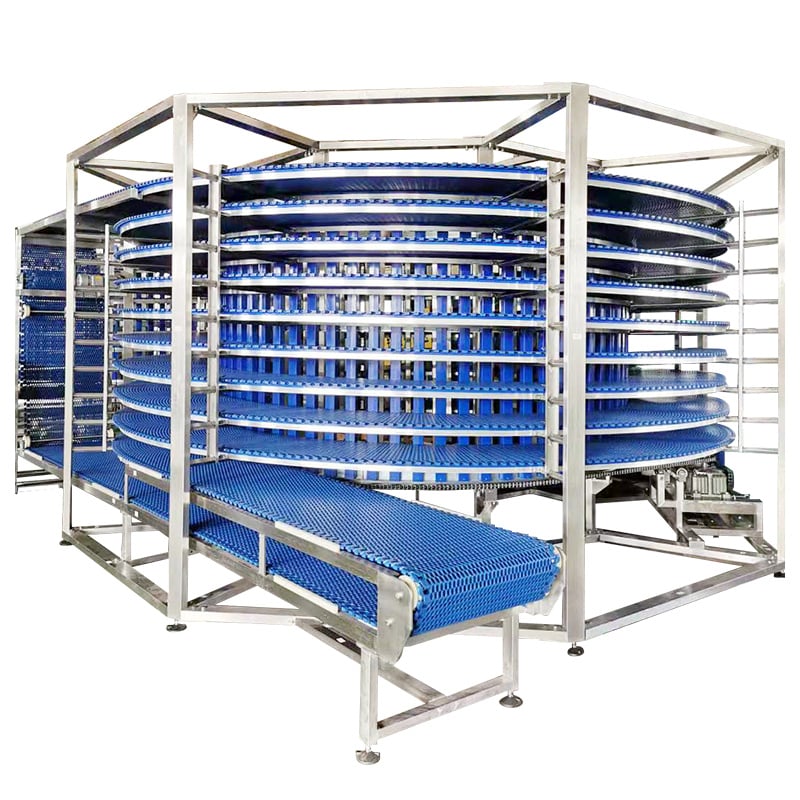
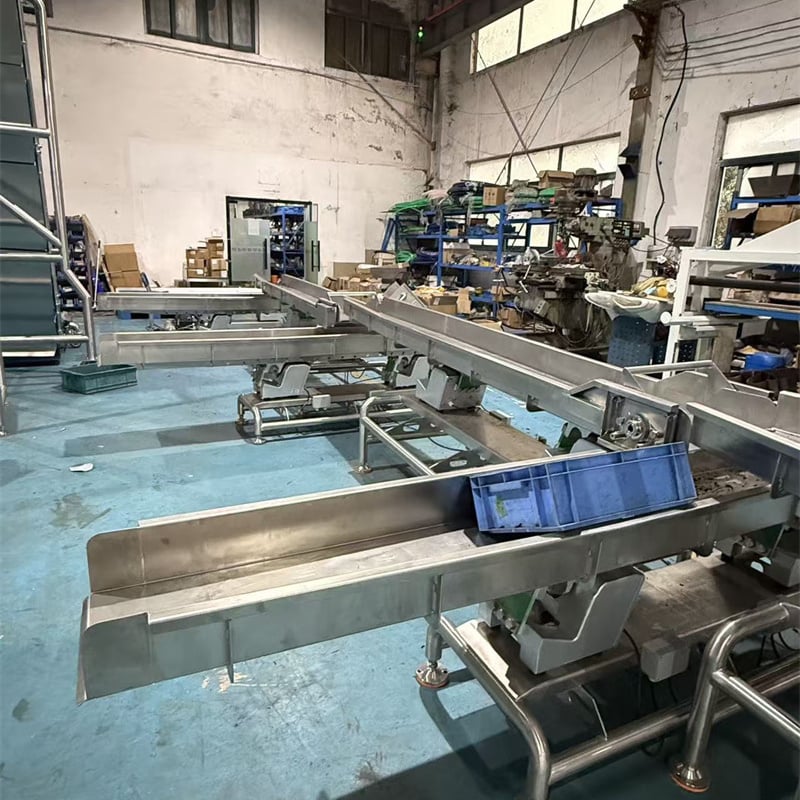
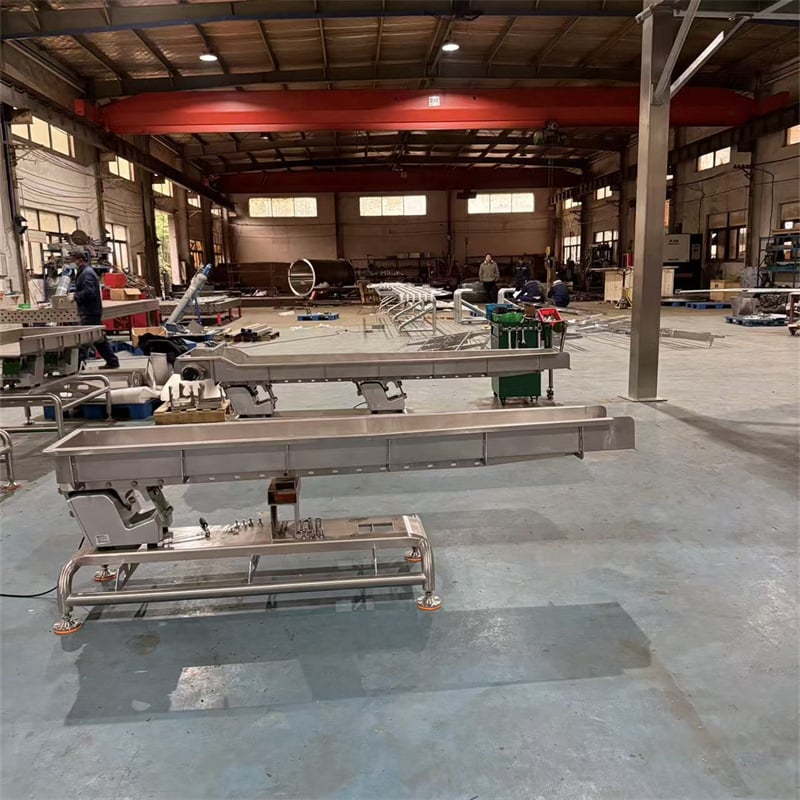
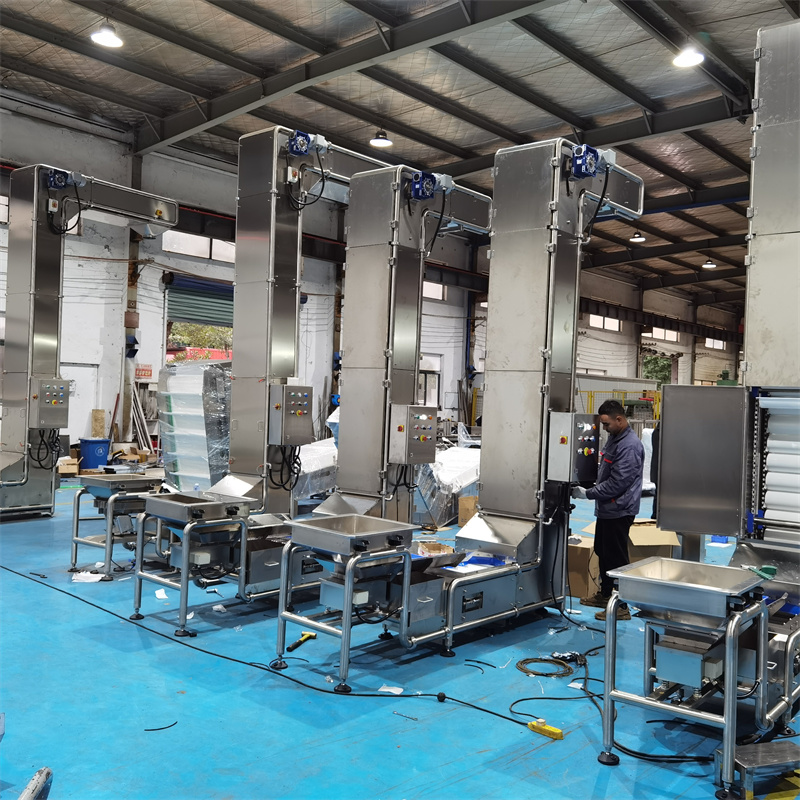
Micro  conveyors are small, moving belts that help transport products and  materials in factories and warehouses.  They play a big role in making work easier  and faster.  At GLOBULE, we know  how  important it is for businesses to keep things running smoothly. These little  conveyors can fit in tight spaces, which  makes them  great for moving  small items  or parts from one place to another. Just think of them as little  helpers that keep everything organized and flowing. They  can be used in  many different  industries, from food  production to electronics. Using micro conveyors can really  help save time  and make work more efficient.
 

Our Products

What Are the Key Benefits of Micro Conveyors for Your Business?

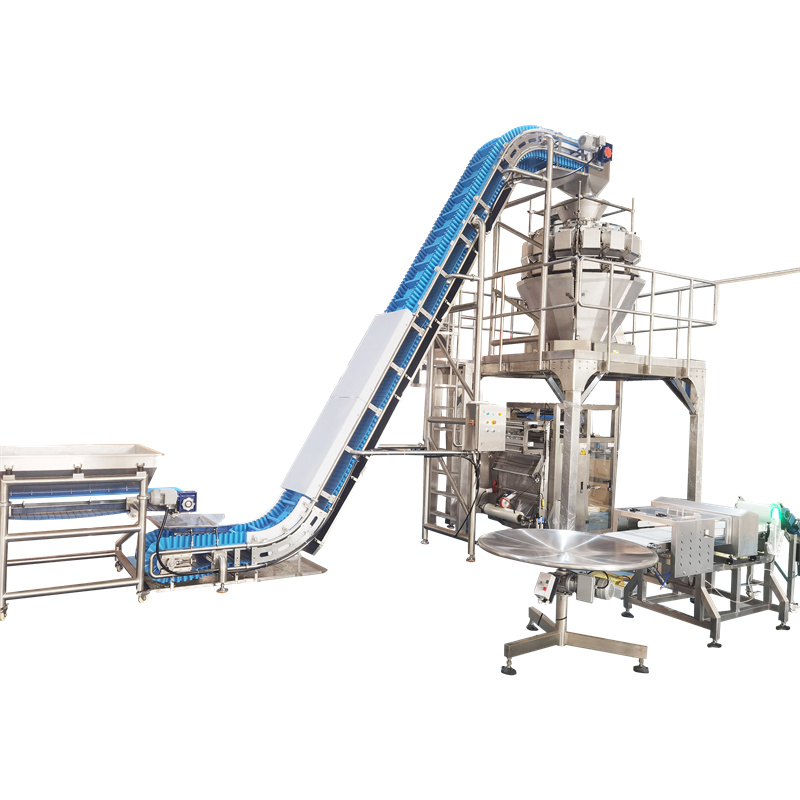
Micro conveyors come with several benefits that can really help your business grow.  First, they  save space. When you have a small area to work with, these conveyors  can fit right in without taking up too much room. This means you can use  that extra space  for other important tasks. Second, they move things quickly and  smoothly. Instead of workers carrying items by hand, micro conveyors can do the heavy lifting. This not  only makes work faster but also keeps workers safe from injuries. For example, in a bakery, a micro  conveyor can carry bread from the oven to the cooling area without anyone needing to touch  it. Another great benefit is that they can be customized. You can change their speed and size to fit what you need. If you have  small parts to move, you can adjust the  conveyor to handle that. Also, micro conveyors can save money. When work is done  faster and safer, your business can save on costs related to accidents, injuries, and time delays. Lastly, they can help  keep things  clean. In industries like food and pharmaceuticals, having a clean  workspace is very important. Micro conveyors can be designed  to be easy to clean,  which  helps maintain a safe working environment. With all these  benefits,  it's easy to see why more businesses are choosing micro conveyors to help with their operations. Additionally, for businesses focused on packaging, a Secondary Packaging System can complement the efficiency of micro conveyors.

Frequently Asked Questions

What is the micro conveyor designed for?

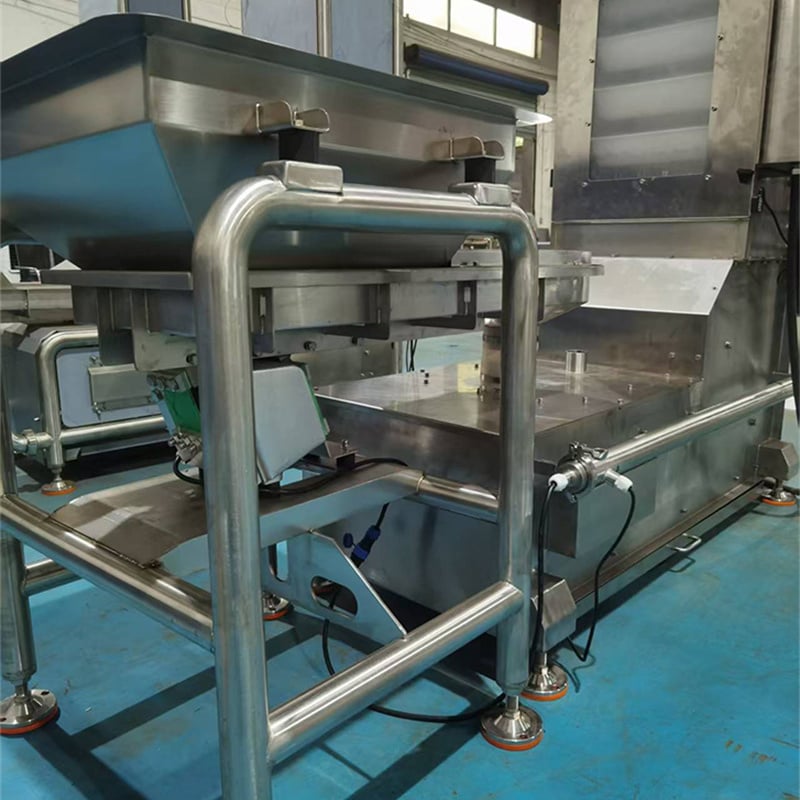
Our micro conveyor is designed for precise, sanitary transfer of small parts and powders in food and pharmaceutical production, supporting gentle handling and contamination control.
Yes. It features hygienic design, smooth surfaces, and selectable materials to meet FSMA and industry sanitary requirements.
Yes. We offer tailored lengths, widths, materials, and fittings to integrate with existing lines and meet specific product handling needs.
Options include stainless steel grades and FDA-compatible polymers chosen for durability, corrosion resistance, and cleanability in hygienic settings.
We provide installation guidance, preventive maintenance plans, spare parts, and responsive service to ensure uptime and sanitary performance.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Mobile
Message
0/1000

Related product categories

How to Choose the Best Micro Conveyor for Your Unique Needs

How to Choose the Best Micro Conveyor for Your Unique Needs

Choosing the  right micro conveyor for your business can seem tricky,  but it doesn’t have to  be. First, think about what you need to move. Are you  moving small parts or heavy packages? Knowing  this  will help you pick the right type. Next, consider  the space you  have  available. If you have  a small area, you'll want a conveyor that fits well without taking up too much room. At GLOBULE, we offer different sizes and designs to suit different  needs.  You also need to think about how fast you want items to move. Some conveyors can go faster than others, so check the speed settings. Another important factor is the material  of the  conveyor. If you're working with food, you’ll want a conveyor that is safe and easy to clean. Lastly,  think about your budget. Micro conveyors come in different price ranges, so it’s important to find  one  that fits within your budget while  still meeting your needs. Don't forget to ask questions and seek advice if you are unsure. At GLOBULE, our team is ready  to help you find the perfect micro conveyor that matches your business needs. Choosing the right conveyor can really make  a difference in how you operate every day.
What Industries Benefit Most from Micro Conveyor Systems?

What Industries Benefit Most from Micro Conveyor Systems?

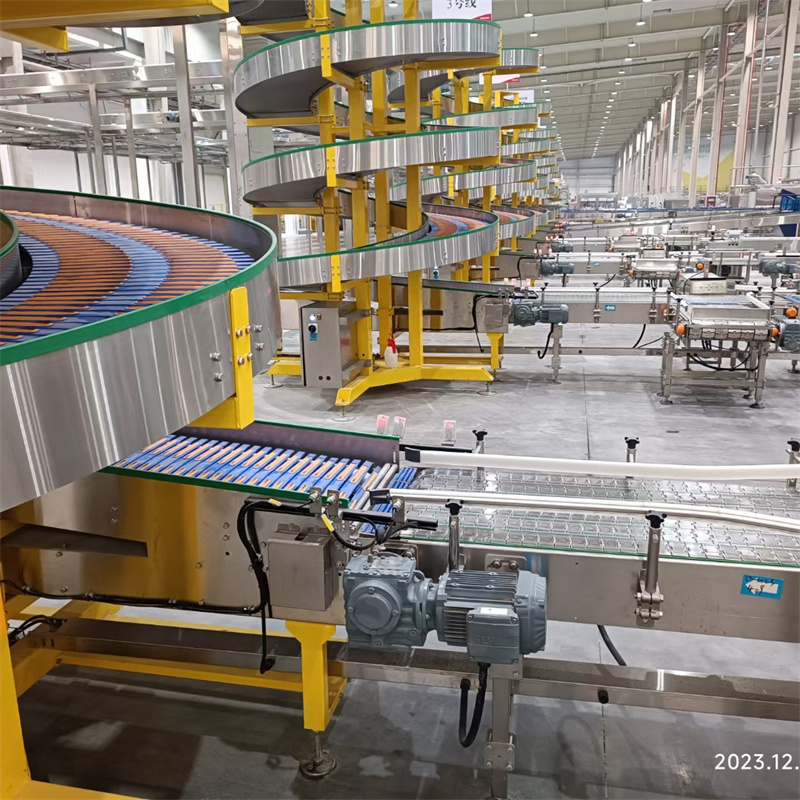
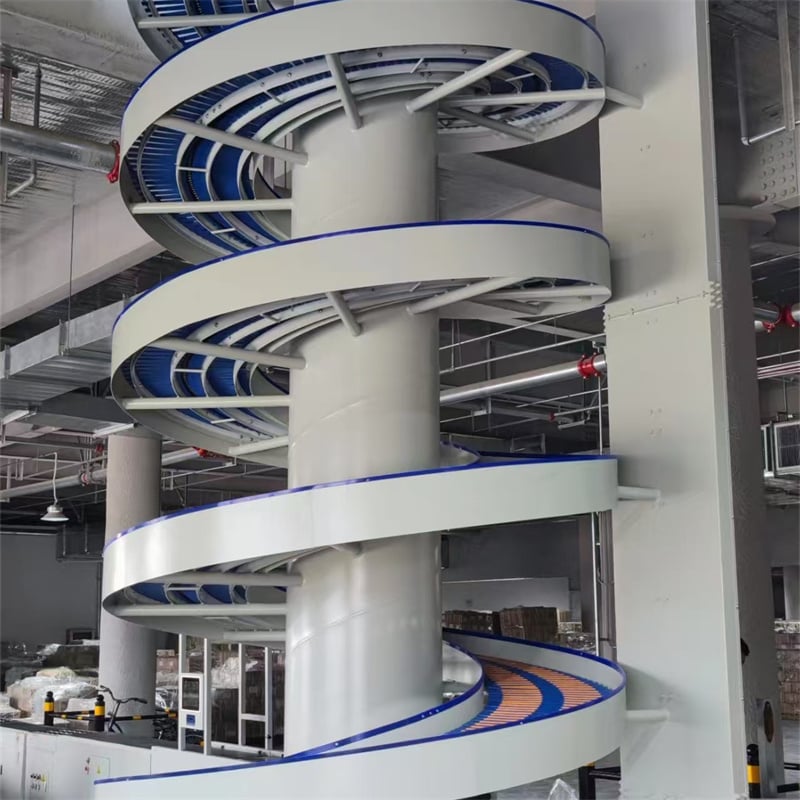
Micro conveyor systems  are small machines that help move  items from one place to another in a factory or warehouse. They are very useful in many industries. Some of the industries that benefit the most from micro conveyor systems include food and beverage, electronics, and packaging. In the food and beverage industry, micro conveyors help move  products like  snacks, drinks, and frozen foods quickly and safely. They keep the food clean and can work  in cold or  hot environments, which is great  for keeping food fresh. In the electronics industry,  micro  conveyors assist in  moving tiny parts like  circuit boards and batteries.  These parts are very small, and micro conveyors can handle them without any damage. This helps factories make electronic  devices faster. Lastly, in the packaging industry, micro conveyors can be used to  move items to be packed. They help sort  and place items in boxes or on shelves efficiently. GLOBULE understands that each industry  has different needs, and that’s why our  micro conveyor systems are designed to be flexible and  easy to use. For example, a Mixing Packaging System can be integrated with micro conveyors to enhance packaging efficiency. We make sure the conveyors can  handle various products, big or small. This adaptability is what  makes micro conveyors so important in many different types of factories.

How Micro Conveyors Improve Efficiency in Manufacturing Processes

How Micro Conveyors Improve Efficiency in Manufacturing Processes

Micro  conveyors also improve efficiency in  manufacturing processes. When factories use micro conveyors, they can save time and reduce  waste. For  example, instead of workers carrying items manually, the micro conveyor  can transport products automatically. This means workers  can focus on more important tasks instead of moving items back and  forth. Additionally, micro conveyors can work continuously without needing breaks,  which helps keep production moving smoothly. They can be made to fit in tight spaces, so  factories  can use every inch of their workspace. GLOBULE micro conveyors are designed  to be reliable and easy to maintain, which means less downtime for  repairs. This helps factories run more smoothly and saves money in the long run. Moreover, with advanced  technology, our micro conveyors can be controlled easily. This  allows factories to  adjust the speed and direction of the conveyor as  needed. This flexibility means that manufacturers can respond quickly to changes in demand and can keep  their production lines flowing without interruption. By using  GLOBULE micro  conveyors,  companies can increase their output and improve the quality of their products.