EN

- Overview
- Recommended Products
Overview
1. Overview
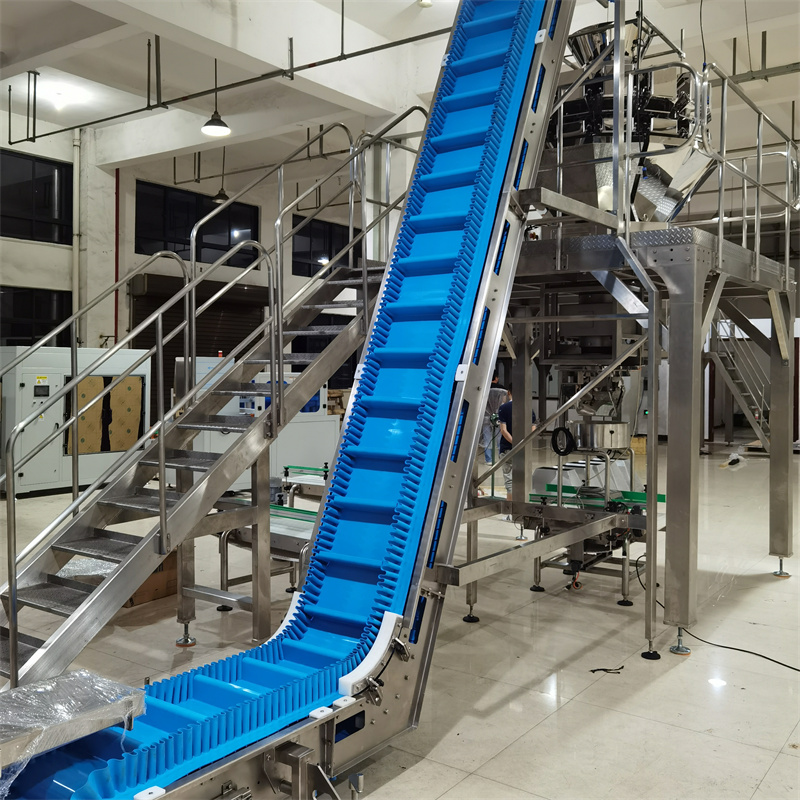
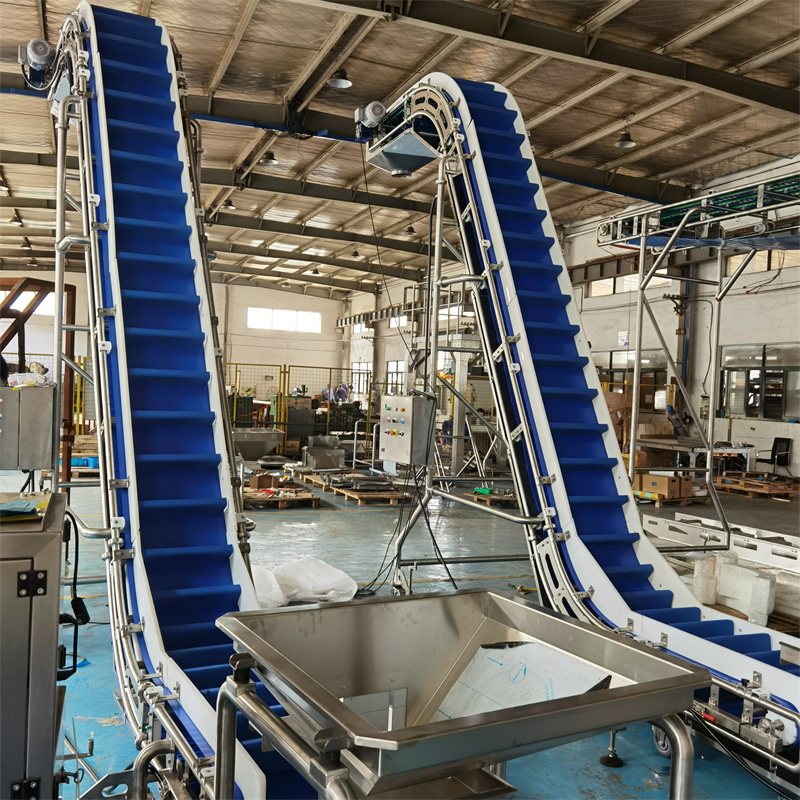
The inclined conveyor is the vertical logistics artery of the mixing and packaging system. It lifts the completed mixed product from the mixing work cell up to the infeed of the packaging machine. In the Globule mixing scene, this conveyor has a mission that sets it apart: what it carries is not a single ingredient but a "mixed-state material" — several kinds of nuts and dried fruit already blended to the recipe ratio. The design focus is therefore not simply "moving material upward", but preserving mix uniformity and preventing segregation for the whole climb, so that the proportioning accuracy built by the front-end linear scales reaches the packaging machine without a gram of drift.
2. Differentiated Role in the Mixing Scene
Within the Globule product family, conveyors with the same name perform very different jobs in different systems: puffed-food lines demand high-speed handling of a single product, and nut lines demand low-speed handling to avoid breakage. The inclined conveyor of the mixing and packaging system focuses on three challenges that are unique to mixed materials:
Preserving mix uniformity
● : after blending, heavy nuts and light dried fruit can easily re-segregate under the vibration of an incline. Globule controls belt speed, layer thickness and gentle material guidance so the blend keeps an even cross-section through the whole journey.
Preventing segregation and roll-back
● : on steep inclines, round nuts tend to roll downward while flaky dried fruit lags behind. The equipment uses a matched incline angle and retaining structure with a low material bed so every particle shape climbs steadily together.
One unified climb, one infeed point
● : several upstream streams merge into one flow, lifted by a single conveyor into the elevated hopper of the packaging machine — simplifying plant space and giving the packaging machine one stable, continuous feed.
3. Structure and Composition
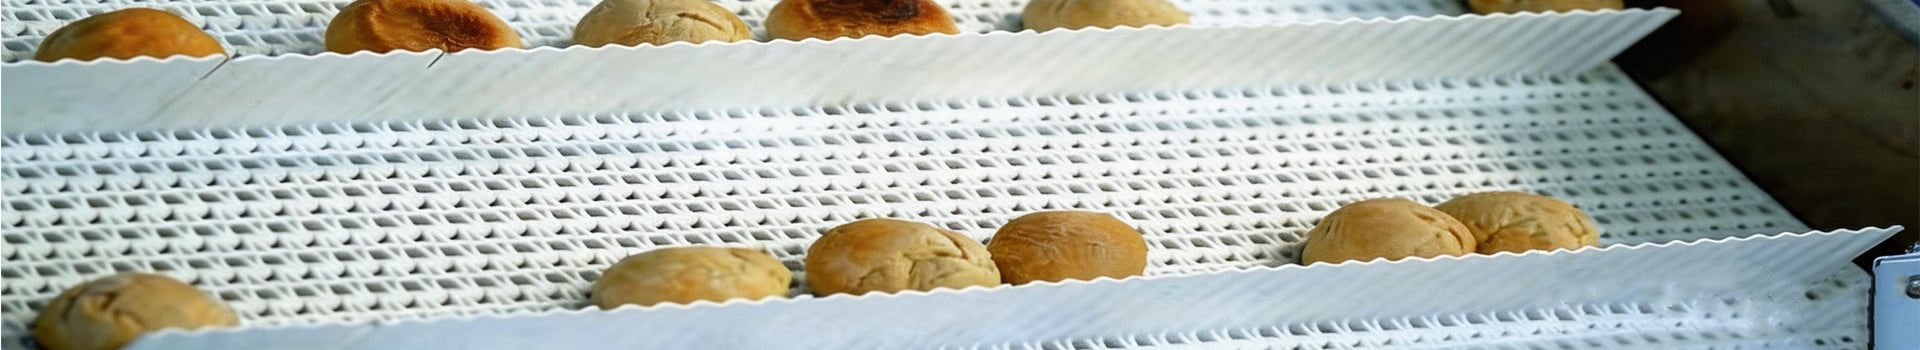
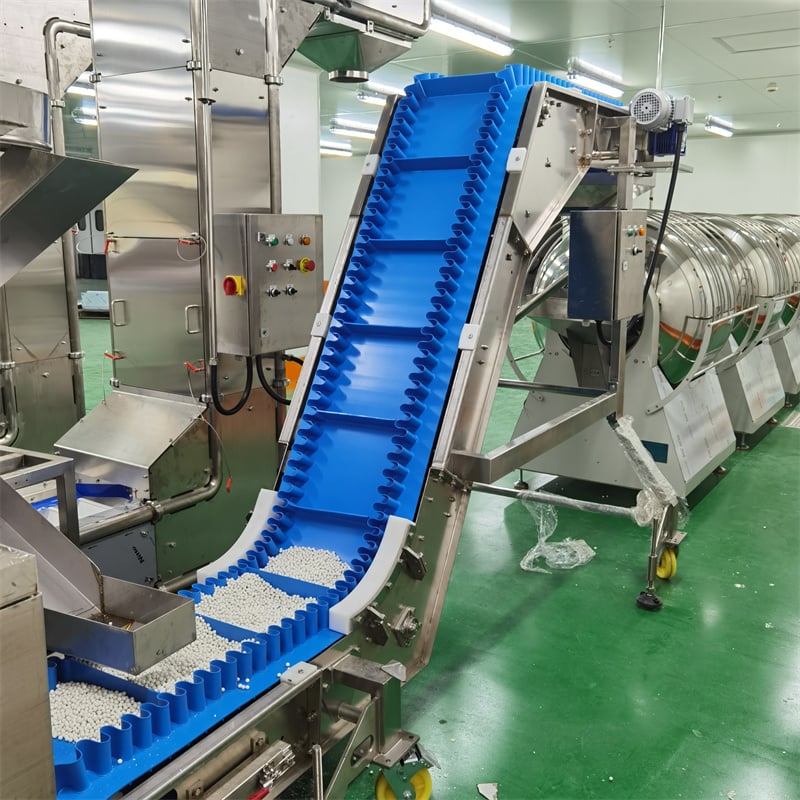
Globule inclined conveyors use a food-grade stainless steel frame and are available with a flat belt plus low cleats, a modular flighted belt, or a bucket format to suit different particle shapes and drop heights. The machine comprises the stainless frame with adjustable legs, a drive unit with geared motor and guard, a tensioning device, belt-run tracking protection, a return-side scraper, infeed and discharge transition troughs, and optional vibrators and level sensors. The incline angle, belt speed and lift height are all engineered to the site — typical angles are between 30° and 45°.
4. Key Features
Mix-dedicated conveying profile
● : belt speed, angle and bed depth are co-designed so the blend moves up the incline as a whole body rather than rolling against itself, suppressing density-based segregation at the mechanism level.
Gentle infeed and cushioning
● : a buffered transition at the infeed prevents the mix from slamming down off the collecting belt, which would cause impact segregation and nut breakage.
Low product-bed design
● : the bed height is controlled so bottom material is not pinned down by the layers above, while top material cannot roll back — large and small particles climb in step.
Unified lift and centralised feed
● : one conveyor merges multiple incoming streams and feeds the packaging machine's elevated hopper continuously and consistently, with level signals for automatic start and stop.
Return-side self-cleaning
● : return scrapers continuously remove adhered fines, preventing residue build-up in a closed environment and avoiding cross-batch contamination.
VFD line interlocking
● : belt speed links to the front weighing rhythm and the rear packaging speed; on starvation it slows down automatically, on blockage it stops — abrupt conditions never get a chance to destroy mix uniformity.
5. Hygiene and Food-Safety Design
The conveyor contacts food directly and is engineered to FSMA hygienic design principles: product-contact parts are food-grade stainless steel with a food-grade belt (food-grade PVC or modular plastic belt optional); the frame uses continuous rounded welds with no harbourage points; drives and electrical parts are properly protected for washdown environments; infeed and discharge transitions are smooth with no ledges that trap product; and scrapers plus catch structures keep residue under control. The open construction supports quick end-of-shift inspection and cleaning.
6. Line Synergy
In the mixing and packaging system the inclined conveyor is the relay between the linear scales and the packaging machine: it receives the blended material from the collecting conveyor, lifts it to the height the packaging machine needs, and feeds it steadily at a rate matched to the packing rhythm. Its level signals are shared across the line, creating a seamless "weigh → merge → climb → pack" sequence in which every pause in one link is sensed and answered by the whole line.
7. Target Scenarios
The conveyor fits every mixing-packing line that must elevate a blended product to a high infeed: mixed nuts, mixed dried fruit, multi-flavour snack pouches and multi-grain cereal before packaging, as well as layouts where the plant has a level difference and the packaging machine's infeed sits above the mixing cell.
8. Reference Technical Parameters (configurable per project)
| Item | Reference value |
| Conveying format | Flat belt with low cleats / modular flighted belt / bucket (selected by material) |
| Incline angle | Typically 30°–45°, engineered per site |
| Lift height | Per packaging machine infeed height |
| Belt speed | VFD-controlled, interlocked with upstream/downstream rhythm |
| Frame material | Food-grade stainless steel 304 (316 optional) |
| Belt | Food-grade PVC / modular belt, optional |
| Cleaning accessories | Return scraper, buffered infeed/discharge troughs, optional vibrators |
9. About Globule
Globule Sanitary Conveyor Pty Ltd (Shanghai Lingan Equipment Manufacturing Co., Ltd.) was founded in 2019. Its core engineering team has more than 10 years of experience in food conveying and packaging equipment, and it upholds the design philosophy of "Hygiene First · Safety First". Our products follow FSMA hygienic design guidelines and deliver integrated mixing, proportioning, conveying and packaging solutions.
10. Selection and Service
Send us your blended composition, particle shapes, capacity and site level difference. Globule will complete the angle, speed and belt-width selection and support on-site verification of the anti-segregation conveying solution.