EN

- Overview
- Recommended Products
Overview
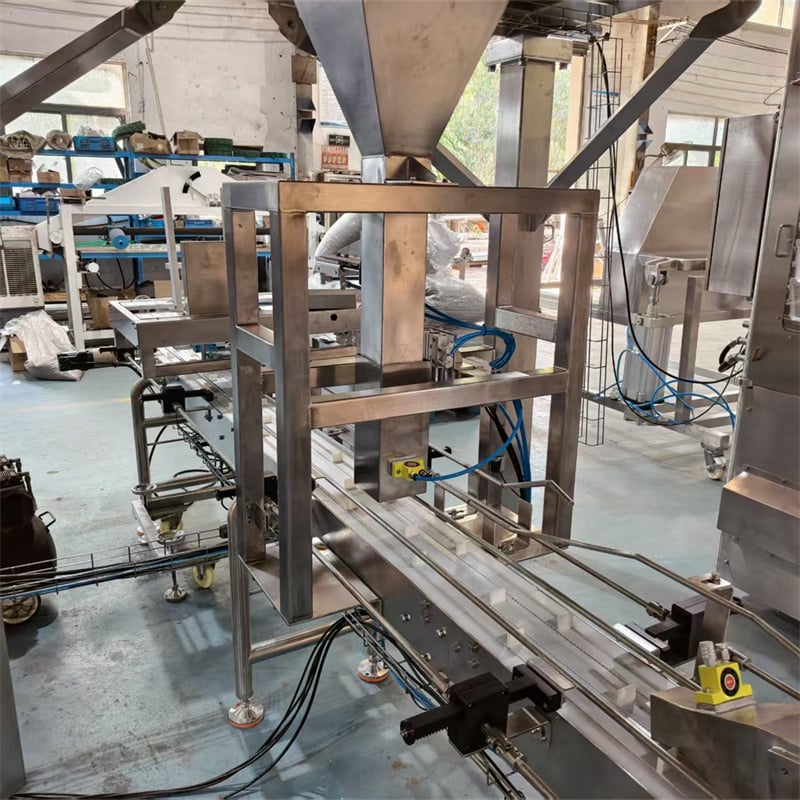
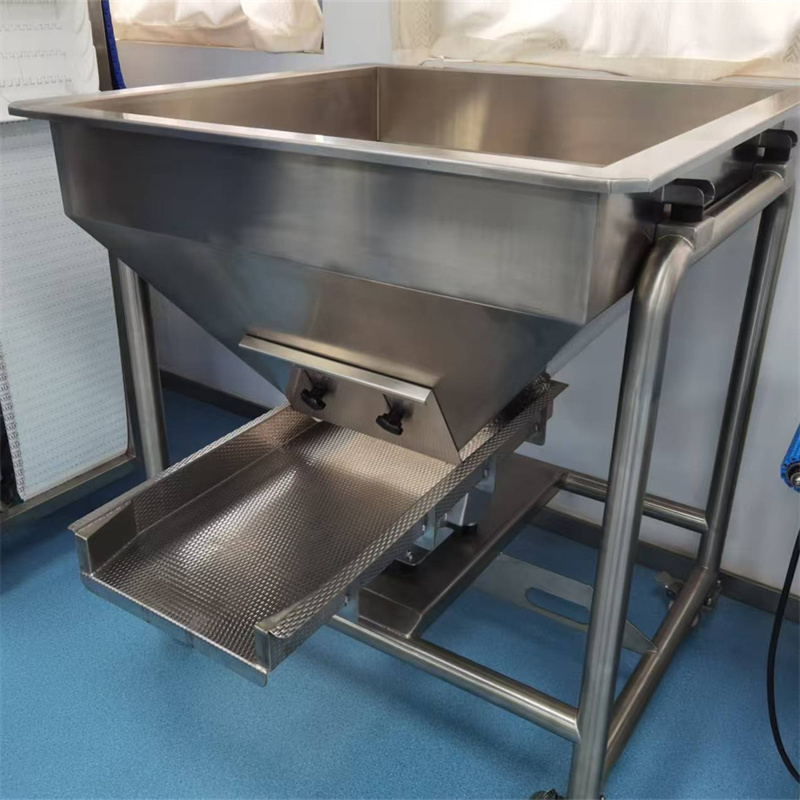
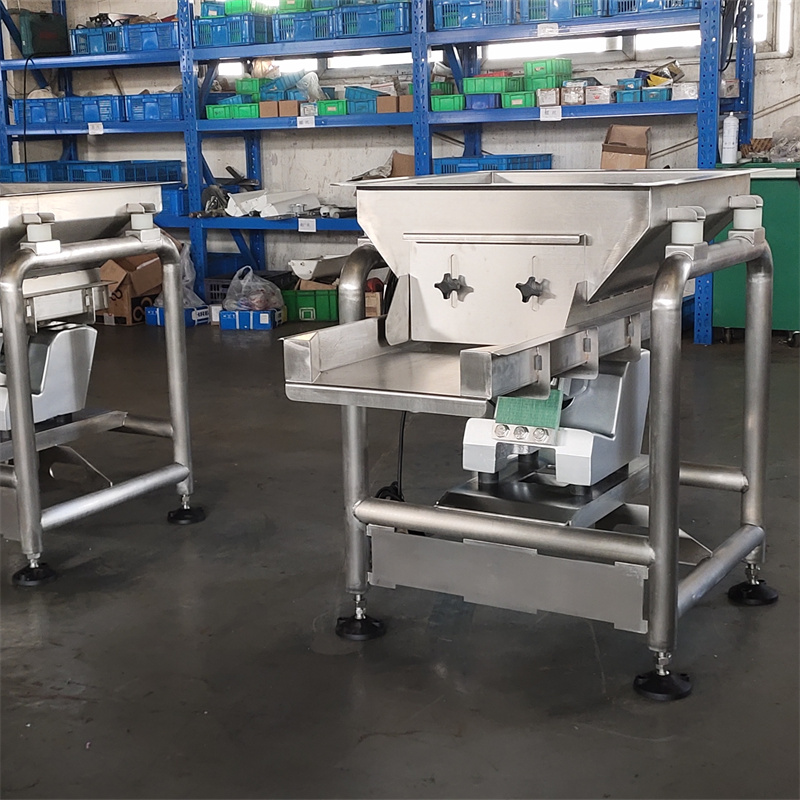
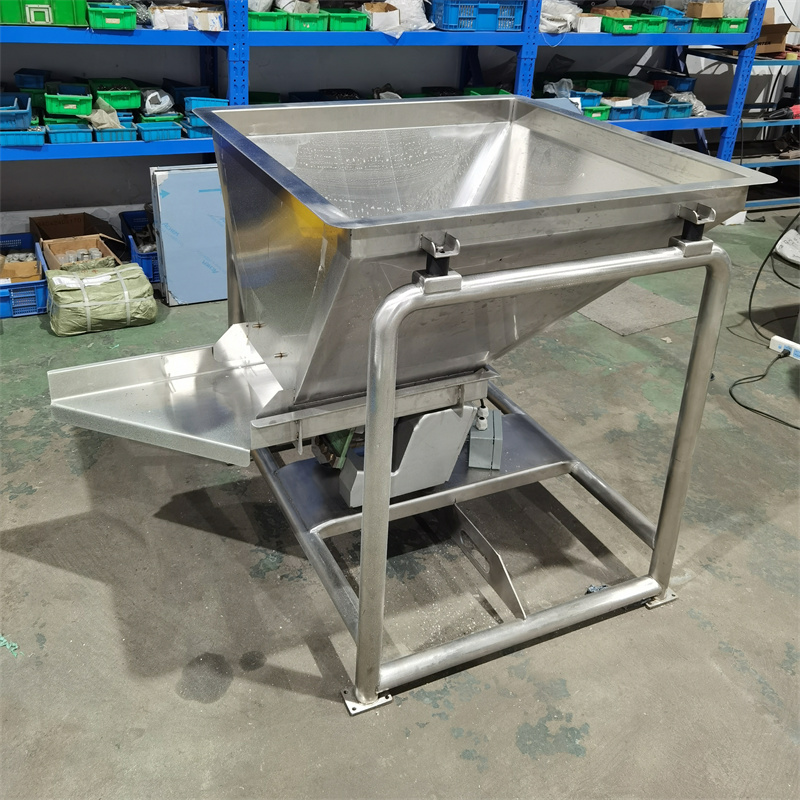
The Vibrate Feeder is the key feeding machine that links elevating with weighing in the nut weighing and packaging system, positioned between the bucket elevator and the multihead weigher. Its task is not speed but uniformity and steadiness: it turns the macadamia, almond kernels, cashews and other nuts delivered from upstream into a stream of even thickness, constant speed and immediate start-stop control, feeding it continuously into the infeed funnel of the multihead weigher.
The stability of the feeding stage directly determines how frequently the multihead weigher can run combination weighing. If the stream surges and dips, the weigher is forced to wait or refill constantly; if product suddenly floods down, the weigh hoppers are overloaded and must be dumped — both throughput and accuracy suffer. The Globule Vibrate Feeder is designed precisely for this stage: an inverter-controlled vibration system spreads the nuts into an even thin layer and discharges it continuously with a constant cross-section, keeping the downstream multihead weigher always full and always even.
At the same time, nuts are high-value and fragile. Macadamia with brittle shells cannot withstand aggressive tumbling, and almond kernels readily break or release oil under mutual compression. This machine runs at low frequency and small amplitude so that nuts maintain an ideal "micro-tossing, continuous sliding" motion inside the trough — moving forward only, without tumbling, jumping off the trough surface or stacking. Product integrity is protected from the feeding stage onward, ahead of weighing and packing.
Core Functions and Design Advantages
1. Uniform Feeding — The First Guarantee of Weighing Accuracy
Vibration frequency and amplitude are finely adjustable, and the machine spreads nuts into an even thin layer for continuous discharge, eliminating pulsing and uneven dosing. For irregular, long and flat, easily overlapping products such as macadamia and pecans, constant-flow output is the precondition for stable combination hits — only when bed depth is consistent is the product distribution in every weighing cycle consistent, and only then does combination efficiency mean anything.
2. Closed-Loop Constant-Flow Control — As Much As Needed, No More
The feeder is interlocked with the multihead weigher’s hopper-level signal to form a feed-and-weigh closed loop: output rises immediately when the level is low and narrows as soon as the level is reached, with millisecond-level response. Transient differences between upstream supply and downstream take-up are absorbed automatically by the feeder, so the weigher neither idles waiting for refill nor dumps overloaded hoppers after a sudden flood — single-line capacity is fully exploited.
3. Large Hopper + Anti-Bridging Design — Absorbing Fluctuation, Preventing Flooding
The generous storage volume absorbs short interruptions in upstream supply, so the multihead weigher is never starved during continuous high-speed take-up. To handle the fragments, seasoning powder and irregular shapes mixed into nut products, which tend to arch inside the hopper, the hopper-to-trough transition uses large radii and an anti-bridging structure combined with vibration de-arching. Product discharges smoothly even at high throughput, with no sudden flooding.
4. Low-Frequency Gentle Vibration — Protecting Nut Integrity and Appearance
The value of nuts lies entirely in their appearance. This machine runs at low frequency and small amplitude, so product movement across the trough is mainly translational sliding rather than violent tumbling and mutual collision. With adjustable bed-depth control, nuts do not stack and compress one another. For fragile kernels such as almond and cashew, this directly reduces breakage and oil release, and also prevents shell fragments from contaminating finished products downstream.
5. Vibration-Isolated Supports — No Interference with Multihead Weighing
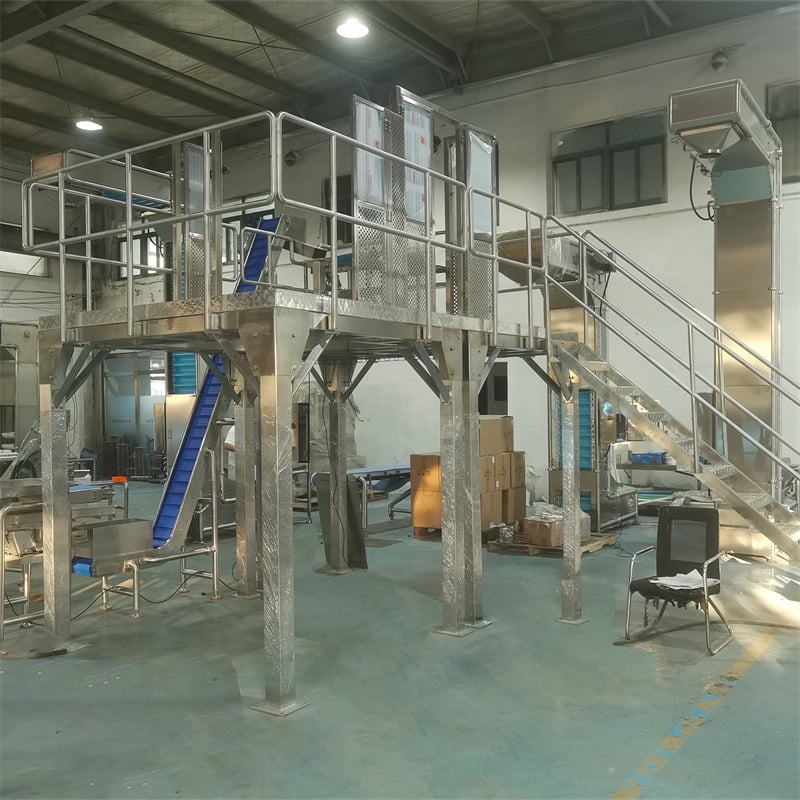
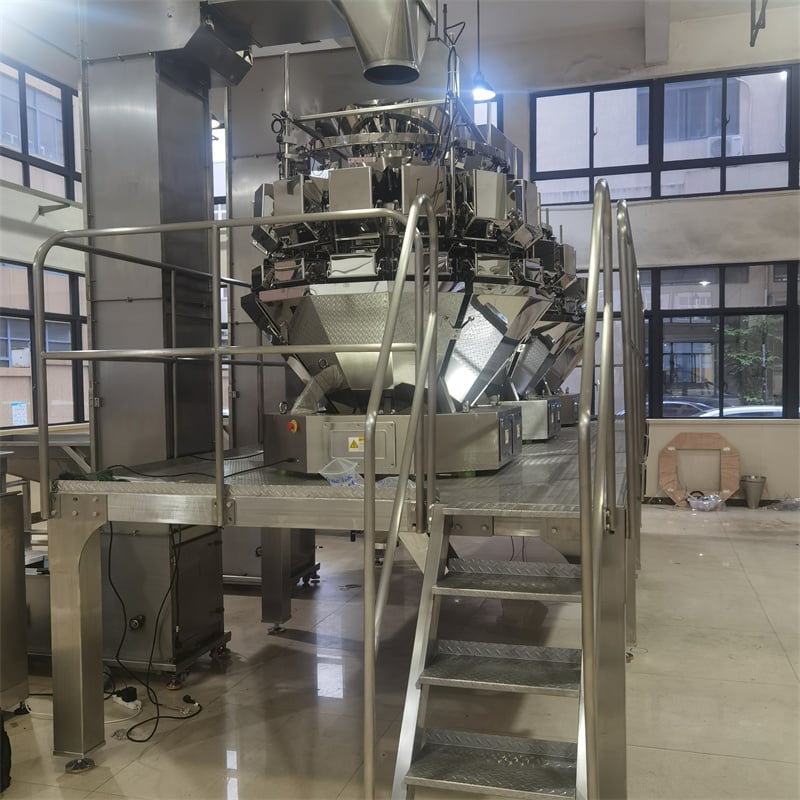
The vibrate feeder and the multihead weigher normally share the same elevated platform. If vibration travels through the frame it directly affects the stability of combination weighing. This machine uses vibration-isolated supports that keep vibration away from the platform and the line, preventing resonance with precision equipment such as the multihead weigher and protecting weighing accuracy at the physical level.
6. All-Stainless, Quick-Release Construction — Built for Nut Dust and Oil
The hopper, trough and vibrating base are all made of food-grade stainless steel with polished, dead-corner-free surfaces, so nut fragments, oil and seasoning powder rinse away immediately. The vibrator motor is waterproof and the wiring is concealed inside the frame, allowing direct high-pressure hose-down. The hopper and trough use quick-release fixings and can be removed for cleaning or replacement within minutes, meeting the high-frequency changeover hygiene requirements of food factories.
7. Inverter Control and Fast Changeover — No Mechanical Adjustment
The machine is fully inverter-controlled, and vibration frequency and amplitude are set directly from the control interface. When switching nut varieties or changing pack weights, operators simply switch parameters — no trough dismantling or mechanical modification is needed. Changeover time drops sharply, making it normal practice for one line to run several varieties in a single day.
Technical Specifications
| Parameter | Specification |
| Equipment Type | Vibrate Feeder |
| Primary Function | Uniform feeding, constant-flow speed control and product-bed conditioning |
| Models | Single body FS02 / FS03 / FS04; twin body FS02 / FS03 |
| Hopper Size | Single 550 × 150 × 260 mm; twin 900 × 900 × 460 mm |
| Vibration Method | Electromagnetic / vibrator motor, inverter-controlled |
| Feeding Characteristic | Constant-flow output, continuous start-stop, interlocked with weigher level signal |
| Product-Contact Material | Food-grade stainless steel, polished, dead-corner-free |
| Cleaning Method | Waterproof and dust-proof, accepts high-pressure hose-down; quick-release hopper and trough |
| Installation | Mounted on the multihead weigher platform; height and interface customizable |
| Custom Options | Hopper and trough dimensions, vibration style, discharge direction to line requirements |
Role in the Nut Weighing and Packaging System
The complete nut weighing and packaging system workflow positions the feeding stage between elevating and weighing:
1. Bucket Elevator — Gently elevates nut material from floor to multihead weigher platform (gentle buckets, anti-chipping)
2. Inclined Conveyor — Low-angle, low-speed inclined conveying to elevator infeed, preventing rolling and breakage
3. Vibrate Feeder (this unit) — Conditions incoming product into an even thin bed and feeds it at constant flow into the weigher infeed funnel
4. Multihead Weigher — High-precision gram-level weighing, ensuring zero-error net weight per package
5. Metal Inspection & Weighing Machine — Finished package metal detection and weight verification, rejection of non-conforming units
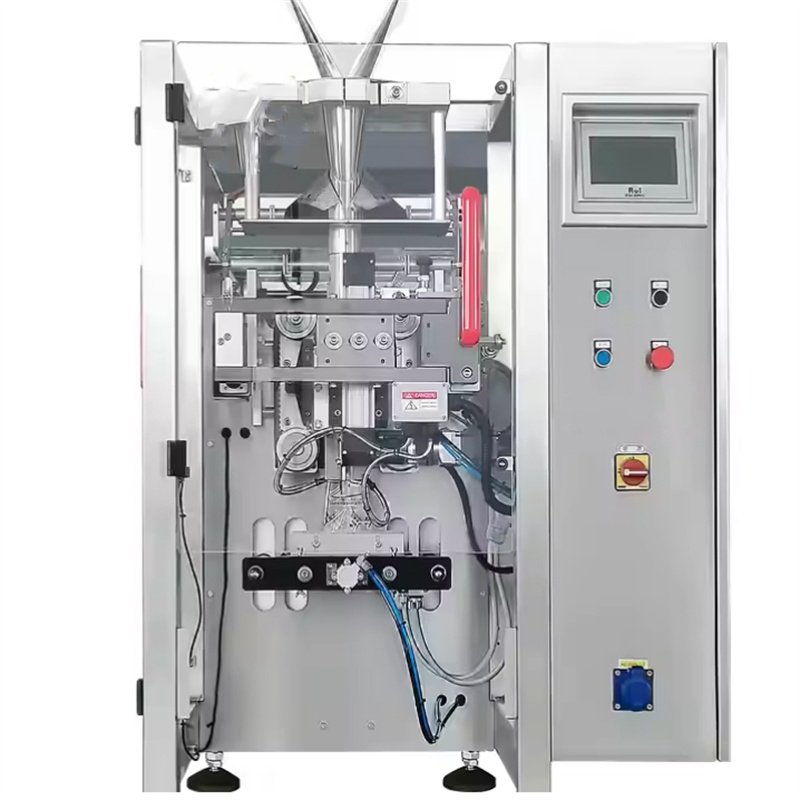
6. Packaging Machine — Bags and seals the weighed nut portions into finished packages
7. Turn Table — Buffers the finished packages and provides pick-off buffering for downstream case-packing
In this workflow the Vibrate Feeder is the upstream valve of the multihead weigher. Its output stability directly determines whether the weigher can run combination weighing at maximum frequency: with even feeding, every cycle receives sufficient product in a consistent distribution; with interrupted feeding, the weigher can only idle and wait. Globule designs the electrical control of the whole line, and the start-stop sequences and speed interlocks between the feeder, the weigher and the elevator are logic-verified before shipment — on site it is plug-in-and-run.
Applicable Products
Globule’s Vibrate Feeder is feed-optimized for the following materials in the nut weighing and packaging system:
High-value nuts — Macadamia nuts, almond kernels, cashews, pistachios, pecans
Mixed nuts and kernels — Multi-variety blends with wide differences in shape and density, requiring even single-layer feeding
Seasoned nuts — Salt-roasted, honey, butter and other flavored products containing seasoning powder, prone to arching and requiring anti-bridging design
Nut pieces and granular products — Small pieces and broken kernels requiring continuous, even feeding
Why Choose Globule’s Vibrate Feeder?
Specifically tuned for the high value and fragility of nuts. Generic feeders pursue conveying speed and pay little attention to tumbling and mutual compression inside the trough. Globule’s Vibrate Feeder starts from nut appearance and tunes vibration frequency, amplitude and bed depth accordingly — forward motion only, no tumbling — containing breakage and shell-cracking risk at the feeding stage.
A true closed loop with the multihead weigher. As original-system-matched equipment for the nut weighing and packaging line, this machine’s output capacity, level-interlock logic and control interface have been co-designed and validated with the multihead weigher on the same line. On-site installation enters the feed-and-weigh closed loop directly, with no additional commissioning.
Full-cycle delivery support. Globule provides complete delivery support from requirements confirmation, concept layout, equipment manufacturing and system integration through to commissioning and operator training, together with full drawings, sanitary design documentation and bilingual operation manuals — ensuring the feeder performs to its design specification within the complete nut weighing and packaging system.
Get a Custom Quote
To learn more about Vibrate Feeder technical specifications or complete line configuration solutions, please contact Globule’s engineering team:
Email: u[email protected]
Tel / WhatsApp: +86 13818737877
Address: No.28 Huiye Road, Songjiang District, Shanghai, China
Hygiene First · Safety First — Globule Sanitary Conveyor Pty Ltd