EN

- Overview
- Recommended Products
Overview
1. Product Overview
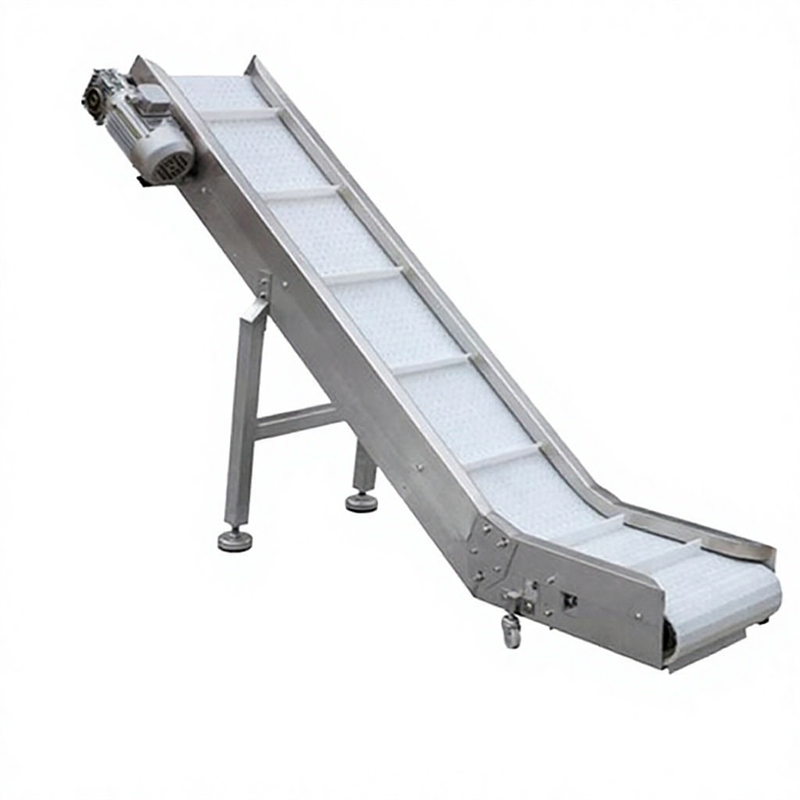
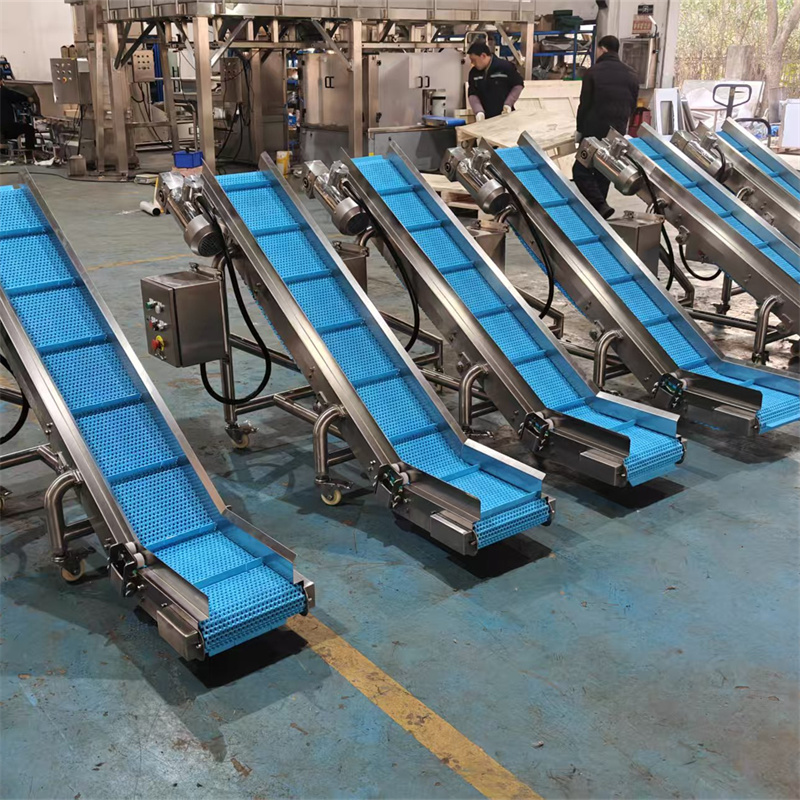
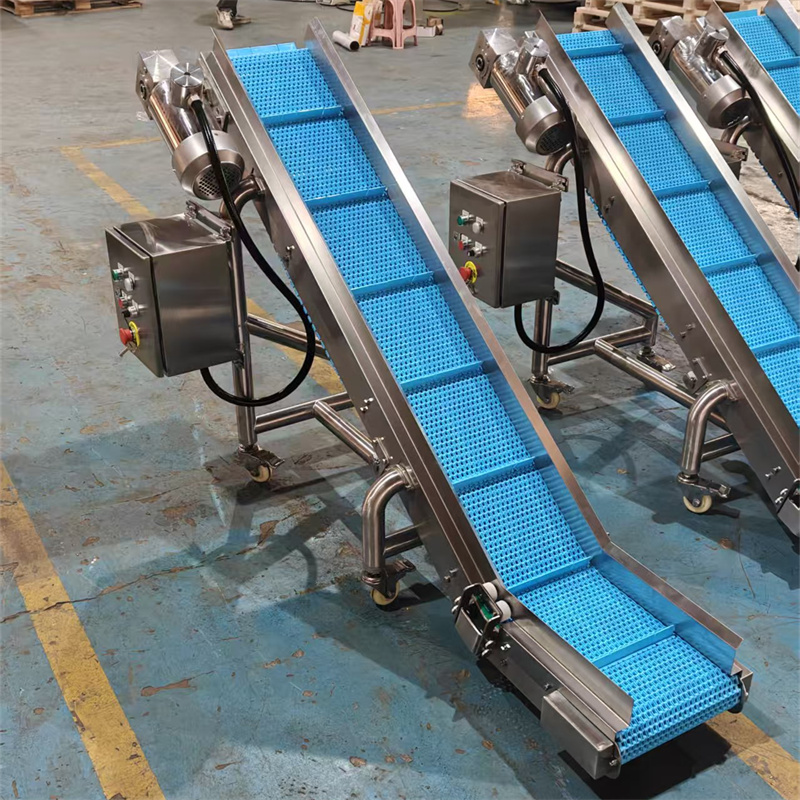
The Take-Off Conveyor is a rapid finished-product discharge system developed by Globule Sanitary Conveyor Pty Ltd for high-speed packaging machines. Installed immediately after the discharge outlet of the vertical form-fill-seal (VFFS) machine, it lifts freshly sealed bags away from the packaging area promptly and smoothly, handing them to the downstream merging conveyor or directly into case packing.
In the 2-in-1 Merging Line, one high-speed VFFS machine serves two weighing channels, so the bag discharge rate is extremely high and finished bags pour out in dense, continuous rhythm. If discharge is not smooth, the packer is forced to slow down or stop, and the capacity advantage of merging two lines is entirely cancelled out. The Globule Take-Off Conveyor is designed precisely for this "high-speed, dense, continuous" discharge duty: its belt speed is matched exactly to the packing rhythm, and the bag-receiving position and guiding geometry are optimized for the bag format, so every bag is caught firmly, carried away quickly and never piles up or jams.
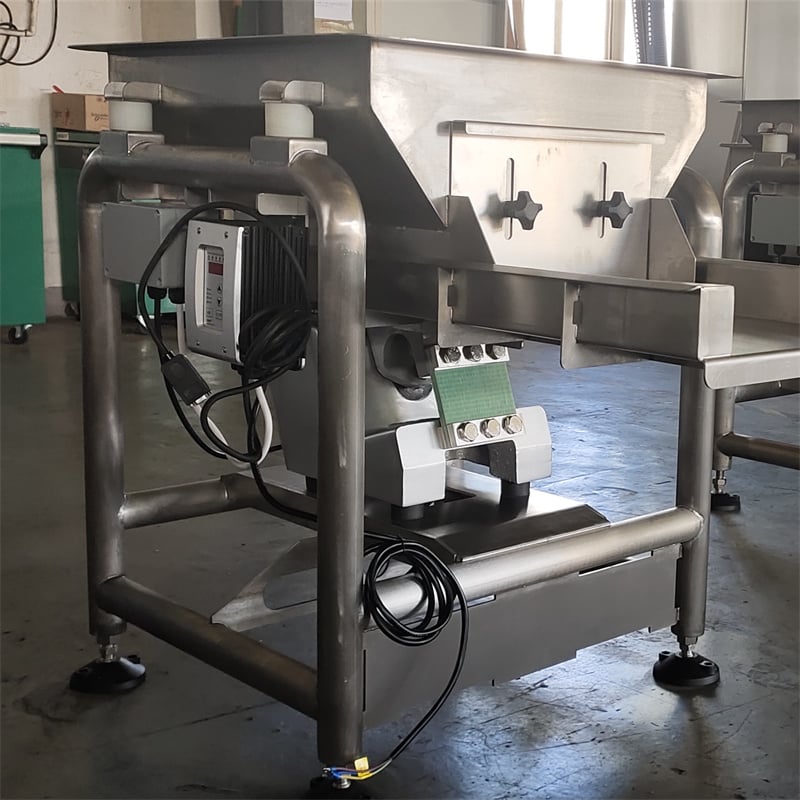
The whole machine carries Globule's line-wide hygienic design language: food-grade stainless steel round-tube frame, concealed wiring, whole-machine washdown and quick-release conveying parts. Because puffed-product bags are light, slippery and easily crushed, the take-off conveyor uses an appropriate belt surface and smooth transition design to minimize bag breakage and product shattering. Mounting height, length and angle can all be matched precisely to the packer and downstream conveyors for seamless connection.
Whether supplied as a standard component of the 2-in-1 Merging Line or retrofitted behind an existing packer of any brand, the Globule Take-Off Conveyor lets finished bags "get out fast, move away quickly and land safely" — the indispensable final baton of a high-speed packaging line.
2. Core Advantages
Advantage 1: Rhythm-matched — high-speed discharge without accumulation
The take-off conveyor interlocks with the packer's bag-discharge signal and its belt speed is infinitely adjustable, matching the machine's discharge rhythm per minute. No matter how fast the packer runs, every bag is removed in time, eliminating pile-ups, crushing and stoppage at the outlet. Under the high discharge frequency of a merged dual-line system, this "keep-up" ability is decisive.
Advantage 2: Optimized receiving and guiding — every bag lands correctly
The transition between the discharge outlet and the belt is specially engineered: receiving position, guide-plate angle and belt height are tuned to the bag dimensions and falling posture, so bags land in the correct orientation without tipping, skewing or jamming at the transition. For fragile products such as chips and egg yolk cakes, the transition minimizes drop impact and protects product integrity.
Advantage 3: Adjustable structure — flexible match with downstream processes
Frame height is adjustable, and conveyor length and discharge direction can be designed around the layout of the downstream merging belt, packing table or palletizing station. Horizontal and inclined configurations are available. It can connect to a Globule merging conveyor to form a complete rear logistics section, or connect directly to the customer's existing case-packing line — flexible and easy to adapt.
Advantage 4: Hygienic design — no dead corners, easy cleaning
The food-grade stainless steel round-tube frame has no dead corners; belt and rollers are quick-release for daily cleaning; the whole machine is washdown-capable to FSMA sanitary design guidelines; concealed wiring eliminates dirt traps and safety hazards. The machine's look is fully consistent with the rest of the 2-in-1 Merging Line, keeping the workshop clean and professional.
Advantage 5: Stable and durable — low-maintenance peace of mind
The conveying parts use mature, reliable drive technology that runs smoothly, quietly and for a long service life. The simple structure means few daily maintenance points. For a high-speed packaging line running long continuous shifts, the reliability of the take-off conveyor directly affects line availability — Globule's solid workmanship keeps production running.
3. Technical Specifications
| Item | Specification / Description |
| Equipment | Rapid finished-bag take-off conveyor |
| 2-in-1 role | Rapid discharge of finished bags |
| Position in line | After the VFFS discharge outlet |
| Frame material | Food-grade stainless steel, round-tube frame |
| Belt material | Food-grade, selected by product |
| Speed control | Variable-frequency drive, interlocked with packer discharge rhythm |
| Hygiene design | Whole-machine washdown, quick disassembly, no dead corners |
| Wiring | Concealed wiring |
| Suitable products | Bagged puffed products: potato chips, corn chips, egg yolk cakes, etc. |
| Customization | Height/length/angle/discharge direction per line layout |
| Note | Detailed dimensions and load data are engineered per packer model and bag format; refer to the official proposal |
4. Role in the 2-in-1 Merging Line
The 2-in-1 Merging Line merges the capacity of two weighing channels into one high-speed VFFS machine, so the product flow at the packer's outlet is nearly double that of an ordinary single line. The take-off conveyor is the first link to carry this high-speed, dense flow — the first landing point for finished bags after they leave the packer.
In the system, the take-off conveyor performs the critical duty of rapid transfer: it moves each bag away from the outlet immediately, making room for the next bags that keep coming, so the packer never backs up; then it hands the bags, in correct orientation and spacing, to the Metal Inspection and Weighing Machine or the merging conveyor. Its belt speed, bag-catching posture and transition smoothness directly affect bag-breakage rate, inspection accuracy and the smoothness of downstream merging.
If the 2-in-1 Merging Line is a high-speed relay race — the multihead weighers "weigh fast and accurately", the VFFS machine "bags well" — then the take-off conveyor is the critical baton: catch it firmly and pass it fast, and the whole line runs in one smooth breath. With stable rhythm matching and reliable conveying, the Globule Take-Off Conveyor ensures the fruits of high-speed packaging are caught steadily and carried away promptly.
5. Why Choose Globule
Born for high-speed discharge
● : designed for high-frequency, continuous bag discharge, with rhythm-matching proven under merged dual-line conditions.
One hygiene standard across the line
● : round-tube frame, whole-machine washdown, quick disassembly and concealed wiring — seamlessly integrated and visually consistent with the 2-in-1 Merging Line.
We understand puffed-food bags
● : receiving and transition details are optimized for light, brittle, crush-prone bags, minimizing bag breakage.
10+ years of engineering experience
● : our core team has long served the food-packaging industry; solutions are mature and reliable, with guaranteed delivery and after-sales support.
Flexible for existing lines
● : available as the standard configuration of the 2-in-1 Merging Line or as a retrofit behind any brand of packer — one machine, many uses.
6. Contact Us
● Company: Globule Sanitary Conveyor Pty Ltd / Shanghai Lingan Equipment Manufacturing Co., Ltd.
● Email:
● Tel: +86 13818737877
● Address: No.28 Huiye Road, Songjiang District, Shanghai, China