EN

- Overview
- Recommended Products
Overview
1. Product Overview
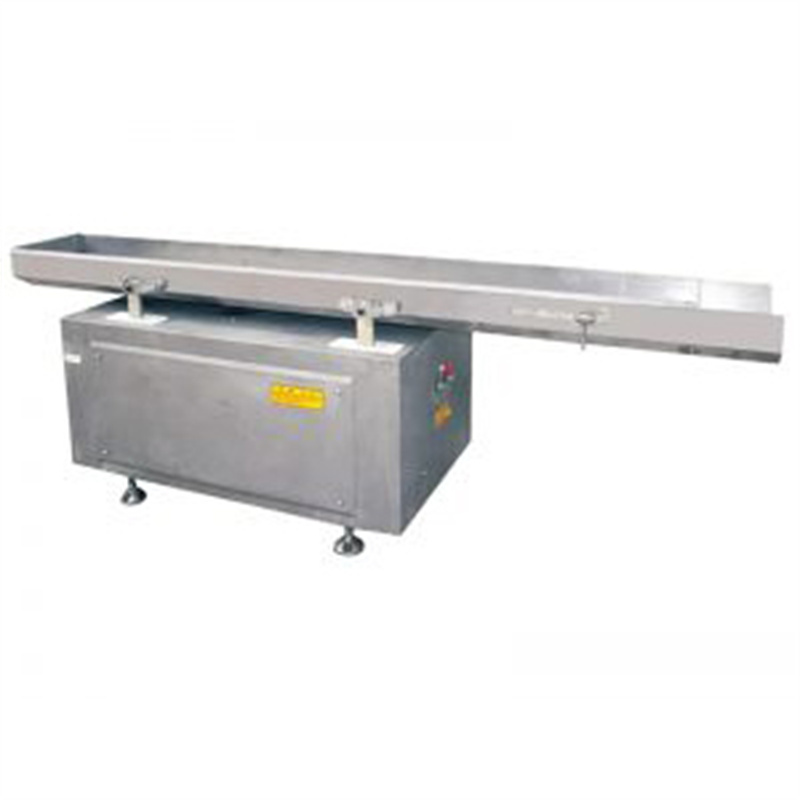
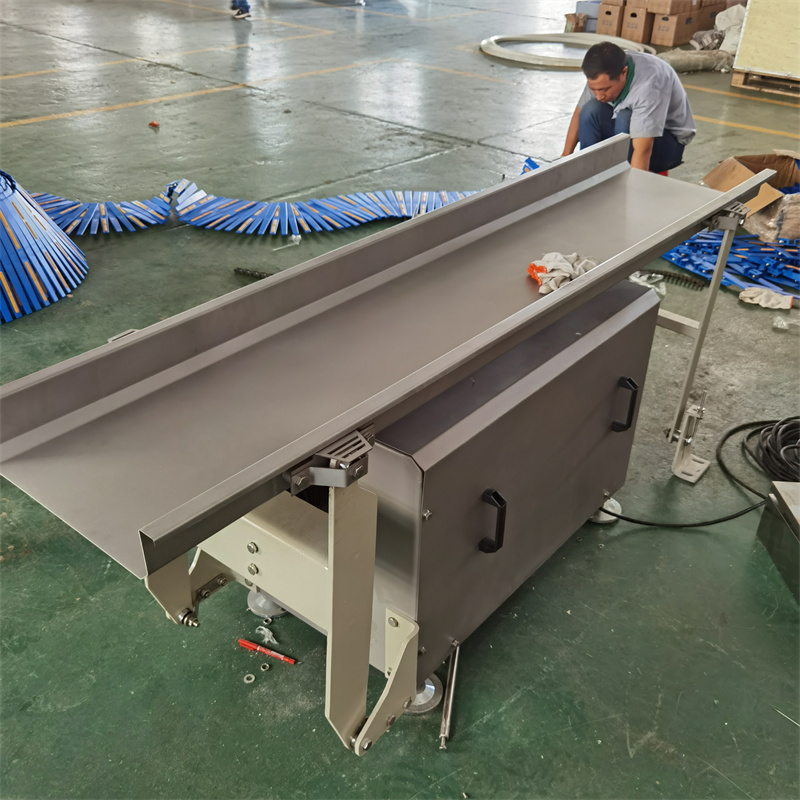
The Fast Back Conveyor is the core machine of the "material return section" on a puffed-snack packaging line. It does not sit in the main flow but on a bypass of it, returning overflow from the high-level buffer hopper, surplus from the multihead weigher and rework product from the packing and inspection stages back to the head of the line or to a distribution point at a controlled speed, so that it re-enters the production cycle.
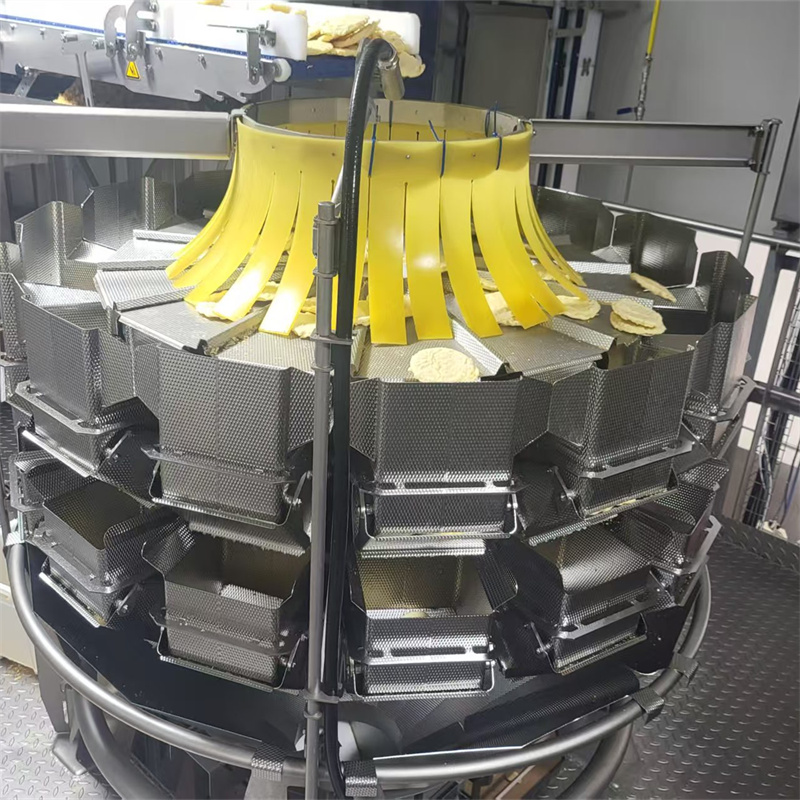
A physical reality of any high-speed puffed line: the multihead weigher takes product in combination-weighing cycles and its take-up frequency changes constantly, while the bucket elevator and inclined conveyor tend to feed continuously and steadily. The instantaneous difference between the two necessarily produces overflow. Without a return path, that overflow can only pile up in the hopper or in the feeding section — at best causing bridging and interrupted feeding, at worst being lifted again and again until product breaks and the equipment is overloaded.
The Globule Fast Back Conveyor uses a reciprocating "slow-forward, fast-back" conveying principle to return overflow and rework material to the head of the line quickly and with low impact and low breakage. It is interlocked with the level signals of the bucket elevator, vibrate feeder and multihead weigher, so the entire single line keeps its material balance automatically in both high-output and overflow conditions.
The machine is designed and manufactured by Shanghai Linguan Equipment Manufacturing Co., Ltd. (Globule Sanitary Conveyor Pty Ltd). It is built in food-grade stainless steel with hygienic construction, complies with FSMA hygienic design criteria, and follows the brand philosophy of "Hygiene First · Safety First".
2. Position in the Puffed-Snack Packaging Line
The complete material flow of a puffed line is: inclined conveyor / bucket elevator → high-level buffer hopper → vibrate feeder → multihead weigher → vertical bagging machine → take-off conveyor → metal detection and weighing unit → cartoning/palletizing. The Fast Back Conveyor connects to this flow as a bypass machine and performs three tasks:
● Overflow return: when hopper level reaches its upper limit, surplus product passes through the bypass into the fast back conveyor, which returns it to the head of the line or to a distribution point at a controlled speed;
● Rework return: rework product rejected by the packing and inspection stages is collected and returned, re-entering the production cycle for redistribution;
● Cadence interlock: the return speed is interlocked with the elevator output and the weigher level signal, preventing excessive return from flooding the line head and preventing lagging return from overfilling the hopper.
Unlike schemes that treat overflow as waste, this machine is designed for a zero-waste closed loop: overflow never touches the floor, never accumulates and is never lifted twice — it all goes back to the head of the line for redistribution by the inclined conveyor and modular belt conveyor. For puffed snacks and nuts, where raw material cost is sensitive, the reduction in overflow loss alone is enough to pay back the machine within a year.
3. Core Advantages: Fast Overflow Return and Dynamic Material Balance
1. Slow forward, fast back — low-impact return. The deck first carries the product slowly forward by one step, then returns quickly to the start position to await the next group. The forward phase runs at low speed and low acceleration, so product keeps its spacing without tumbling or stacking; the return phase is unloaded and fast, never touching the product on the deck, so cycle loss is minimal and continuous feeding capability is unaffected.
2. Specially optimised return curve suppresses reversing vibration. Reversing is where machines of this type most often fail: once vibration gets out of control it shatters fragile puffed product and accelerates fatigue in the frame and drive. The fast-return motion curve of this machine is specially optimised so that reversing vibration is strongly suppressed — protecting product integrity and extending frame and drive life.
3. Cadence interlock with the elevator and weigher keeps the system balanced. Level detection is provided between the elevator top and the buffer hopper; when the hopper is full, surplus product enters the fast back machine through the bypass. Elevator output and return speed are interlocked, so the system self-balances in both high-output and overflow states, eliminating material accumulation and the breakage caused by repeated lifting.
4. Low breakage as the number-one index — compact and easy to maintain. Slow-forward/fast-back combined with the vibration-reduced curve keeps fragile, irregular product completely collision-free throughout the return path. The reciprocating structure has none of the classic belt-tracking or idler-wear problems, with fewer moving parts and simple construction — low maintenance frequency and low spare-part consumption. It also needs no long conveyor run to hold buffer volume, significantly shortening line length and freeing valuable floor space.
4. Structure and Hygienic Design
● Food-grade stainless steel contact surfaces: the trough and frame are food-grade stainless steel with polished, dead-corner-free surfaces; oil, crumbs and seasoning powder rinse away instantly, consistent with the brand’s whole-line design language;
● No belts, no idlers: the reciprocating structure eliminates belt tracking and idler wear at the root, and also removes the dirt-trapping dead zones common behind belts and at idlers;
● Quick-release and washable: waterproof, isolated electrics with wiring concealed inside the frame accept direct high-pressure hose-down, meeting the frequent cleaning demanded by high-oil and seasoning-powder puffed-snack conditions;
● Safety and low noise: moving parts are fully guarded with safety interlocks and a drive-side emergency stop, meeting export equipment safety standards; measured noise is only 65 dB, far below plant limits, giving operators a quiet and safe workplace.
5. Technical Specifications
| Parameter | Value / Option |
| Function | Controlled return of overflow and rework material; dynamic whole-line material balance |
| Conveying principle | Reciprocating conveying (slow-forward, fast-back, step-wise advance) |
| Max conveying speed | 12 m/min |
| Return curve | Specially optimised to suppress reversing vibration |
| Breakage rate | Low (core design index) |
| Noise | ≤70 dB (65 dB measured) |
| Construction | No belts or idlers; compact, space-saving, low maintenance |
| Cleaning | Food-grade stainless steel; in-place hose-down / quick-release washing |
| Installation | Customised on site, flexible mounting |
| Custom options | Conveying length, width, step and cadence to site conditions |
6. Integration with the Whole Line
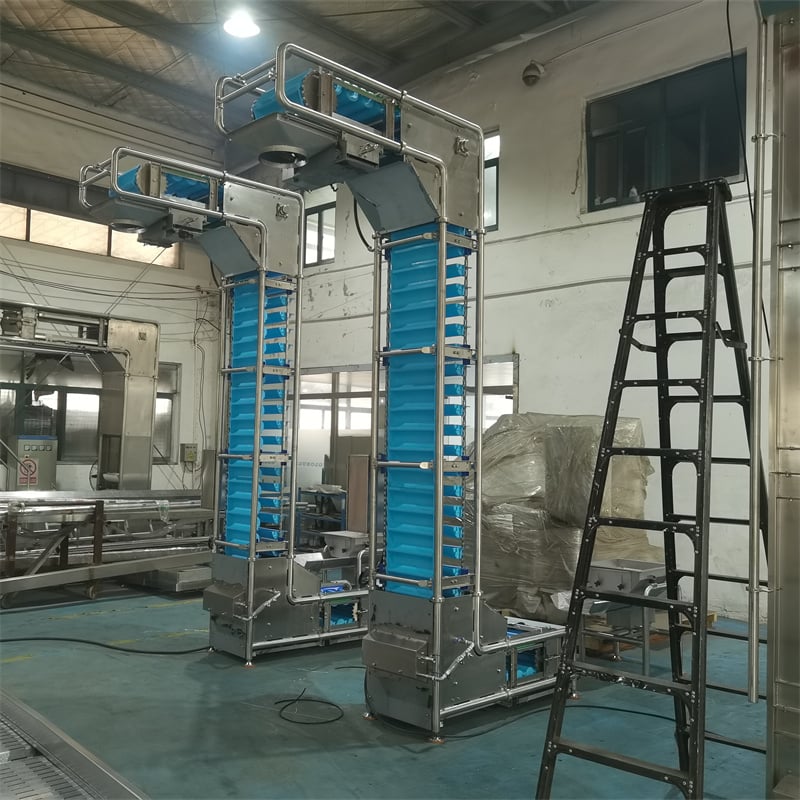
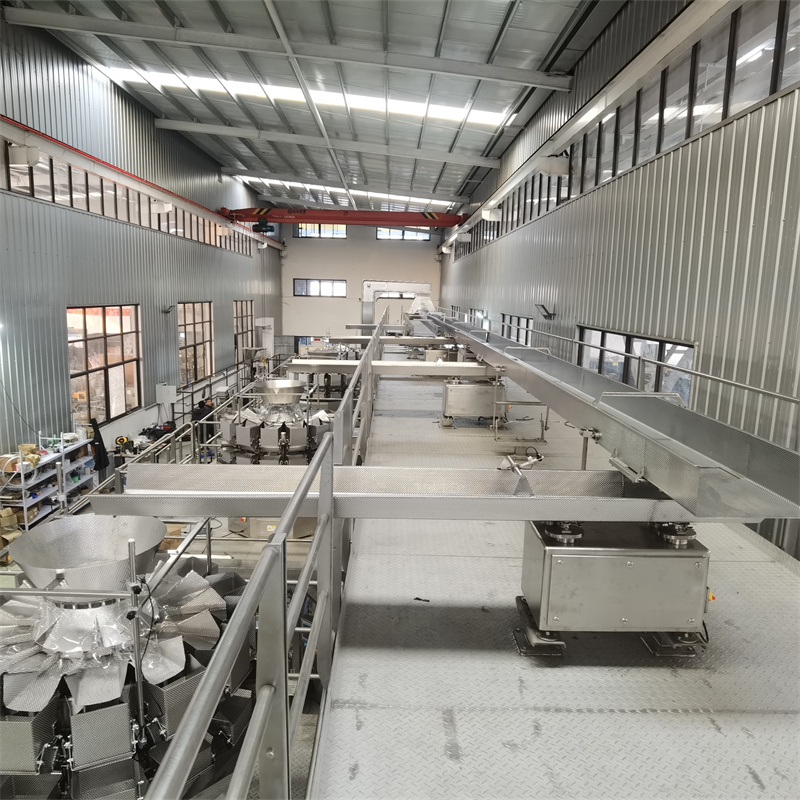
The Fast Back Conveyor is the lower half of the "vertical feeding + fast-back return" loop of a puffed line, and forms a linked unit with the bucket elevator: upward, the elevator keeps delivering product to the high-level buffer hopper; downward, the fast back machine returns surplus and rework material promptly to the front end. The two are interlocked so the single line is always both well supplied and free of accumulation.
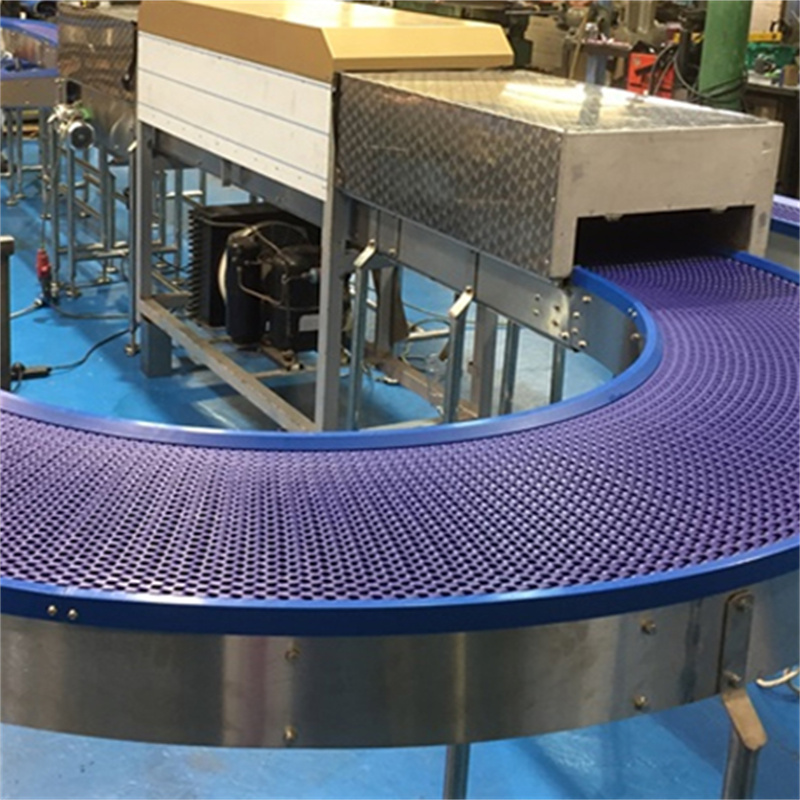
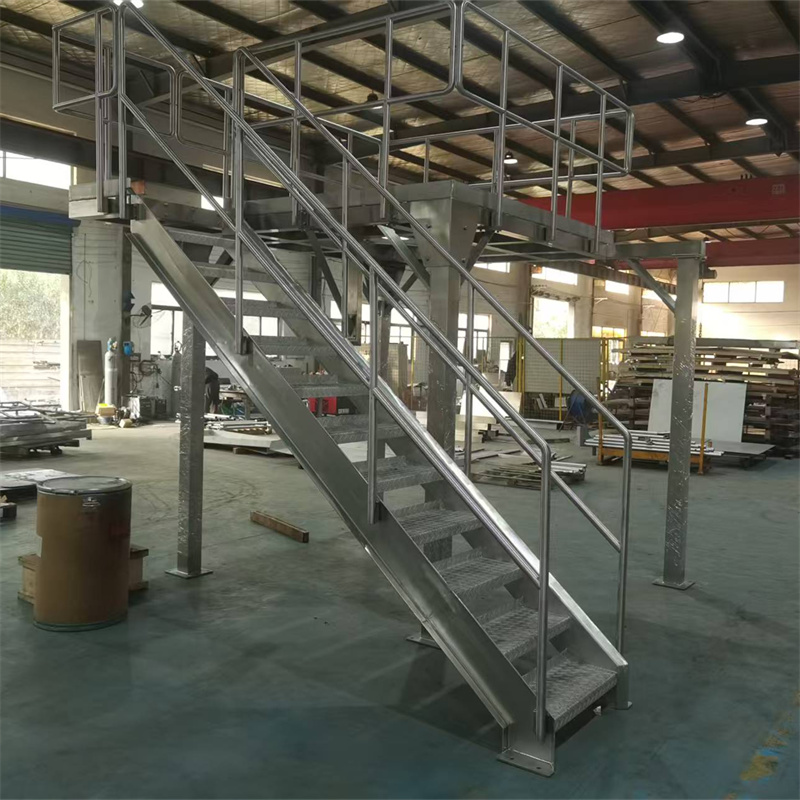
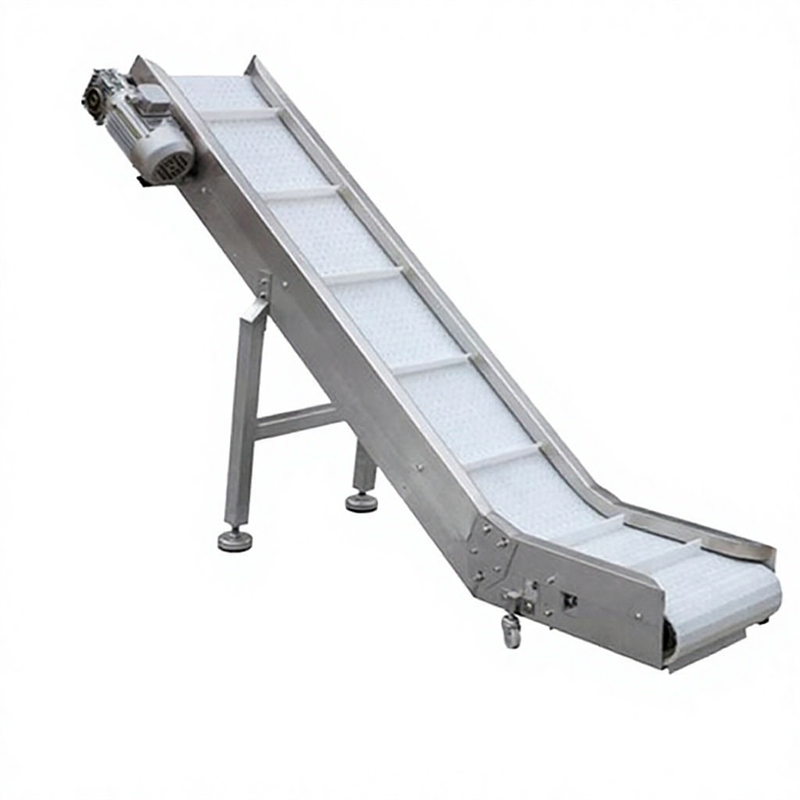
After redistribution at the line head, returned material is fed back into the production cycle by the inclined conveyor and modular belt conveyor. The weigher’s level requests are linked in real time with the speeds of the feeder, elevator and fast back machine, keeping the scale running in its optimum level window. When weigher supply fluctuates briefly, the vertical bagging machine adjusts cadence in coordination with the fast back machine: overflow is returned to the front end for redistribution, so the bagger produces no empty or half-filled bags and both film and product utilisation stay high. Globule programs the whole line’s electrical control, and start-stop sequences and speed interlocks are logic-verified before shipment — on site it is plug-in-and-run.
7. Suitable Products and Conditions
● Overflow and rework return for sheet-type puffed snacks such as potato chips and prawn crackers;
● Light round products such as popcorn and corn balls (breakage-reducing return, less damage from repeated lifting);
● Nuts and mixed kernels — bulk products sensitive to raw-material cost where material balance must be maintained;
● High-speed single lines where the multihead weigher takes product frequently and occasional overflow occurs;
● Line layouts with limited space that need a compact structure instead of a long conveyor run.
8. Quality and Service
Shanghai Linguan Equipment Manufacturing Co., Ltd. was founded in 2019, and our engineering team has more than ten years of experience in food conveying and packaging-line design, strictly following FSMA hygienic design criteria. The conveying length, width, step and cadence of the Fast Back Conveyor are all customised to site conditions. It can be purchased as a single machine or designed and commissioned together with the bucket elevator, vibrate feeder, multihead weigher, modular belt conveyor, stainless steel platform and vertical bagging machine. Full drawings, hygienic design documentation and bilingual operation manuals are supplied, together with on-site installation and commissioning, operator training and remote technical support.