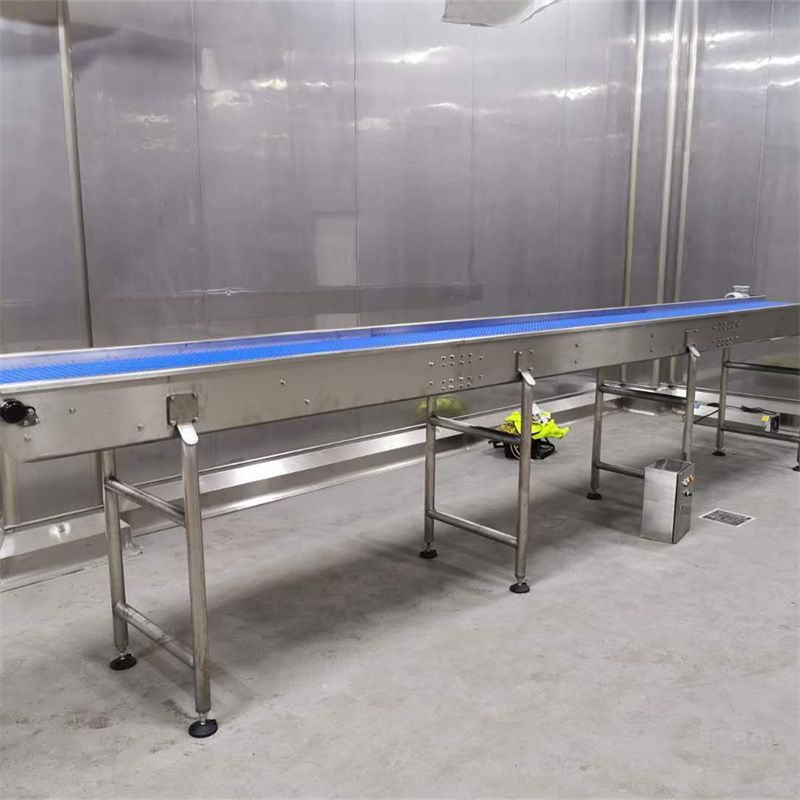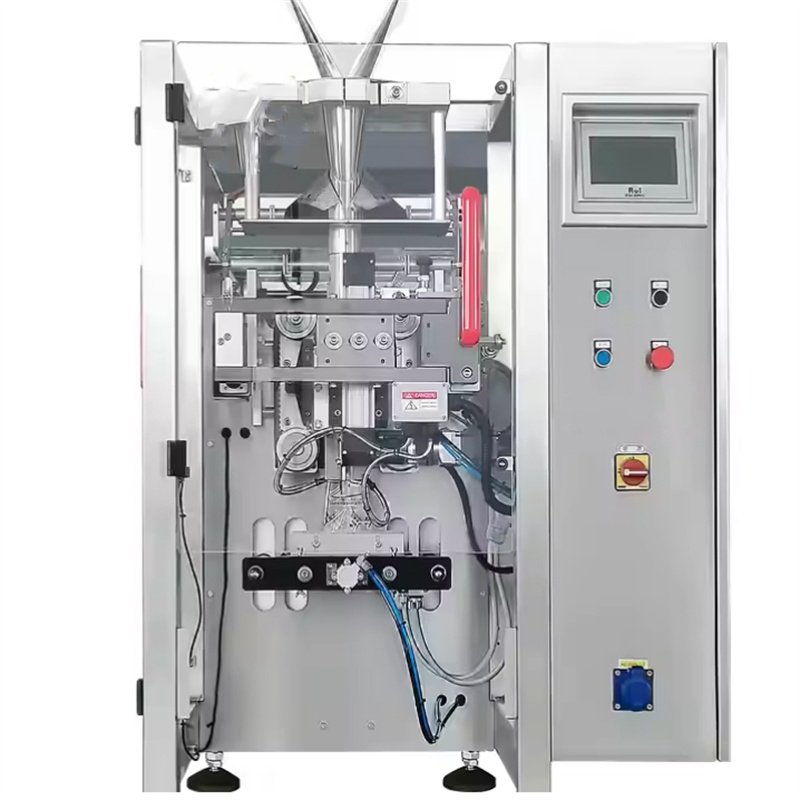
Globule Sanitary Conveyor Pty Ltd provides a high-performance Two-in-one Confluence Line, designed to seamlessly merge products from dual-stream packing units into a single high-speed downstream flow, maximizing throughput while maintaining strict food safety standards.
System Overview: In high-volume food production, managing output from multiple packaging machines can create bottlenecks. Globule Sanitary Conveyor Pty Ltd engineered this Two-in-one Confluence Line to synchronize and merge separate product streams into a unified, orderly conveyor path for efficient secondary packaging.
Key Technical Features:
Intelligent Merging Logic: Uses precision sensors and PLC-controlled gating to ensure products from two lines interleave without collisions or jams.
High-Speed Confluence: Engineered for seamless transition at speeds matching the highest output of dual VFFS or rotary packing machines.
Washdown-Ready Construction: Full SUS304 stainless steel frame with an open-profile design, enabling rapid, tool-less cleaning for high-hygiene environments.
Synchronized Infeed Control: Integrates with upstream fillers and weighers to automatically balance line loads and prevent downstream overflow.
Core Benefits: Achieve a 50% reduction in downstream equipment footprint and a significant increase in sorting efficiency, ensuring a continuous, non-stop packaging process.
 EN