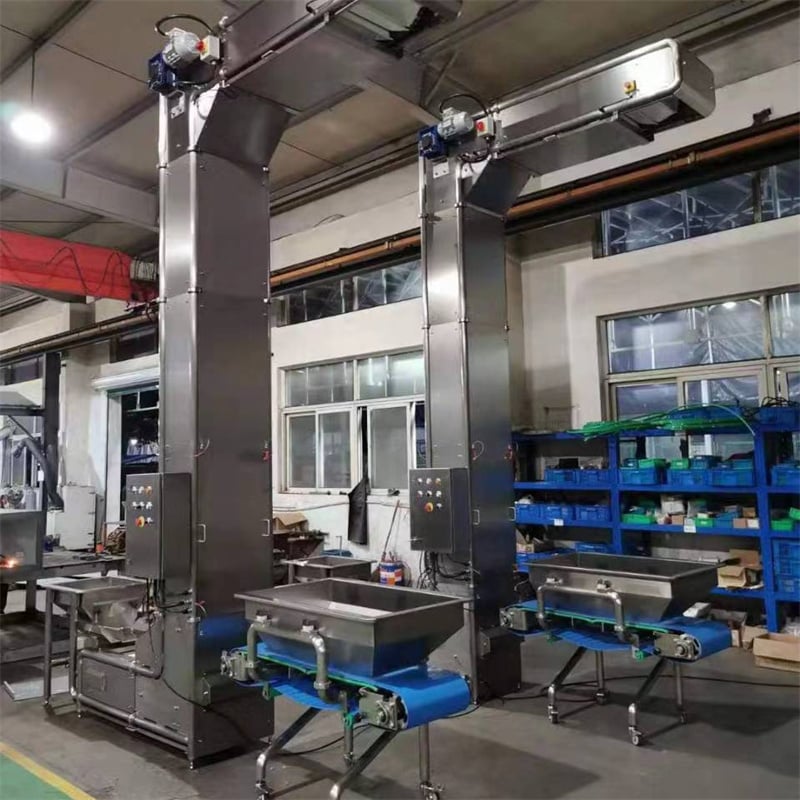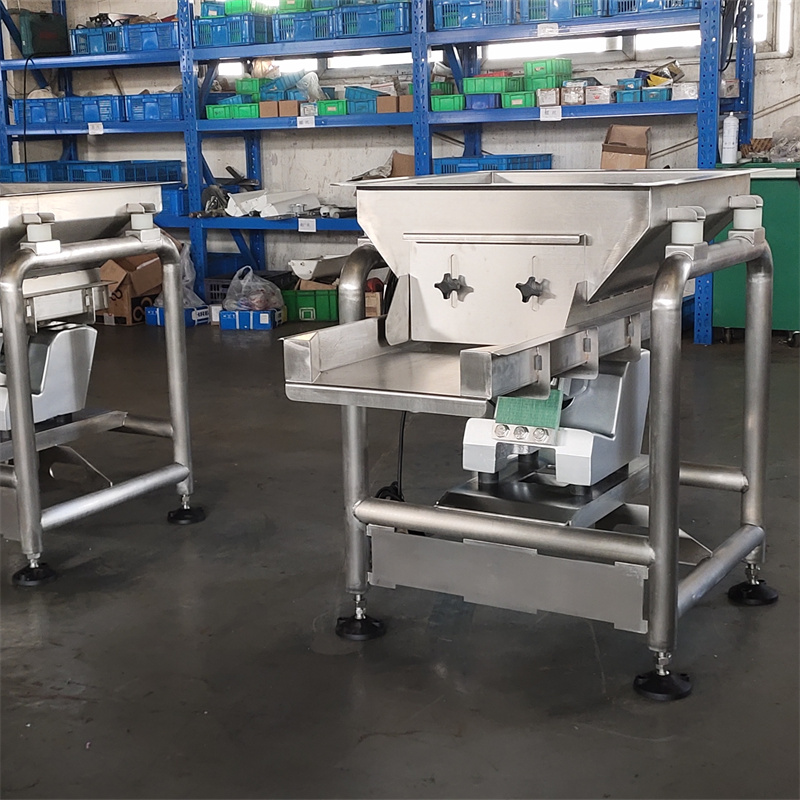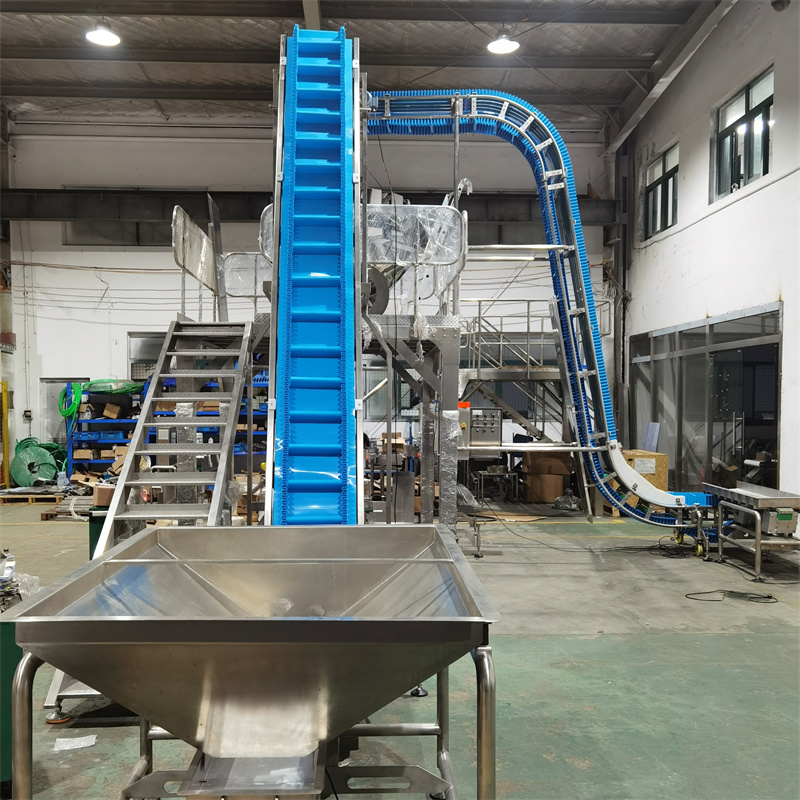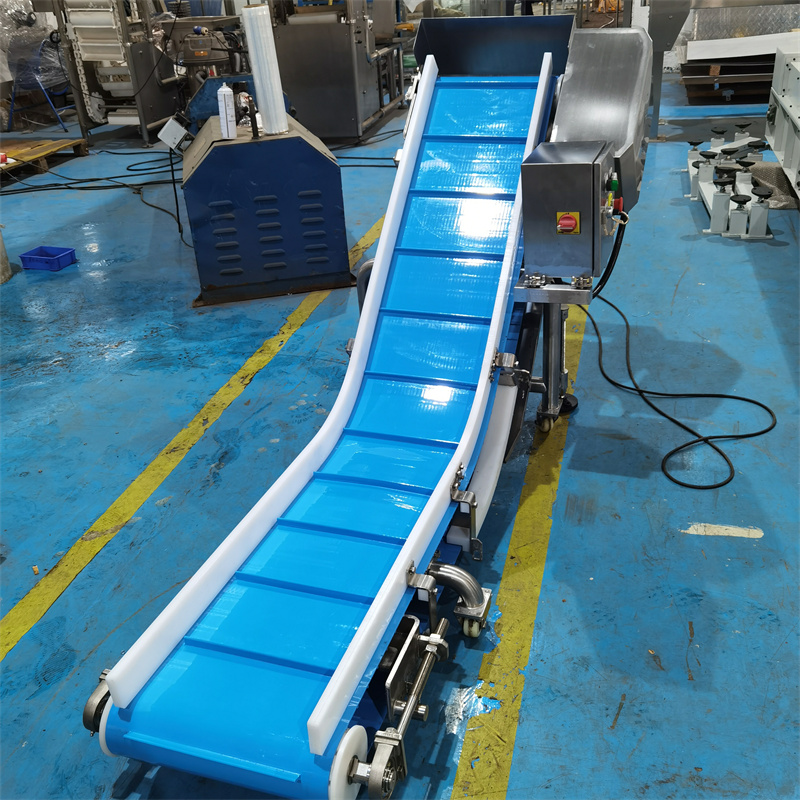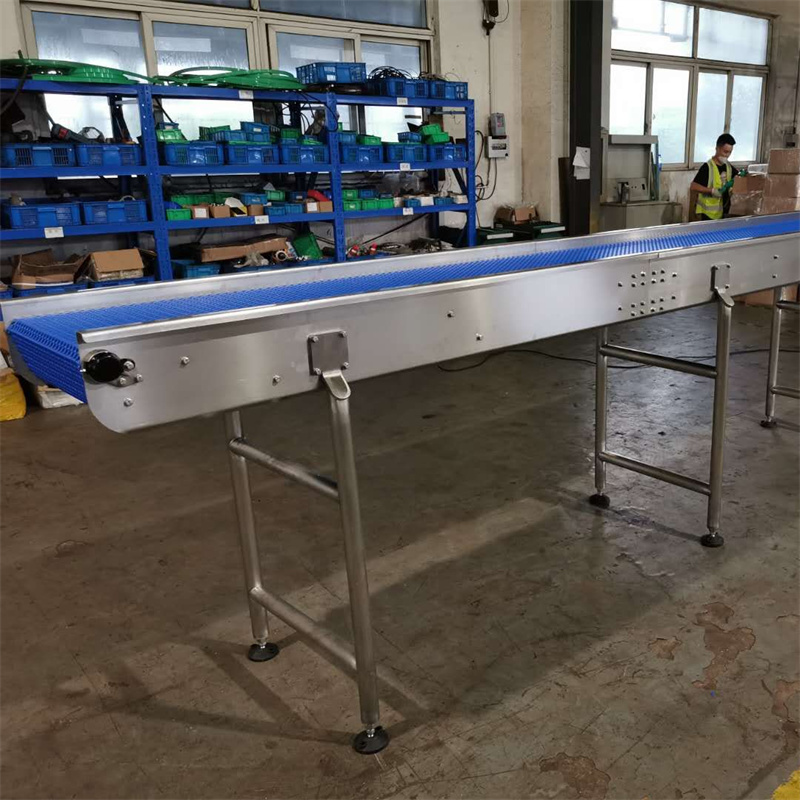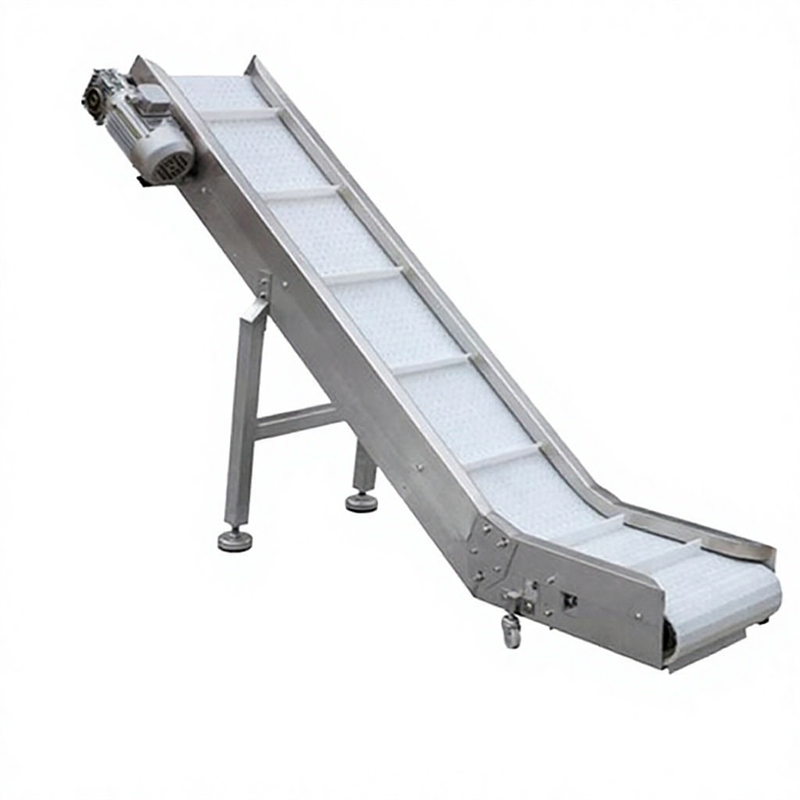
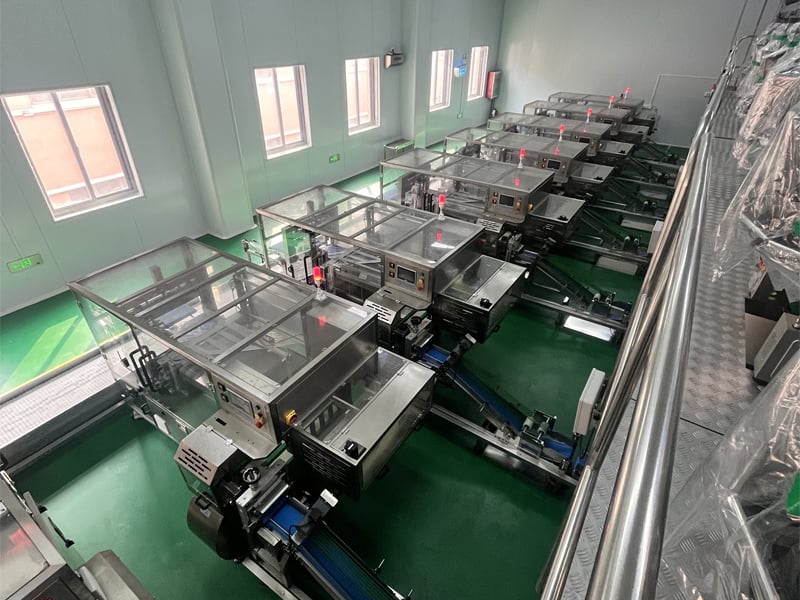
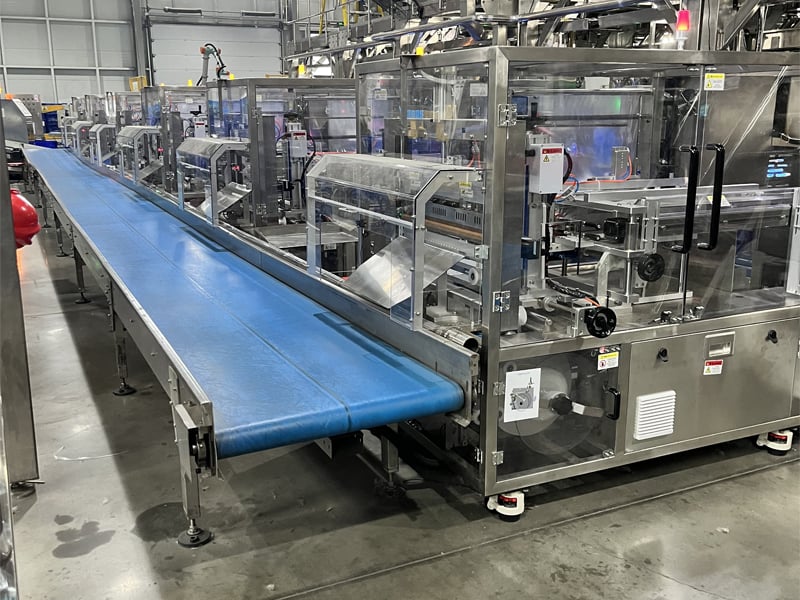
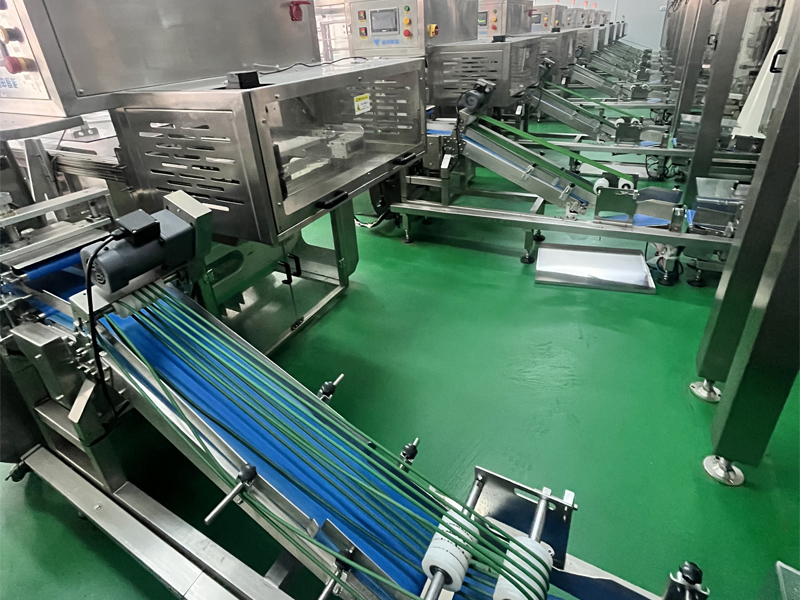
In the modern food industry, safe, efficient, and intelligent secondary packaging is a crucial link in ensuring product value and enhancing brand image. Leveraging its deep understanding of industry needs and continuous technological innovation, GLOBULE SANITARY CONVEYOR PTY LTD. provides clients with customized intelligent integrated secondary packaging system solutions, helping food companies improve quality, increase efficiency, and reduce costs in the packaging process. Globule Sanitary Conveyor Pty Ltd offers an intelligent integrated secondary packaging solution, automating the transition from individual pouches to bulk bagging or cartoning with 100% precision and significantly reduced labor costs.
Core Value: Modern food production demands efficient, high-speed secondary packaging. Globule Sanitary Conveyor Pty Ltd delivers modular systems that adapt to bags, boxes, or bottles, ensuring rapid changeover and superior shelf appearance.
Typical Process:
Intelligent Sorting: Directional conveying of individual units to the packing station.
Precise Bundling: Automatic assembly into preset patterns (e.g., 2x3, 5x10) and secure wrapping.
Auto-Bagging/Cartoning: Seamless loading into large baler bags or display cases, with optional accessory insertion.
Data Traceability: Integration with labeling and coding systems for full product life-cycle management.
 EN