EN

- Overview
- Recommended Products
Overview
1. Product Overview
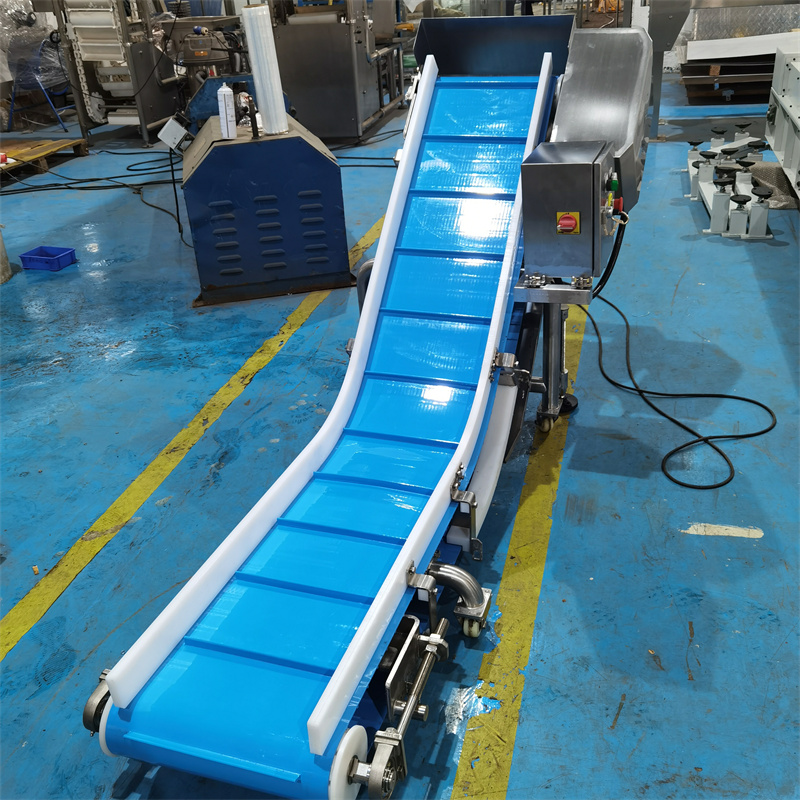
This conveyor is the standard transfer unit inside Globule's Secondary Packaging System, purpose-built for orderly queuing transport of finished small packs. In a secondary packaging line, finished packs — already formed and sealed retail pouches from the upstream line — must travel to downstream machines such as the bucket elevator, vibrate feeder, multihead weigher or the secondary (bundling) packaging machine in tidy rows at a steady pace. This conveyor is therefore not a simple "transporter". Its real jobs are queue management and pacing synchronisation: every row keeps the same spacing, the same orientation and the same speed, so the whole line runs like clockwork.
Founded in 2019 with an engineering team of more than ten years of experience in food-grade and sanitary conveying equipment, Globule designs and builds in line with FSMA sanitary design guidelines. From structure and materials to control logic, this machine is engineered to food-factory standards — fully cleanable, reliably interlocked and quick to maintain — and suits the secondary packaging of biscuits, confectionery, extruded snacks, nuts, daily chemicals and pharmaceutical finished packs.
2. Position and Process Role in the Secondary Packaging Line
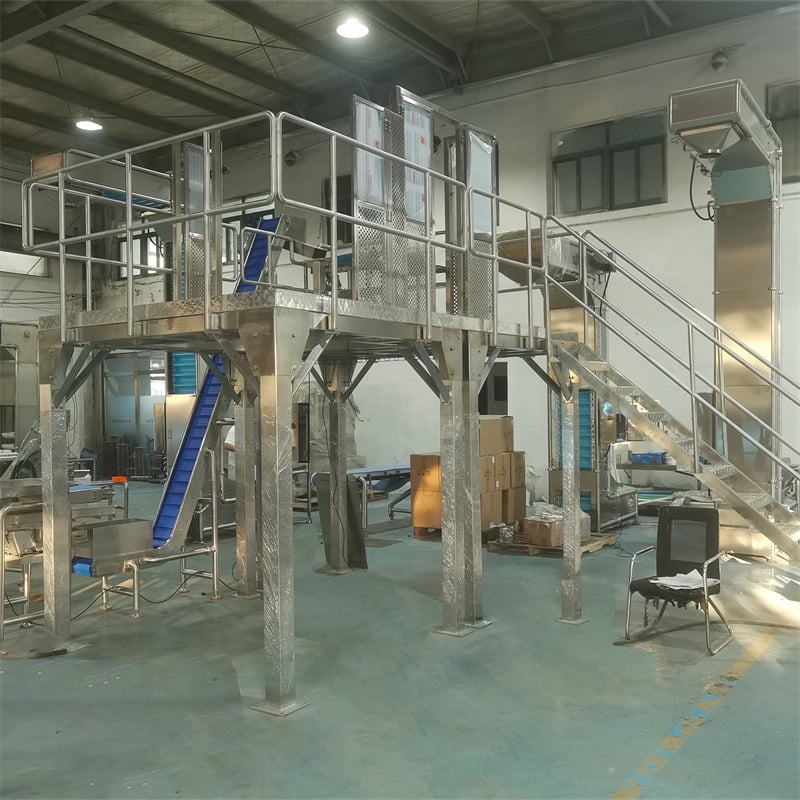
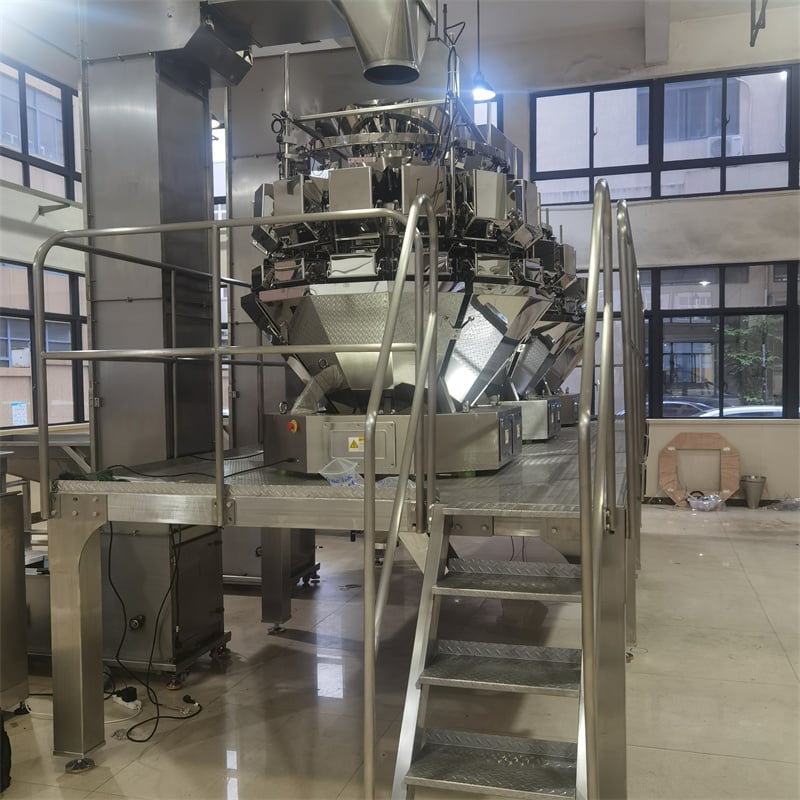
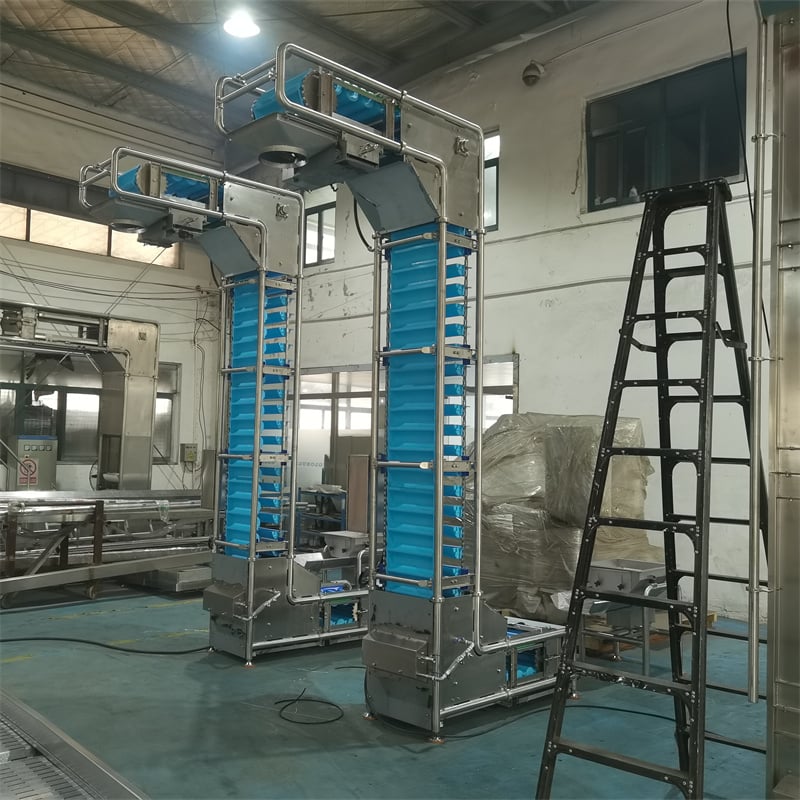
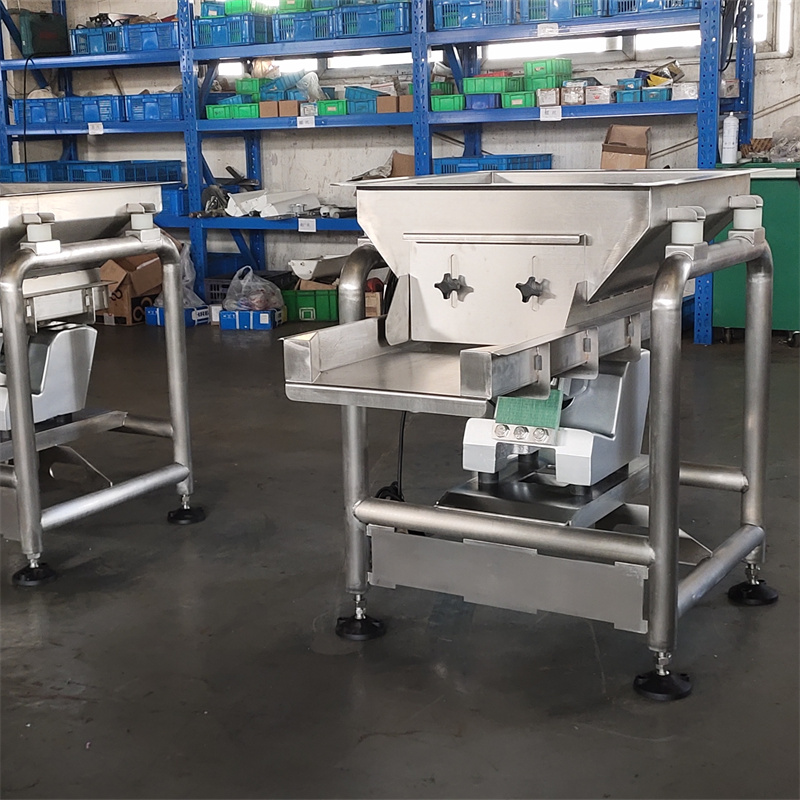
The secondary packaging system comprises the bucket elevator, vibrate feeder, multihead weigher, fast-back conveyor, stainless platform, secondary packaging machine, packaging machine and conveyors. The conveyor typically serves one of three stations:
Front-end takeover section
1. — receiving finished packs discharged from the bag-making / primary packing machine and converting an irregular, high-speed flow into a single orderly, evenly spaced queue;
Mid-line pacing section
2. — holding a stable supply between the multihead counting/checkweighing stage and the bundling machine, smoothing out the burst-type flow of upstream discharge;
End-of-line takeaway section
3. — carrying bundles/medium packs to the packaging machine for final big-bag or carton packing.
Whatever station it serves, the conveyor is interlocked with the neighbouring machines through photoelectric sensing and PLC signals: it automatically slows or pauses when the downstream machine is full, and automatically feeds when a gap appears. This prevents the vicious cycle of "blockage — stop — restart" and ensures the line's 80–120 packs/minute secondary packaging rhythm is actually delivered.
3. Differentiation from Other Conveyor Versions
In a powder plant a conveyor may provide dust-tight transfer; in a batching plant it may blend multiple ingredients; another version merges two finished lines into one stream. The conveyor presented on this page is entirely different in purpose:
● It carries
already-formed finished packs
, not powder, granules or bulk material — so there is no dust hood and no weighing hopper; its priority is protecting the pack's appearance;
● Its core capability is
queuing
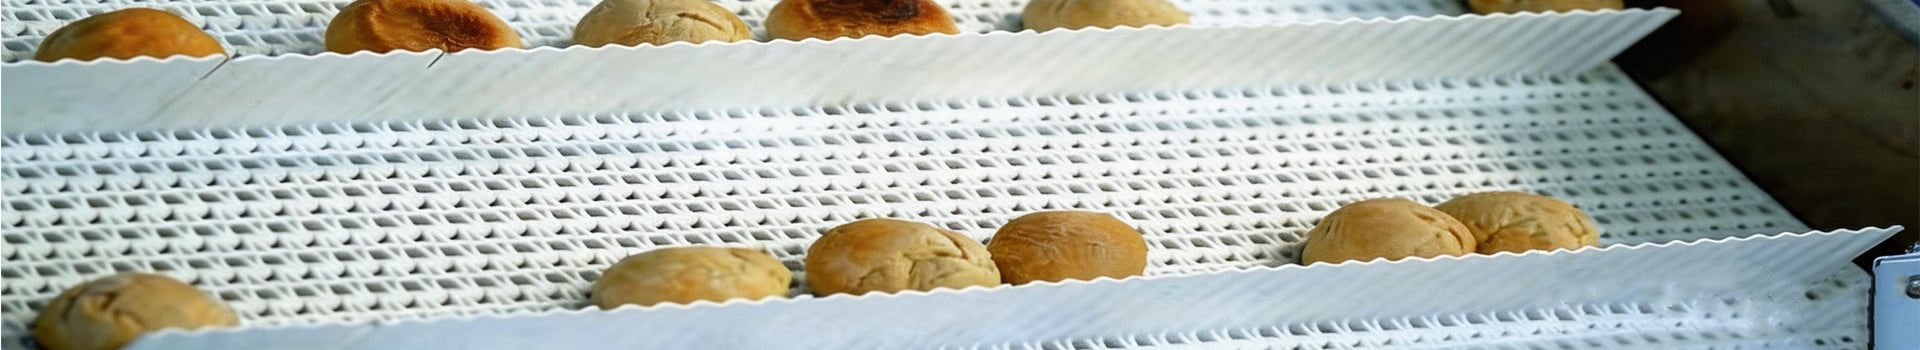
: side guides, lane dividers and photoelectric checks keep the product single-layer, single-file and evenly spaced, giving the downstream counting/check-weighing and wrapping stages a stable rhythm;
● Its control focus is
pacing synchronisation
: variable-speed interlocking with upstream and downstream equipment prevents overlapping packs, mis-feed and accumulation inside the line.
Put simply: other conveyors solve "moving material from A to B"; this one solves "moving finished packs from A to B in neat, evenly spaced rows at exactly the right speed".
4. Construction and Design Highlights
Hygienic frame
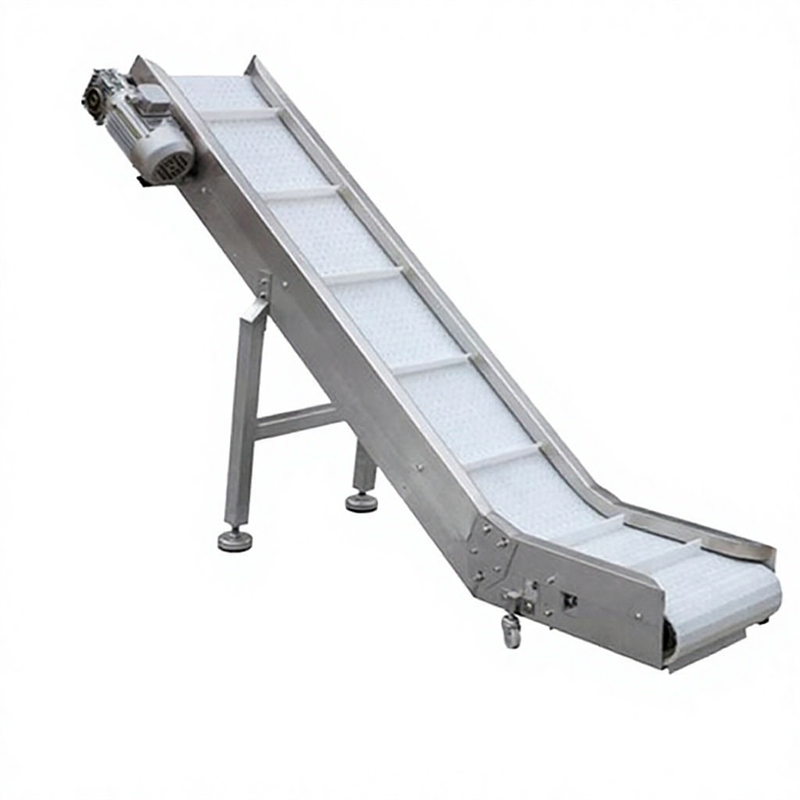
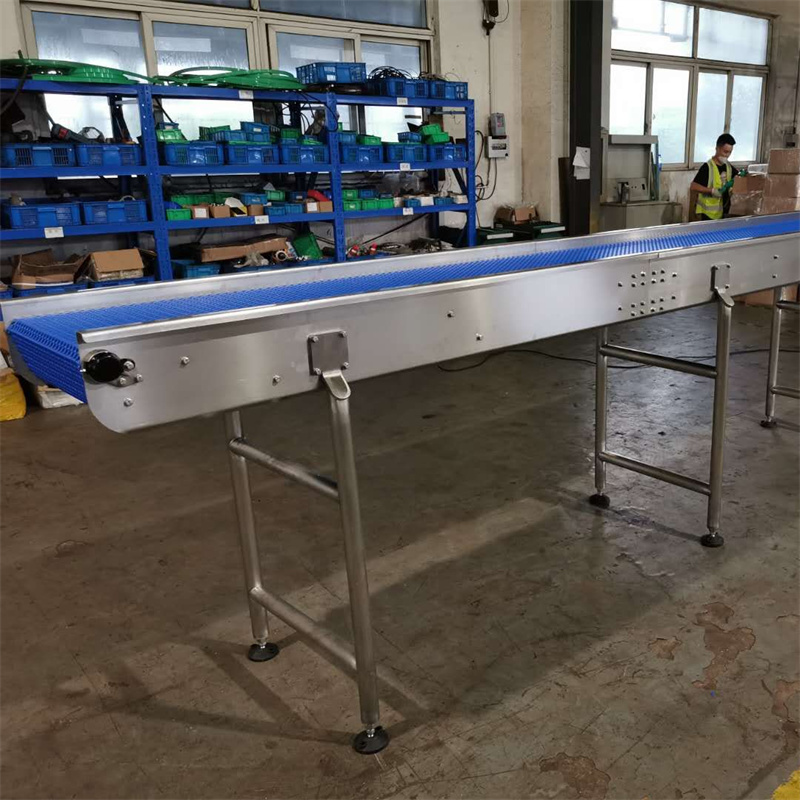
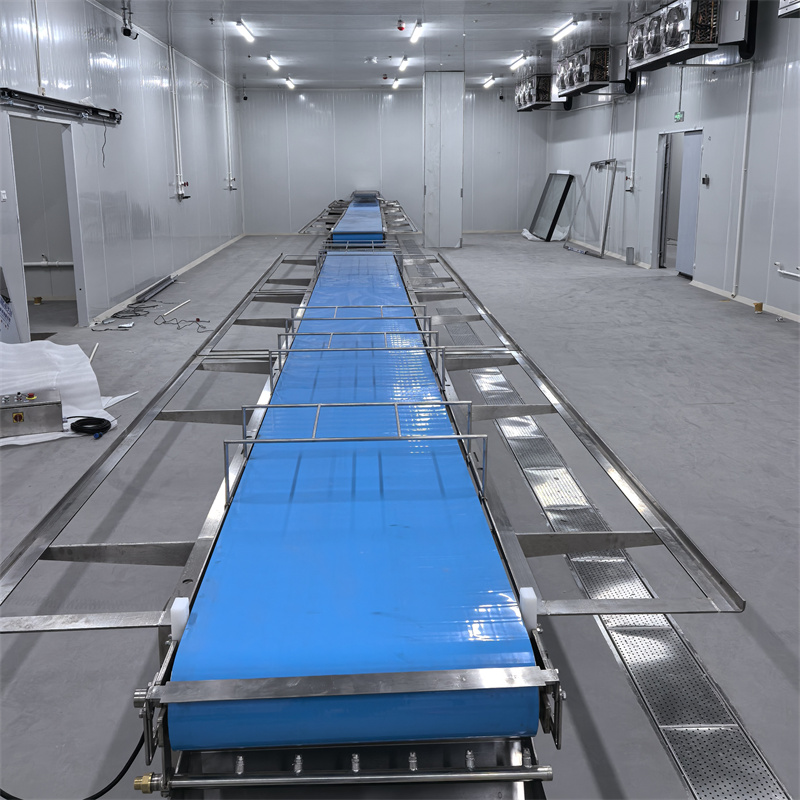
● — made entirely of food-grade stainless steel with polished, crevice-free, dust-shelf-free surfaces; fully compatible with high-pressure water and foam cleaning under FSMA thinking;
Flexible belt options
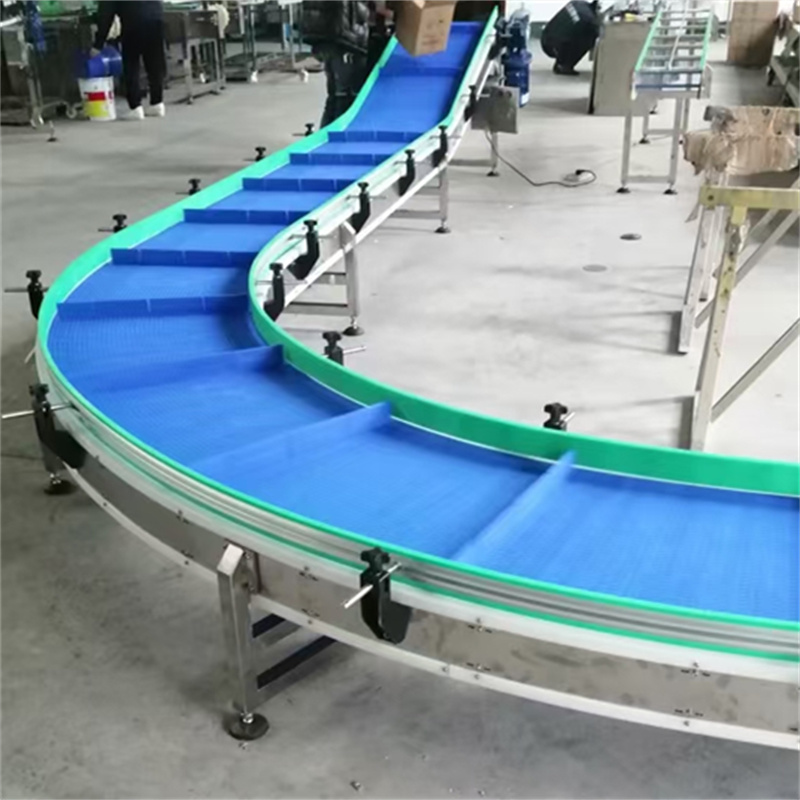
● — flat belts, modular belts or anti-slip patterned belts can be selected according to pack material and friction to balance smooth transport and surface protection;
Queuing guide system
● — adjustable side guide rails and dividing parts allow fast changeover to different queue widths and lane counts;
VFD drive with soft start/stop
● — gentle acceleration and deceleration prevent packs from sliding, squeezing or toppling through inertia;
Interlocked control
● — photoelectric interfaces as standard, ready to connect to a Globule line PLC (e.g. INOVANCE-based control) for linked speed regulation, gap-filling and full-load stop.
5. Hygiene and Safety Design
The whole machine follows the brand principle "Hygiene First · Safety First". The frame uses rounded transitions, belt-support decks can be hinged open for cleaning, and electrical wiring uses quick connectors so parts can be unplugged and flushed. All moving parts are guarded with safety interlocks, and maintenance space is reserved on the operator side. Every product-contact material meets food-contact requirements, eliminating foreign-body contamination risks and helping food plants pass hygiene audits and FSMA compliance checks with confidence.
6. System Coordination and Customisation
As a complete-line supplier, Globule delivers layout engineering together with the conveyor: machine spacing, conveying direction, turning radius and transfer heights are surveyed and customised on site by our engineers so the conveyor mates perfectly with the bucket elevator, vibrate feeder, multihead weigher, fast-back conveyor, stainless platform and secondary packaging machine. Both single-machine purchases and whole-line packages are available, and expansion interfaces are reserved — when production grows, additional sections can be added without rebuilding the line.
7. Service and Support
Globule offers end-to-end service from selection, site survey, installation and commissioning to operator training. Our engineering team has cross-industry implementation experience in food, daily chemical and pharmaceutical plants. Every delivery includes bilingual manuals, spare-parts lists and remote technical support so the secondary packaging line keeps running reliably for the long term.
Specifications (Typical Configuration)
● Standard configuration is customised per line layout; contact Globule for the exact belt width, length, speed and interlock scheme matched to your rhythm and pack size.