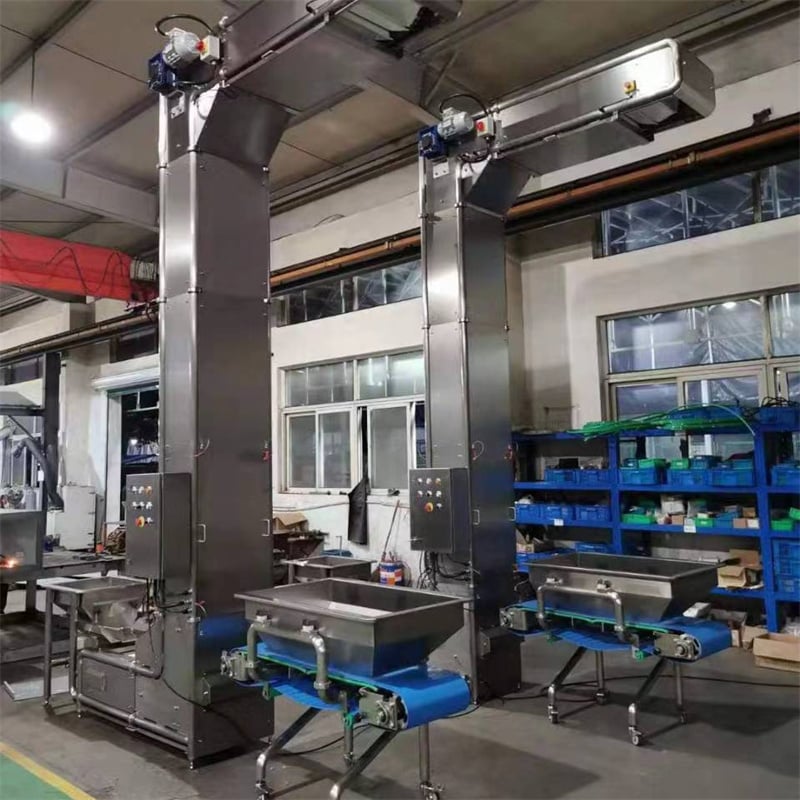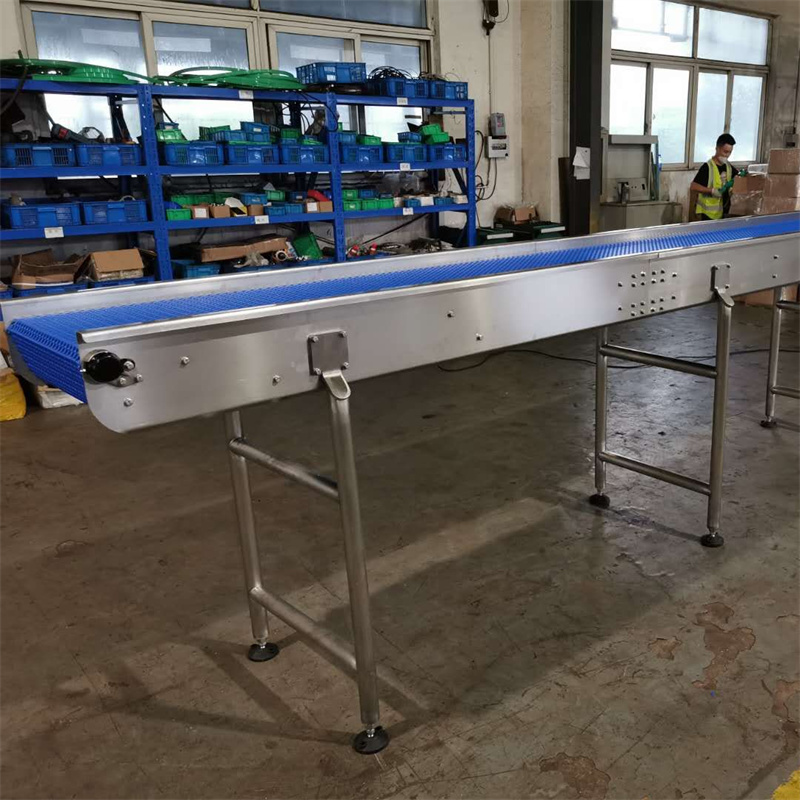
In traditional food production, the mixing of powdered, granular, or liquid raw materials relies heavily on manual labor or semi-automated equipment, resulting in problems such as large fluctuations in proportioning accuracy, risks of cross-contamination, difficulty in ensuring batch consistency, and limited production efficiency. Furthermore, the transfer of materials after mixing and the seamless connection between the packaging process can easily lead to material exposure and secondary contamination. Customers urgently need an integrated system that can achieve precise metering, uniform mixing, and direct connection to the packaging line to improve product quality, production speed, and compliance levels.
Globule Sanitary Conveyor Pty Ltd provides a fully automated, high-precision food mixing and packaging system that integrates ingredient preparation, uniform mixing, and direct filling to eliminate contamination risks and boost production efficiency by 40%.
· Zero-Residue Mixing Logic: Mirror-polished inner walls and customized ribbon agitators ensure 99.9% discharge rate, perfect for high-value food powders.
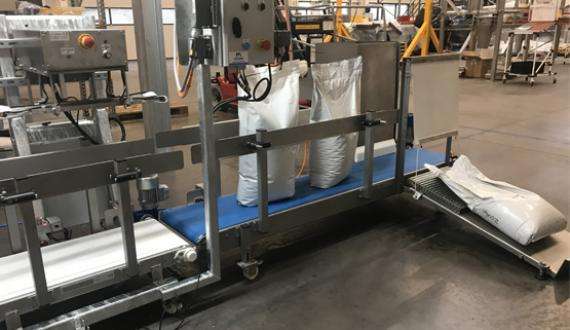
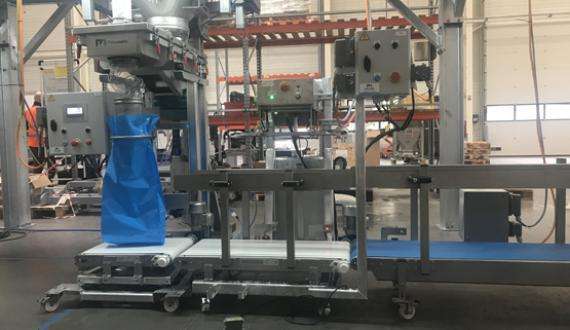
· One-Click Size Changeover: The integrated secondary packaging unit allows for switching between sachet counts and bag sizes in under 15 minutes via the PLC interface.
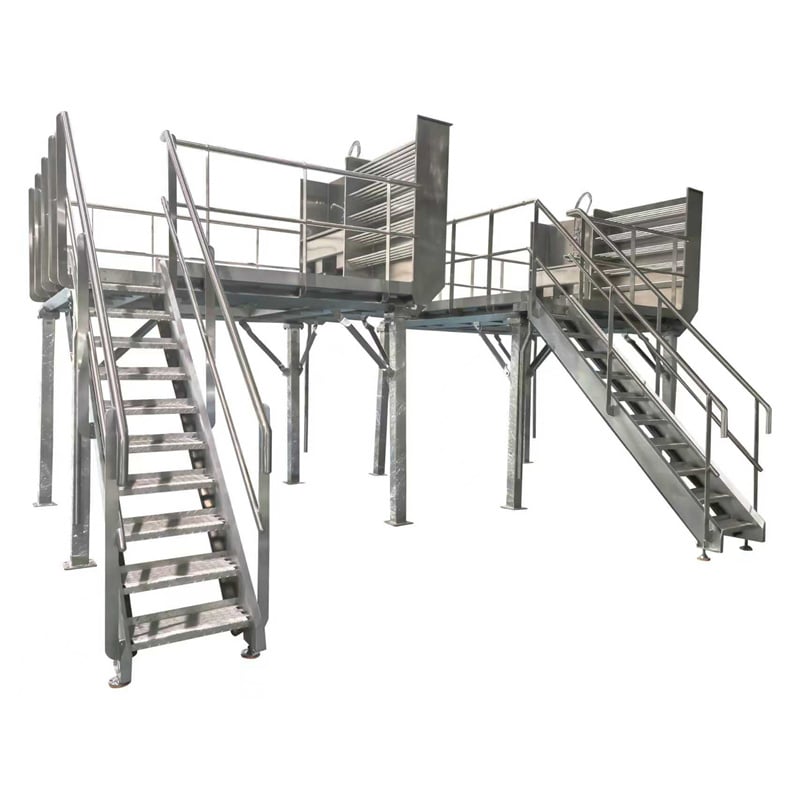
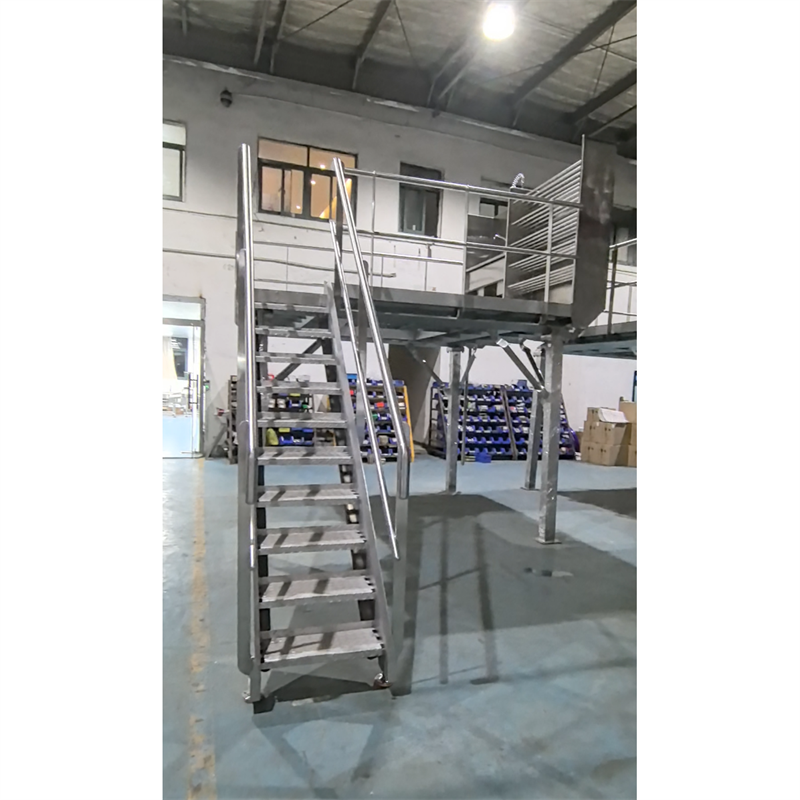
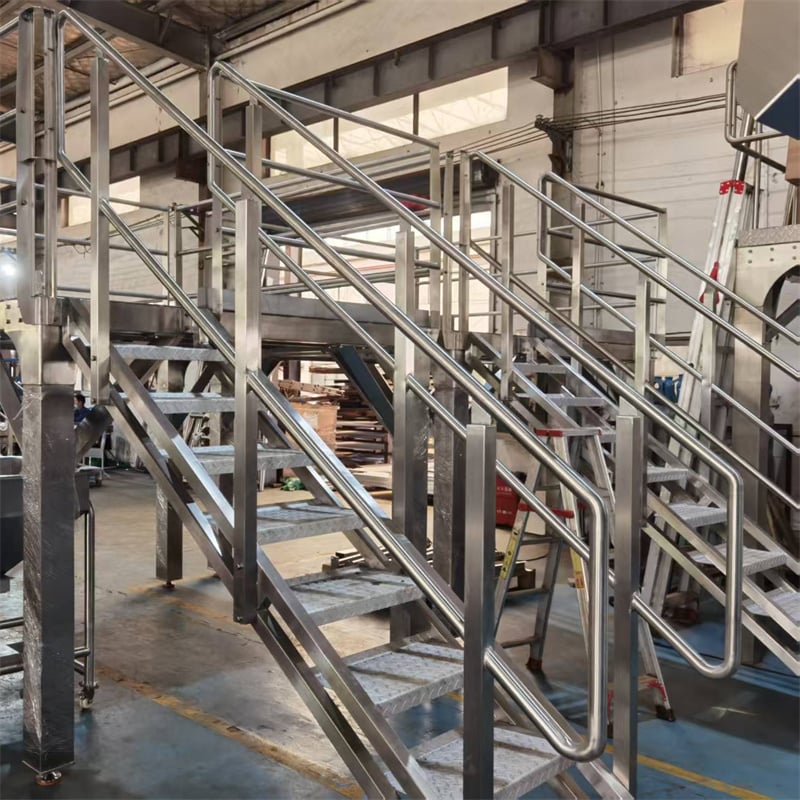
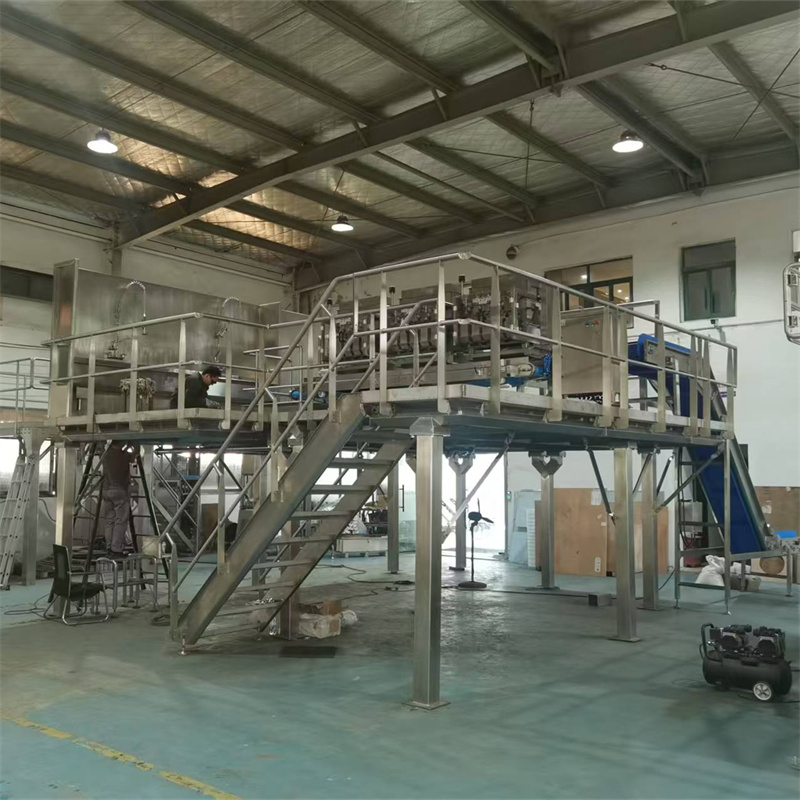
· Sanitary Support Structure: All platforms and mezzanine floors feature circular tubing and open-frame welding to prevent any bacterial accumulation in food plants.
 EN