EN

- Overview
- Recommended Products
Overview
Product Overview
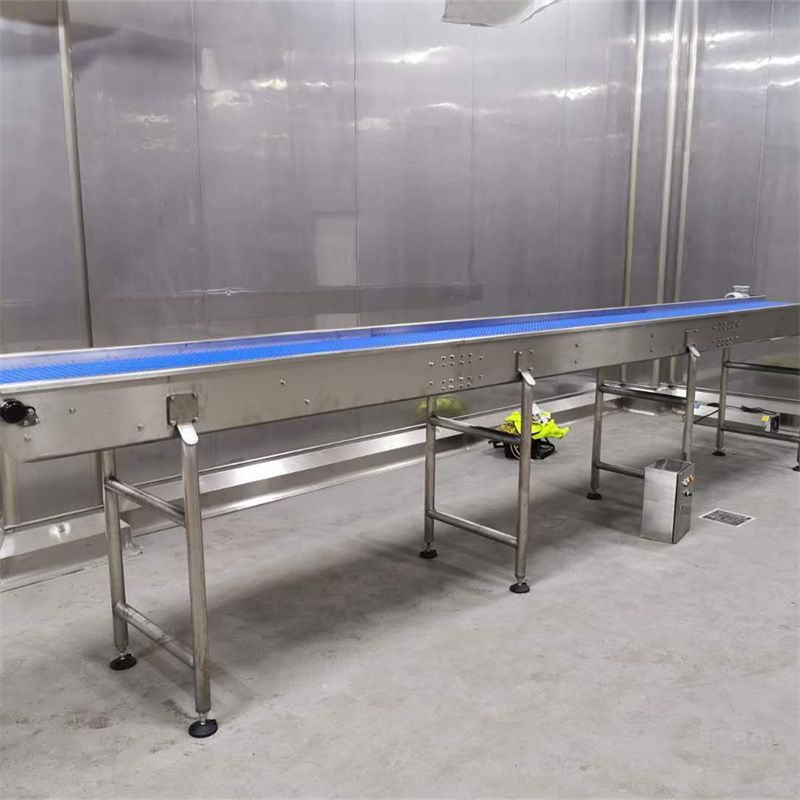
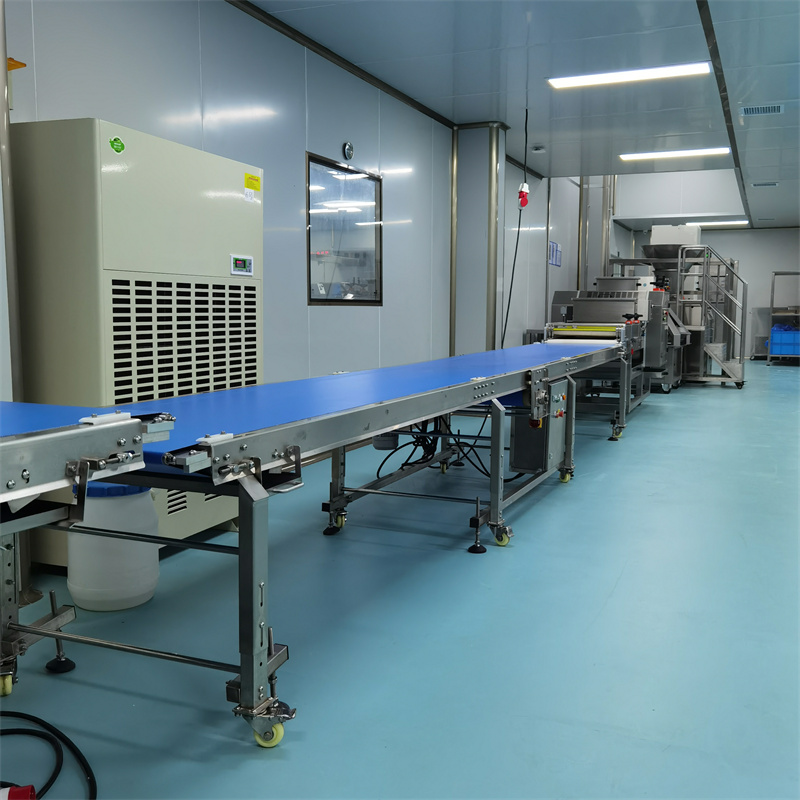
The Conveyor in the mixing packaging system serves as the "unified dispatcher" for multi-ingredient blended materials after they exit the linear scale. Unlike the conveyors in other packaging system categories — which primarily handle single-product logistics — the mixing packaging system places a higher-dimensional demand on the conveyor: not only must it accomplish the horizontal displacement of materials, but it must also maintain the blend uniformity of multi-ingredient mixtures throughout the conveying process, preventing ingredients of different densities and particle sizes from separating or stratifying under conveying vibration, ensuring that every finished package faithfully reproduces the precise blend ratio output by the linear scale.
Established in 2019, Globule's engineering team brings over 10 years of hands-on industry experience to every design. The mixing-system-dedicated Conveyor is purpose-optimized in belt material, operating speed, belt width, and side-guide design for multi-ingredient mixed conveying duty, following FSMA sanitary design guidelines to ensure that blend ratio integrity is maintained — without stratification or contamination — throughout the full conveying path from mix outlet to packaging machine inlet.
Core Design Advantages
1. Wide Belt Surface — Preventing Multi-Ingredient Stratification
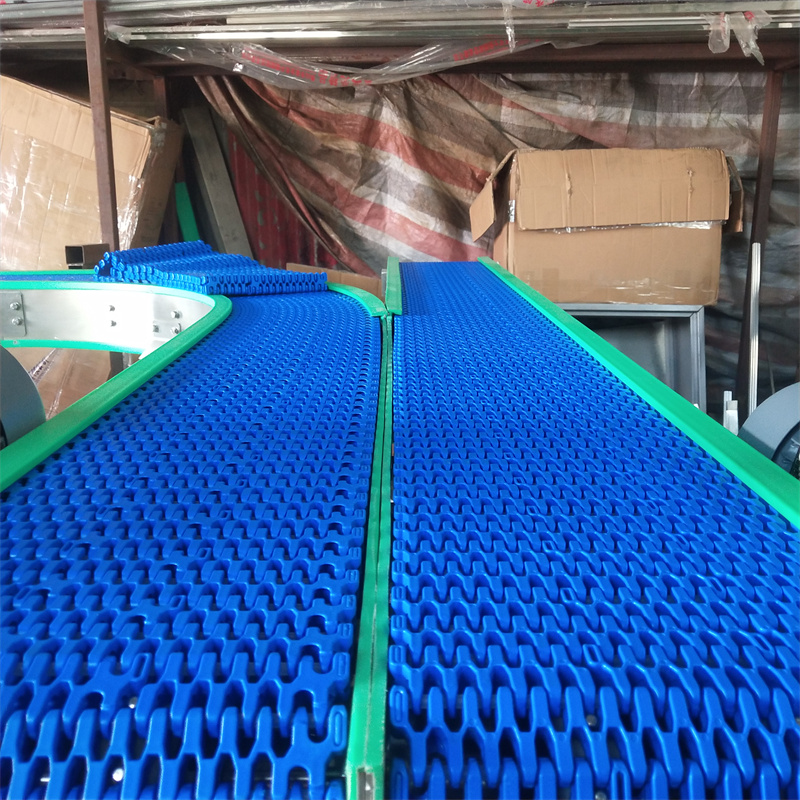
Mixing packaging products typically contain multiple ingredients with significantly different densities and particle sizes — for example, cashews and raisins, or nuts and oats. In narrow-belt high-speed conveying, dense particles (nuts) tend to migrate to the belt edges while lighter particles (oat flakes, dried fruit) concentrate in the center, causing cross-sectional blend imbalance and final product deviation from the target recipe. Globule's mixing system Conveyor uses a wide belt surface design where materials are conveyed in a naturally spread-out single layer across a larger belt area. This reduces stacking height per unit area and fundamentally lowers the driving force for vibration-induced stratification, ensuring finished package blend ratios closely match the linear scale output.
2. Smooth Low-Vibration Operation — Preserving Blend Uniformity
After the linear scale completes blend weighing, the mixed materials enter the conveyor already in a specific blended state. Any vibration shock or speed change during conveying can disrupt this state and cause remixing-induced stratification. Globule's Conveyor drive system is specifically tuned for smooth start-stop and minimal operating vibration, maintaining blend state stability from belt entry to belt exit throughout. The belt tensioning system is similarly optimized to eliminate periodic belt sag and flutter, providing a "disturbance-free" conveying path for mixed materials.
3. Easy-Clean Belt Design — Supporting Rapid Multi-Recipe Changeovers
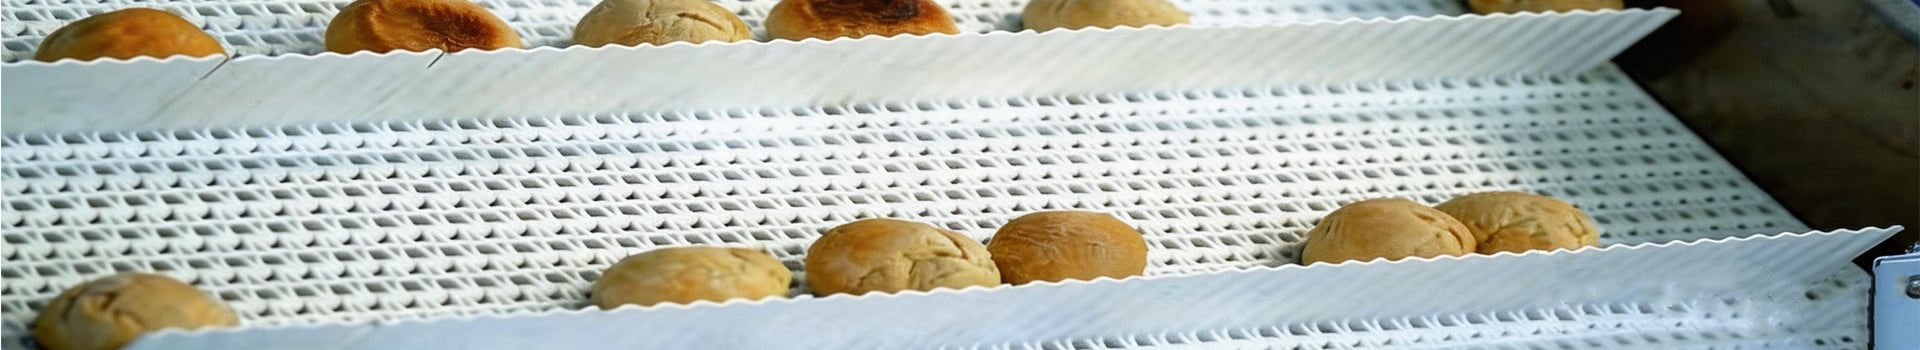
Mixing packaging products are typically highly varied, requiring a single line to complete multiple recipe changeovers within the same production day. At each changeover, thorough cleaning of the conveyor belt is the critical step for preventing residual ingredients from compromising the next batch's recipe accuracy and for avoiding allergen cross-contamination. Globule's Conveyor uses a food-grade belt material with a smooth, non-adhesive surface. Combined with quick-release side guides and a liftable lightweight slack-drive belt, operators can complete belt cleaning in minimal time, matching the high-frequency changeover pace of modern food factories.
4. Optional Side Guides — Preventing Material Loss and Protecting Blend Integrity
In mixed-material conveying, lighter or smaller-particle ingredients can spill from the belt edges, causing blend ratio loss. Globule's Conveyor can be fitted with flexible food-grade side guides that closely follow the belt surface curvature, forming a dead-zone-free lateral enclosure along the full conveying path. This delivers every batch of mixed material completely to the packaging machine inlet without losing any ingredient component. The side guides use food-grade elastic material that conforms tightly to the belt without excessive friction — effectively retaining materials while not impeding normal belt operation or cleaning.
5. Full Stainless Steel Frame — Meeting Mixing Workshop Hygiene Standards
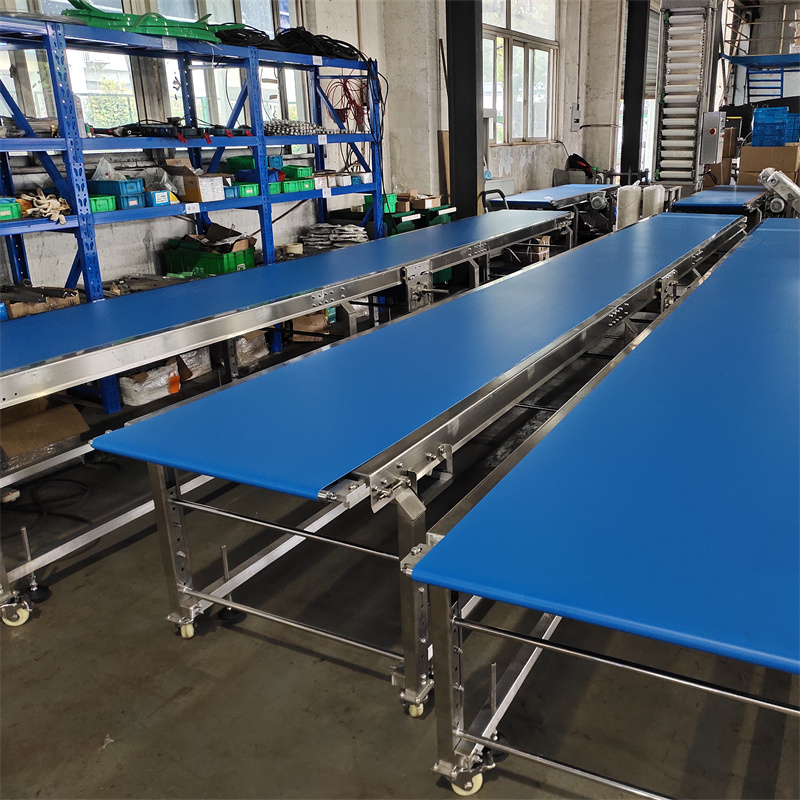
Mixing workshops simultaneously handle multiple food ingredients, with high hygiene classification requirements — especially when high-allergen-risk materials such as nuts or dairy ingredients are involved, where equipment surface cleanliness directly impacts product safety. Globule's Conveyor frame is manufactured entirely from food-grade stainless steel with smooth, seamless, dead-zone-free surfaces. It withstands high-pressure water rinse, steam cleaning, and food-grade disinfectant treatment, ensuring zero-residue compliance after every changeover cleaning — satisfying the equipment hygiene requirements of FSMA, HACCP, and other food safety regulations.
Technical Specifications
| Parameter | Specification |
| Frame Material | Food-grade stainless steel |
| Belt Material | Food-grade polyurethane or PVC, smooth surface |
| Belt Width | Customized to blend product type and production capacity |
| Drive Method | SITI / SEW gear motor / motorized drum (optional) |
| Side Guides | Optional food-grade flexible side guides |
| Cleaning System | Optional inline spray cleaning system |
| Installation | Adjustable-height stainless steel legs, on-site height setting |
| Compliance | Designed following FSMA sanitary guidelines |
| Custom Options | Belt width, conveyor length, side guide height, drive position to specification |
Role in the Mixing Packaging System
Within the complete mixing packaging system workflow, the Conveyor bridges the linear scale's blend output and the packaging machine:
Linear Scale
1. — Precisely weighs multiple ingredients to the set blend ratio, completing the mix
Conveyor (this unit)
2. — Receives mixed materials from the linear scale, conveys them with stable uniform distribution while maintaining blend ratio integrity, delivers to packaging machine inlet
Inclined Conveyor
3. — Elevates the mixed materials from the conveyor to the height required by the packaging machine (where a height difference exists in the line)
Packaging Machine
4. — Receives mixed materials and completes filling and sealing of multi-format finished bags
Protective Frame
5. — Provides allergen cross-contamination isolation protection at key conveying nodes
The Conveyor occupies the critical connecting position between the linear scale and the packaging machine in this workflow. Its conveying stability and blend ratio preservation capability directly affect finished package quality compliance rates.
Applicable Products
Globule's mixing system Conveyor is purpose-optimized for the following mixed-product types:
Mixed nuts
● — Multi-variety nut blends: cashews, almonds, walnuts, pistachios
Nut and dried-fruit blends
● — Nuts combined with raisins, cranberries, goji berries, and similar
Grain blends
● — Oats, quinoa, flaxseed, and nut multi-ingredient mixtures
Multi-flavor snack blends
● — Mixed snacks of different shapes, densities, and flavors
Functional food formulations
● — Protein bar ingredient blends, meal-replacement mix pre-conveying
Why Choose Globule's Mixing System Conveyor?
Purpose-designed for blend ratio preservation — not generic logistics conveying. Globule's mixing system Conveyor is specifically optimized in belt width, low-vibration operation, and side guide configuration for maintaining multi-ingredient blend uniformity — genuinely solving the "conveying stratification" problem that is common in mixing packaging and that generic conveyors are typically unable to address.
Original system-matched, interface co-designed. As matched equipment for Globule's mixing packaging system, the Conveyor's belt surface height, inlet width, and discharge dimensions are co-designed and validated with the linear scale outlet and packaging machine inlet — direct installation with no secondary modification required.
Full-cycle delivery support. Globule provides complete delivery support from factory acceptance testing, on-site system integration, and commissioning through to operator training, ensuring the Conveyor achieves its designed operating performance within the complete mixing packaging system.
Get a Custom Quote
To learn more about mixing system Conveyor configuration options or a complete line quotation, please contact Globule's engineering team:
Email:
●
Tel / WhatsApp:
● +86 13818737877
Address:
● No.28 Huiye Road, Songjiang District, Shanghai, China
Hygiene First · Safety First — Globule Sanitary Conveyor Pty Ltd