EN

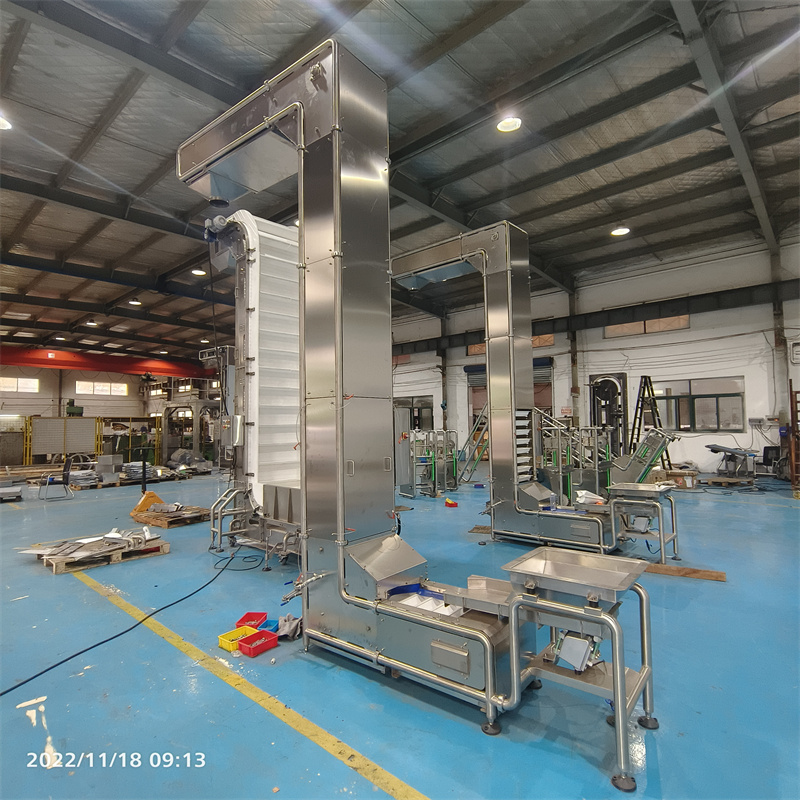
- Overview
- Recommended Products
Overview
1. Product Overview
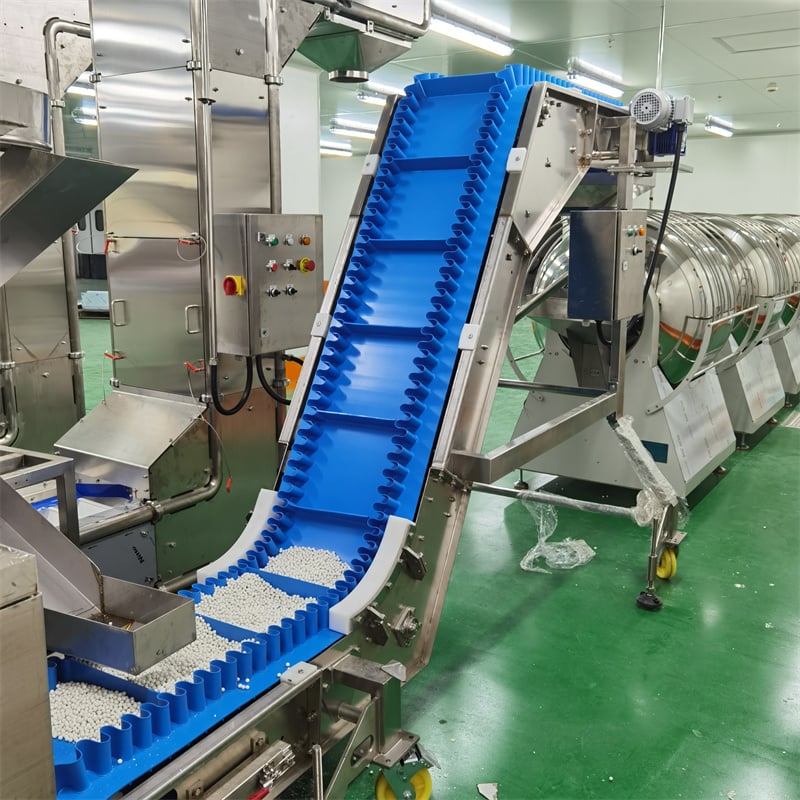
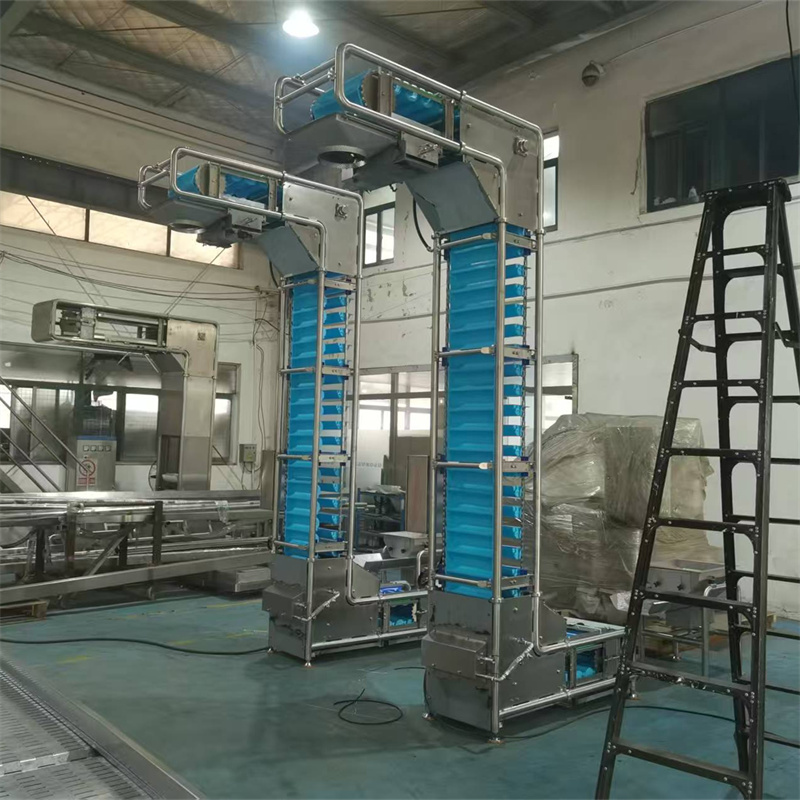
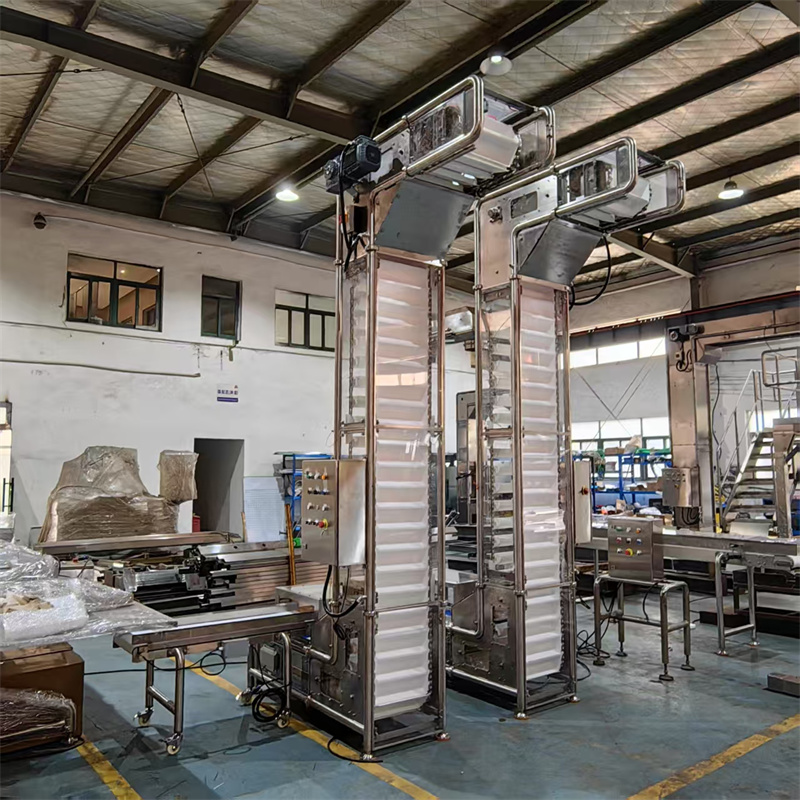
This bucket elevator lifts already-formed, already-sealed finished small packs in the vertical direction from a low-level conveyor line to a high level — a "secondary lifting" step. It is called "secondary" because the packs were already manufactured and wrapped on the primary production line; this machine handles no bulk material at all. Its only job is to carry these delicate finished packs smoothly upward — for example, into the secondary packaging machine mounted on the stainless platform, or across floors and equipment height differences, so the secondary packaging line can be laid out efficiently in three-dimensional space.
With an engineering team of more than ten years of experience in sanitary conveying equipment, Globule designs in line with FSMA sanitary design guidelines. For the secondary packaging scenario, this elevator is optimised on four parameters — lifting height, bucket geometry, running speed and transfer pacing. Its goal is protecting package integrity, not maximising throughput.
2. Essential Difference from Bulk Bucket Elevators
Traditional bucket elevators serve the vertical conveying of powders, granules, grain and other bulk materials: deep buckets, high speeds and bottom digging, chasing tonne-level capacity; the material is "scooped in and dumped out". This machine carries already-formed finished packs, and its design philosophy is entirely different:
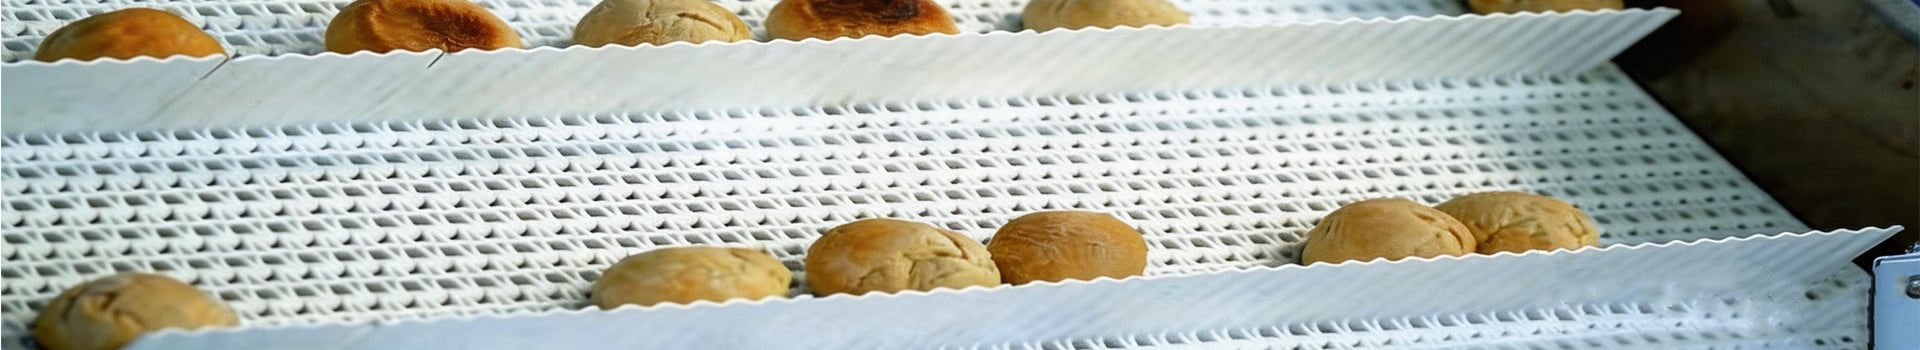
Cradle-type shallow/curved buckets
● — the bucket profile matches the shape and size of the pack, so each pack "sits" stably without tumbling or squeezing against its neighbours, and corners and seals are never scratched;
Speed tuned to the packaging material
● — running speed is buffered and throttled so start/stop inertia never tears film or loosens seals;
No bottom digging
● — finished packs are loaded in an orderly manner by the upstream conveyor at the loading station; not a single grain of bulk product enters the machine, eliminating the crushing, dust and jamming problems typical of bulk elevators;
Smooth transition sections
● — both the inlet and discharge are fitted with buffered guides and packs keep their spacing, preventing stacking and deformation at turning points.
In a bulk elevator a little bump is nothing; on a finished pack the same bump means a broken bag, leaking product and rework. That is exactly the problem this machine exists to solve.
3. Typical Applications in the Secondary Packaging Line
Low-to-high cross-level conveying
1. — finished packs are lifted from the floor conveyor line up to the infeed of the bundling machine on the stainless platform, saving floor space and straightening the personnel flow;
Process height bridging
2. — where an upstream machine and the secondary packaging equipment sit at different heights, the elevator replaces a long inclined climbing conveyor, shortening the travel and reducing surface friction;
Multi-storey line linking
3. — packs made on the ground floor can be lifted to the second floor for secondary packaging, enabling compact "pack upstairs, store downstairs" layouts.
In every application the elevator is interlocked with neighbouring machines via photoelectric detection and PLC signals: it waits when the supply is short and slows when downstream is full, keeping the whole line's rhythm stable without stacking or starving.
4. Construction Highlights
Food-grade stainless housing
● — enclosed body with polished, crevice-free surfaces, flush-cleanable and in line with FSMA sanitary design;
Inspection windows
● — viewing ports let operators check pack condition and bucket travel at any time; a jam can be cleared within seconds;
Anti-slip buckets with cushioning strips
● — internal anti-slip and cushioning details minimise displacement and vibration during the rise;
Reliable tensioning and anti-tracking
● — simple, dependable chain/belt tensioning with anti-tracking devices reduce unplanned downtime;
Low-noise running
● — dynamically balanced drive components keep operation quiet and non-disruptive to the production environment.
5. Hygiene, Safety and Maintenance
All product-contact parts — buckets, guides and transfer plates — use food-contact-grade materials. Head and boot sections are guarded with safety interlocks: opening a service door stops the machine to protect personnel. Routine cleaning is simply a matter of opening the inspection doors and flushing the buckets and housing; modular construction makes wear-part replacement quick and maintenance cost low.
6. System Matching and Customisation
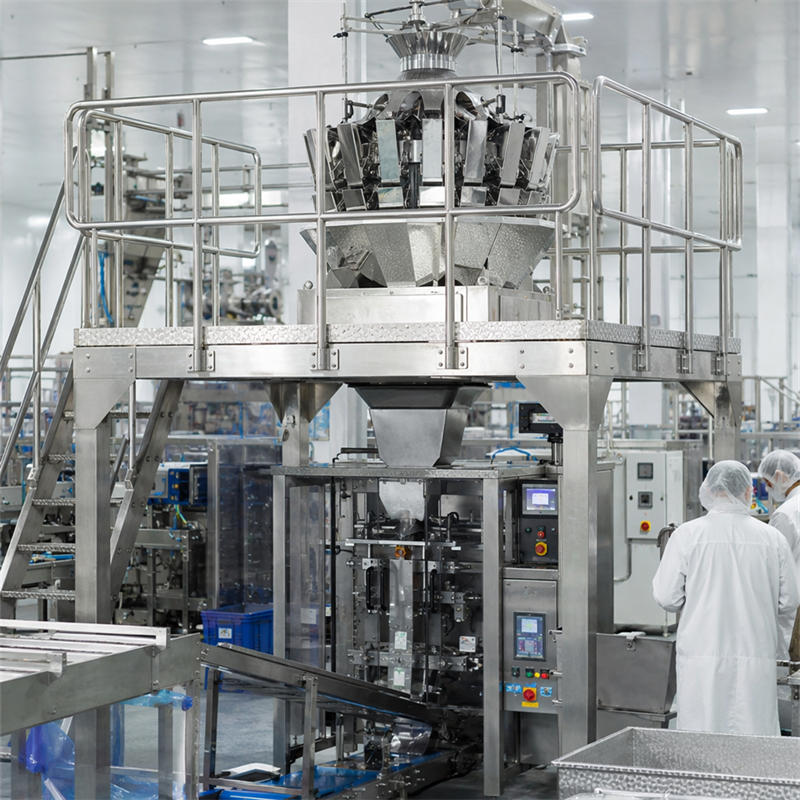
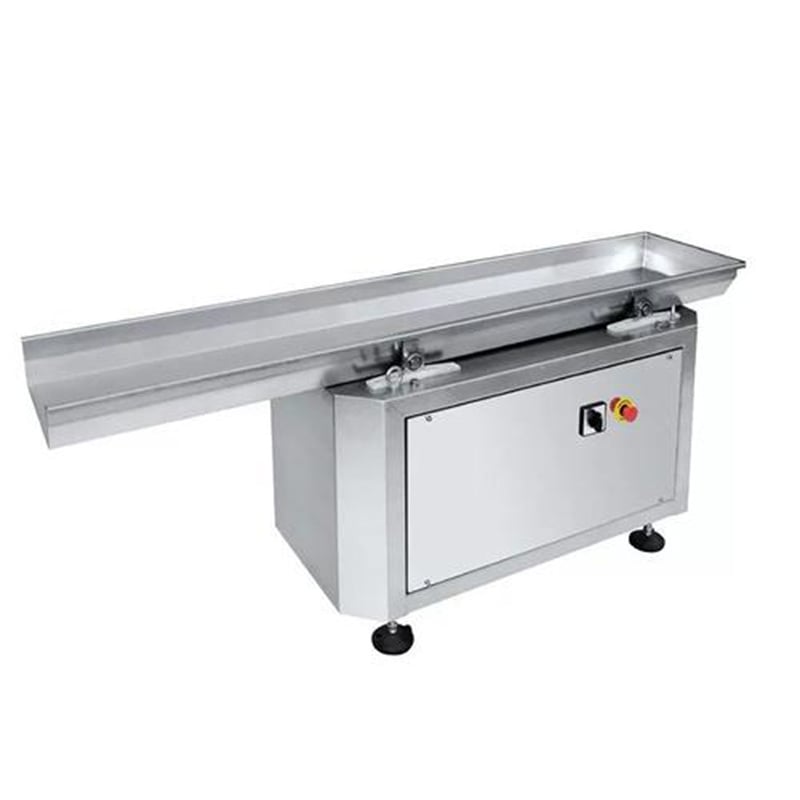
Globule provides site-surveyed customisation for every elevator: bucket pitch, bucket width and lifting speed are determined from the pack size, unit weight, lifting height and downstream infeed height. The elevator can be supplied and commissioned together with conveyors, vibrate feeder, multihead weigher, stainless platform and secondary packaging machine as one integrated package. Single-machine retrofits and greenfield lines are both welcome — send us pack samples and a line layout, and our engineers will issue a technical proposal.
7. Service Commitment
Since 2019 Globule has stood by "Hygiene First · Safety First". We provide full-service support — selection consulting, design, installation, commissioning, operator training and remote assistance — so every elevator is a stable, worry-free link in your secondary packaging line.
Specifications (Typical Configuration)
● Lifting height, bucket pitch and speed are customised per pack dimensions and line layout; contact Globule for a project-specific data sheet.